
Inside the works — machining to dispatch
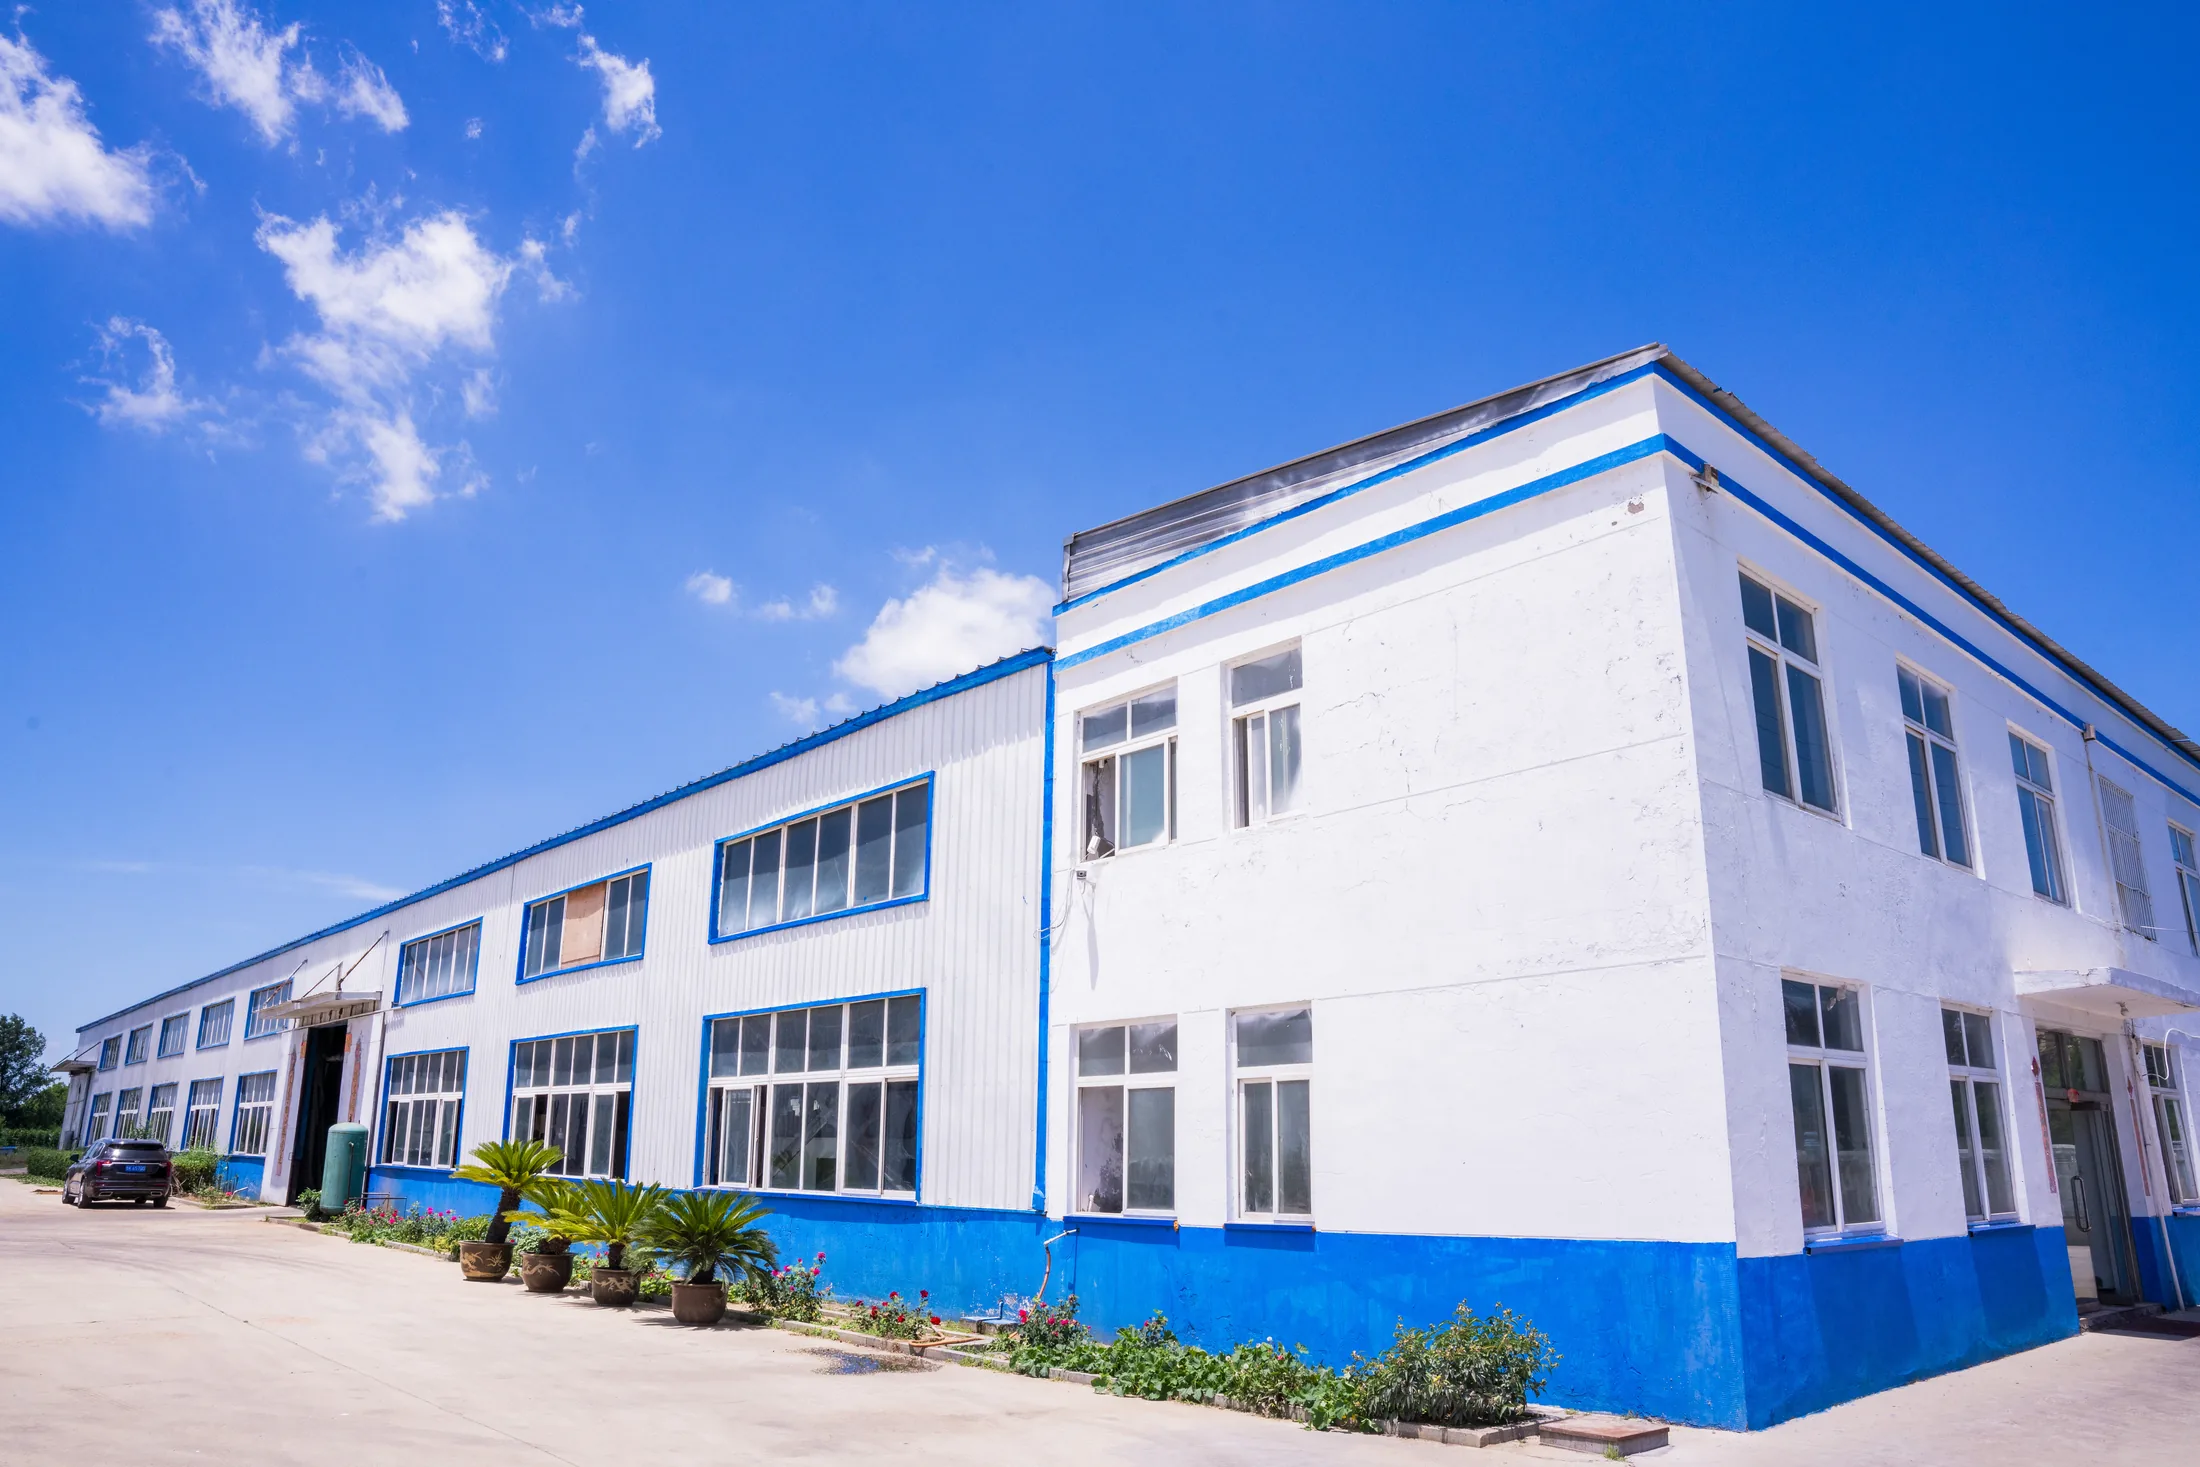
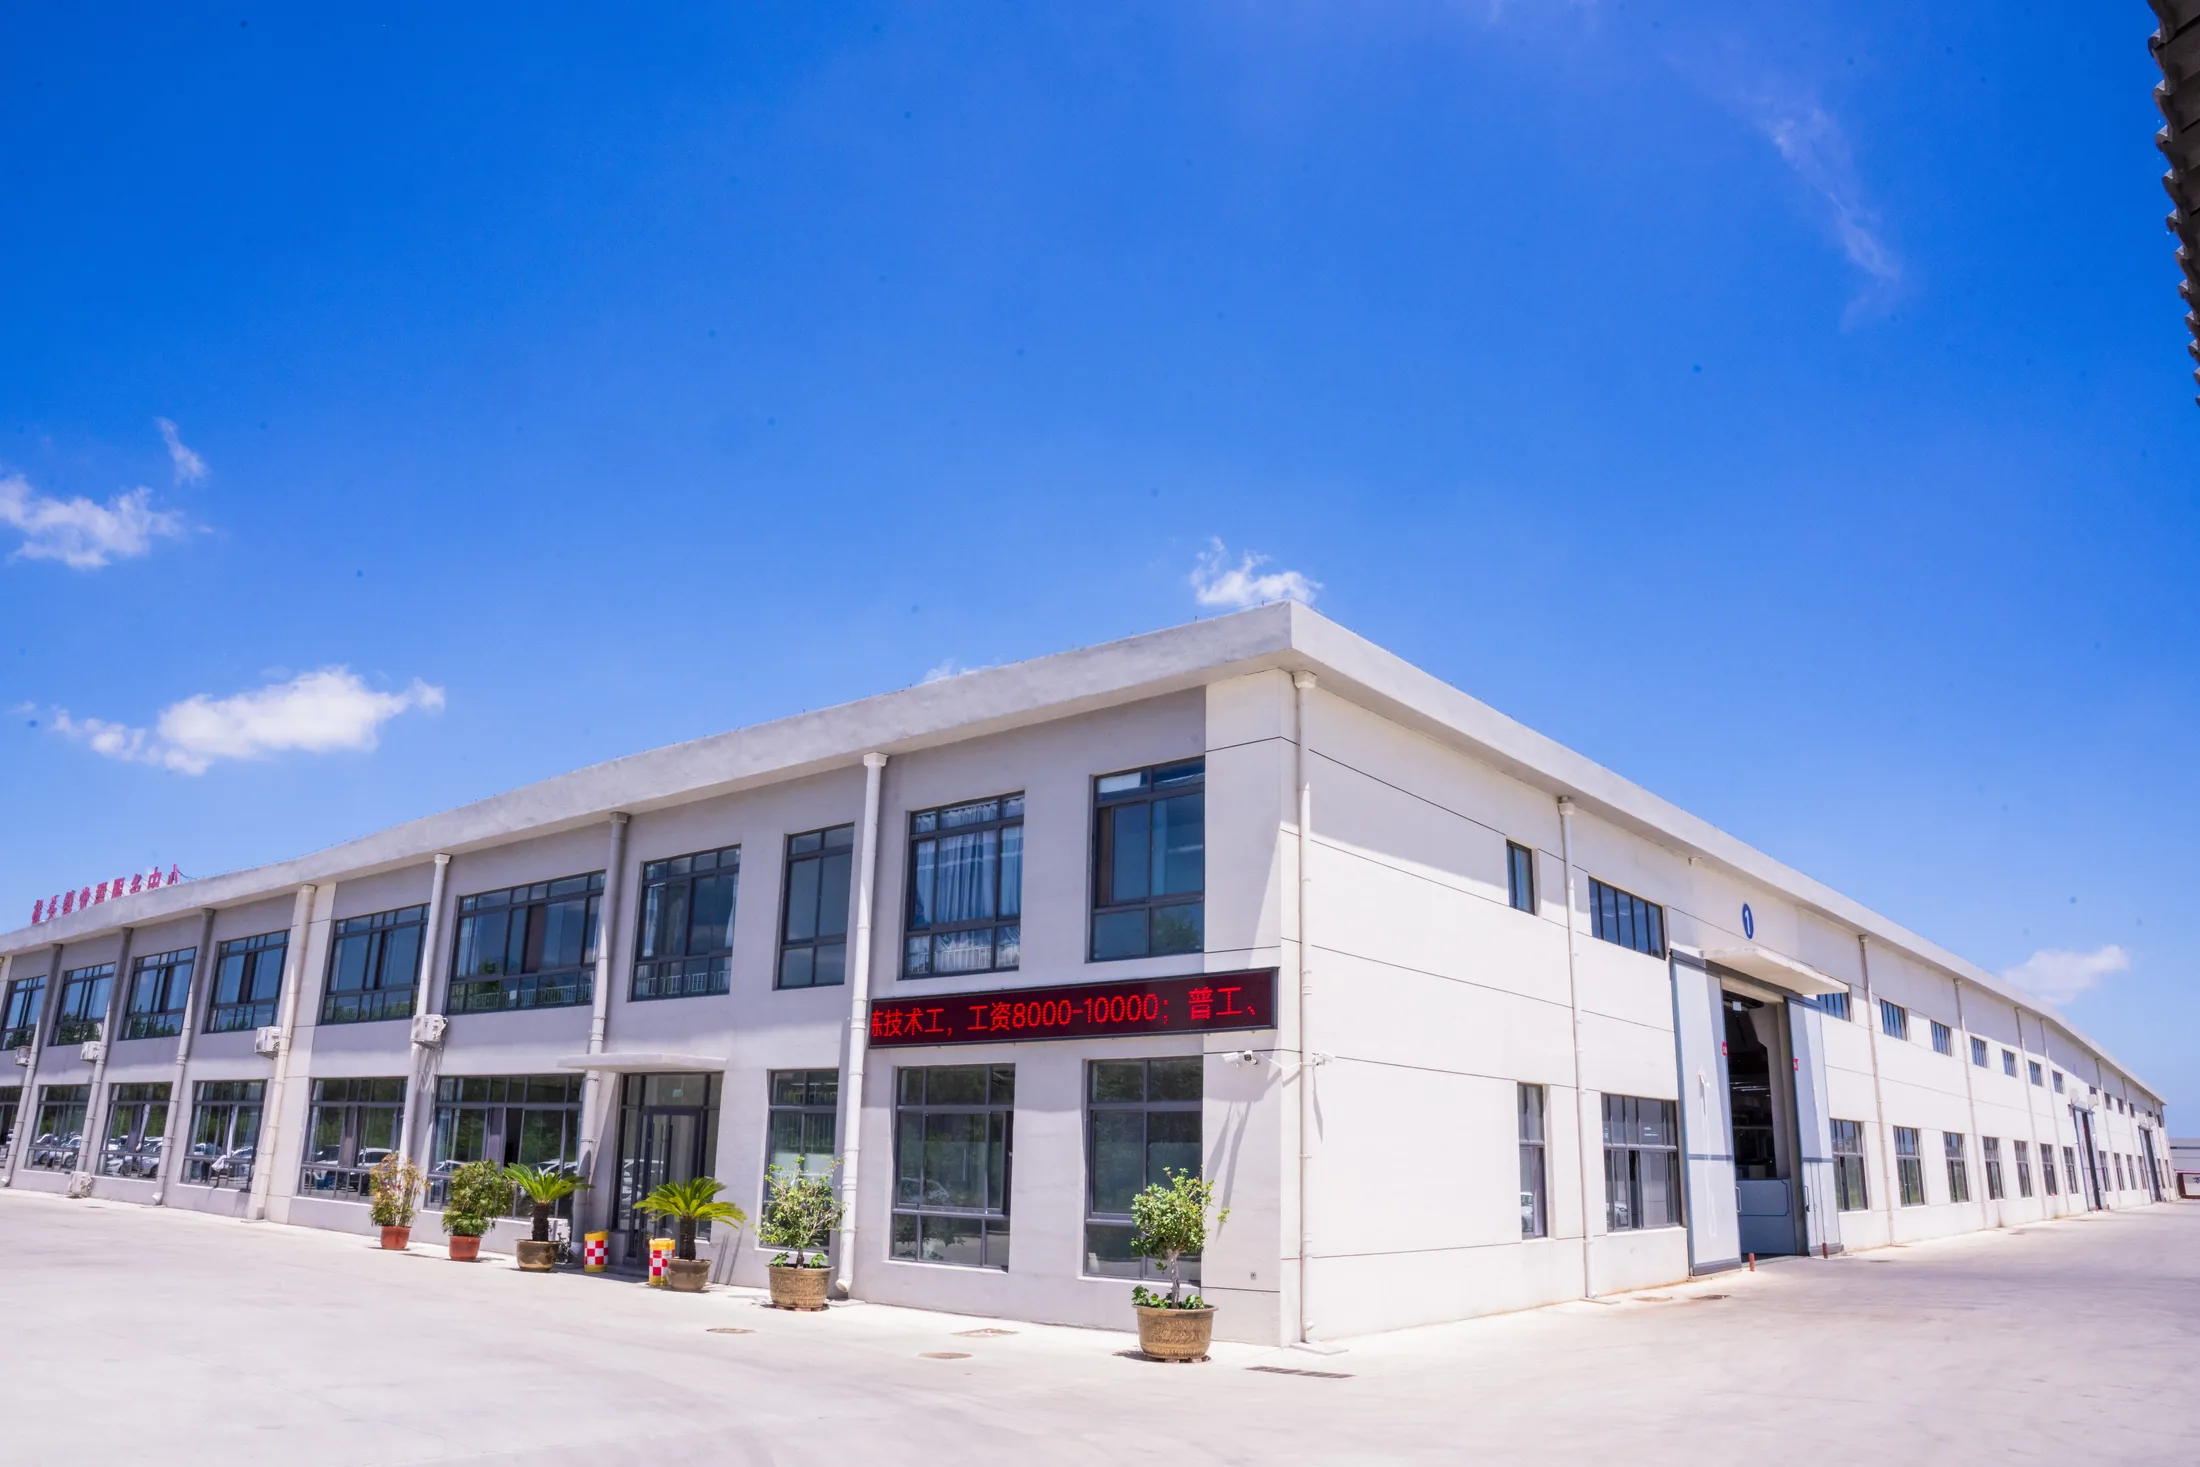
Thirty-seven pictures, no stock photos. Everything on this page is on our single site in Weihai — follow one actuator from bar stock to dispatch, with the machine behind every step. Visitors and third-party inspections are welcome.
The machine park — built around the spline
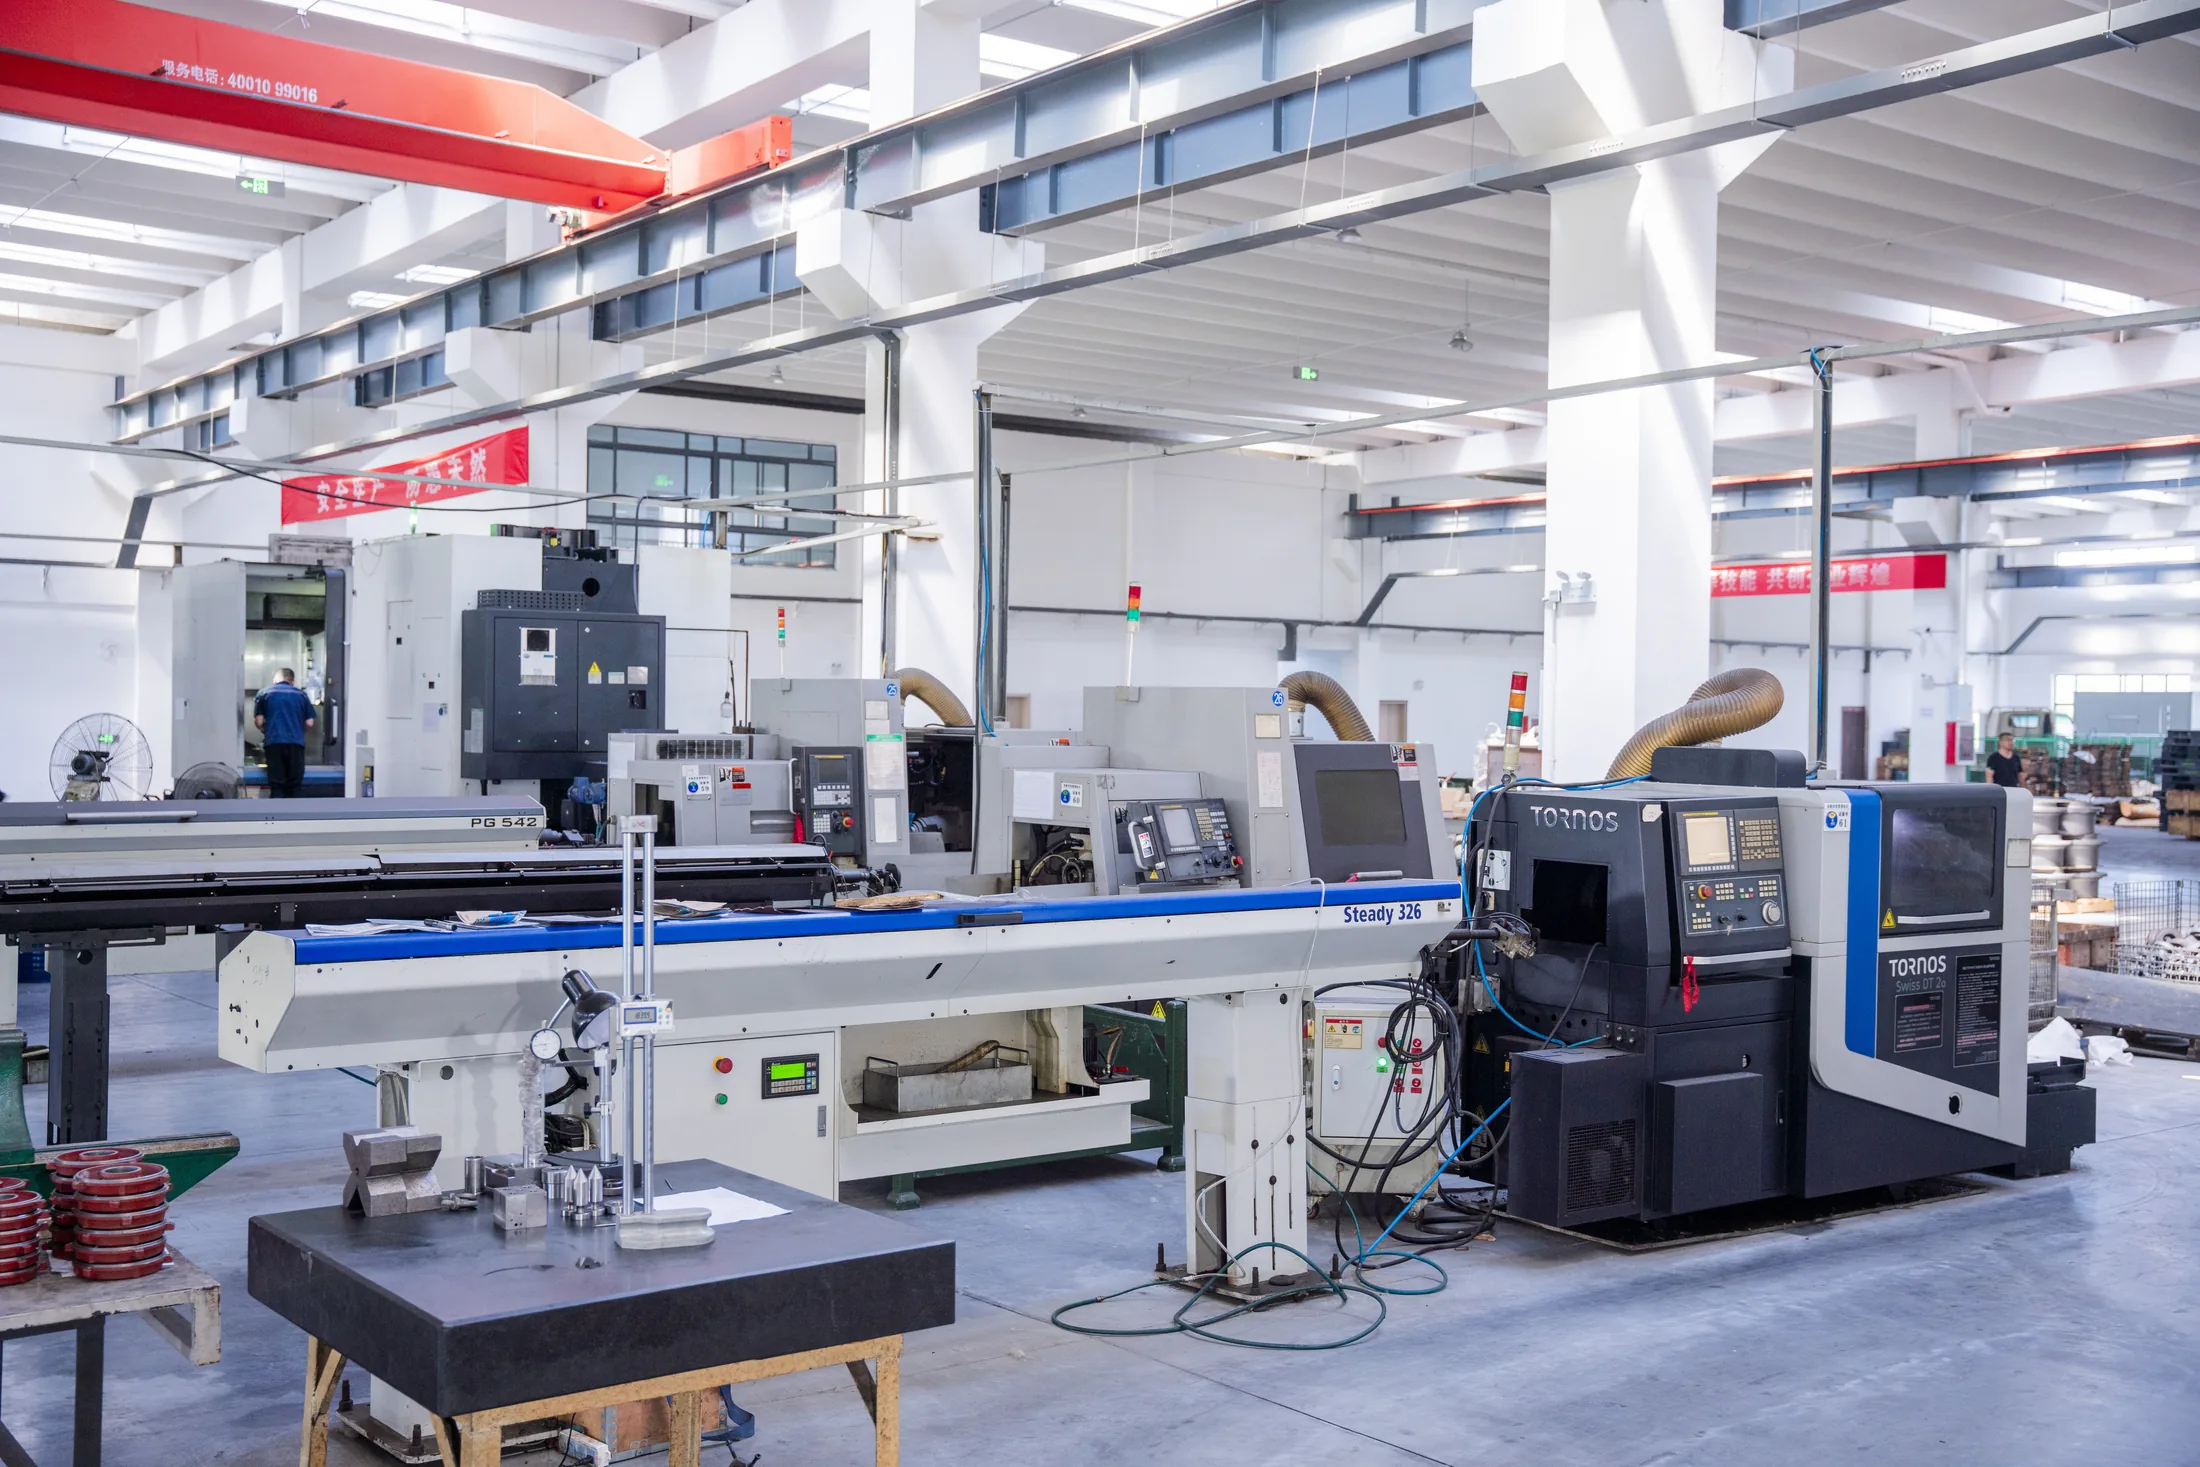
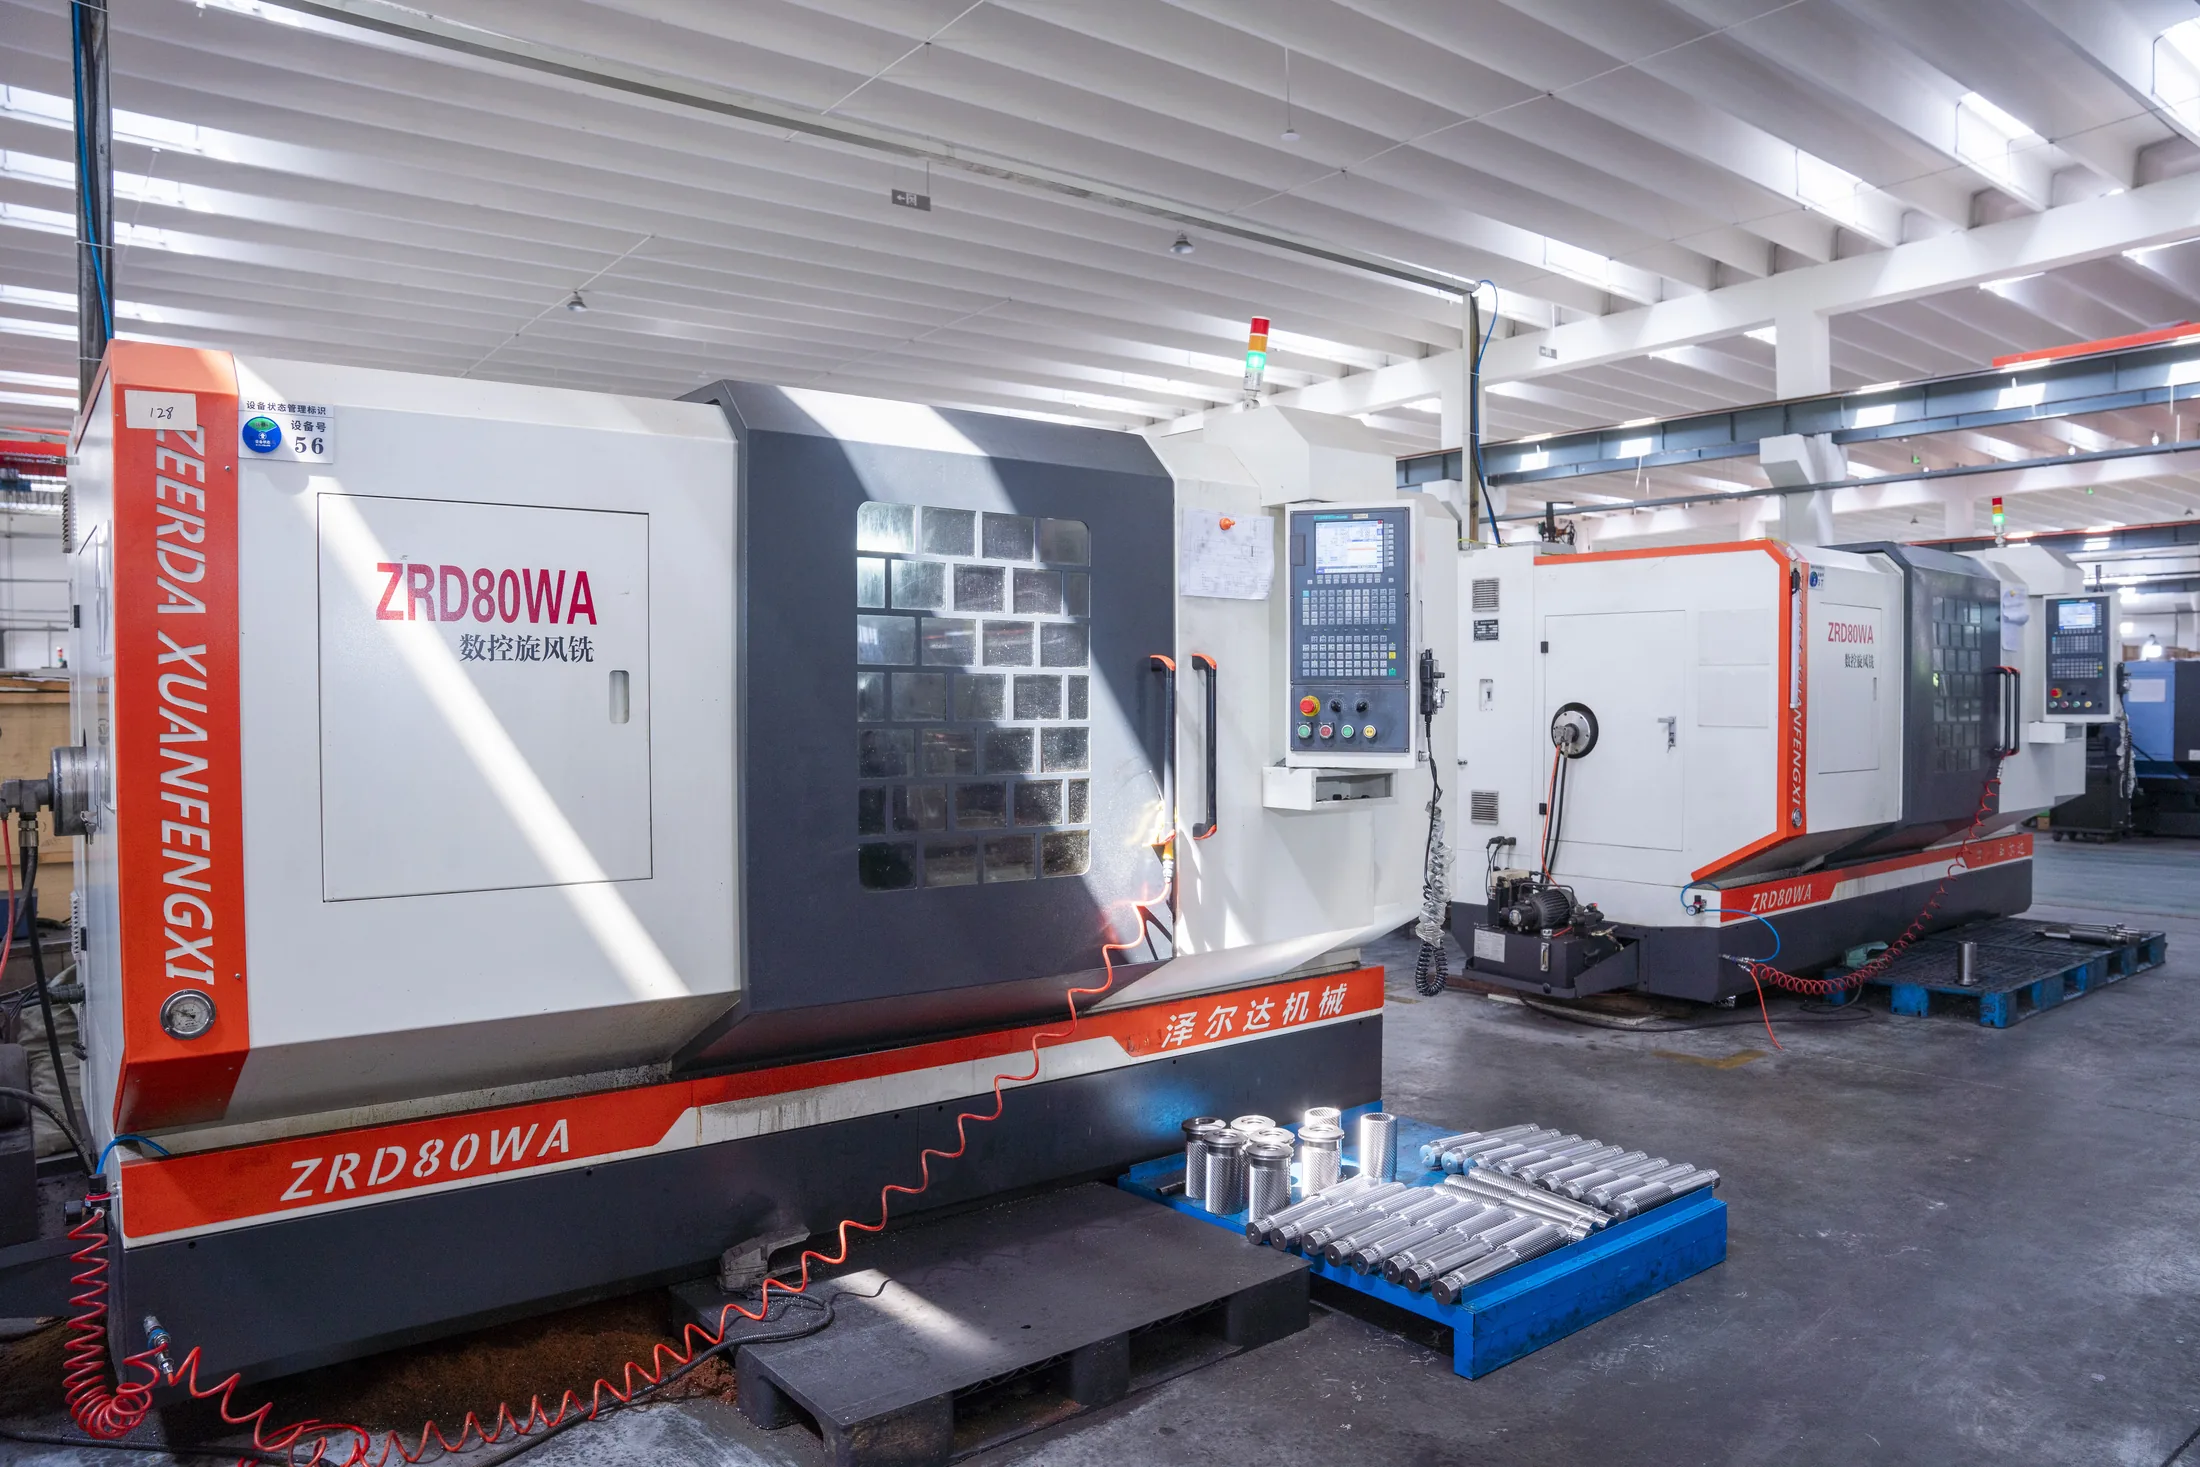
The performance of a helical rotary actuator depends on its spline set, so our machine line-up is arranged around it: whirling-milling and gear cutting for the splines, vertical lathes for the big flanges, Swiss lathes for the small shafts, machining centres for the housings.
Buildings & yard
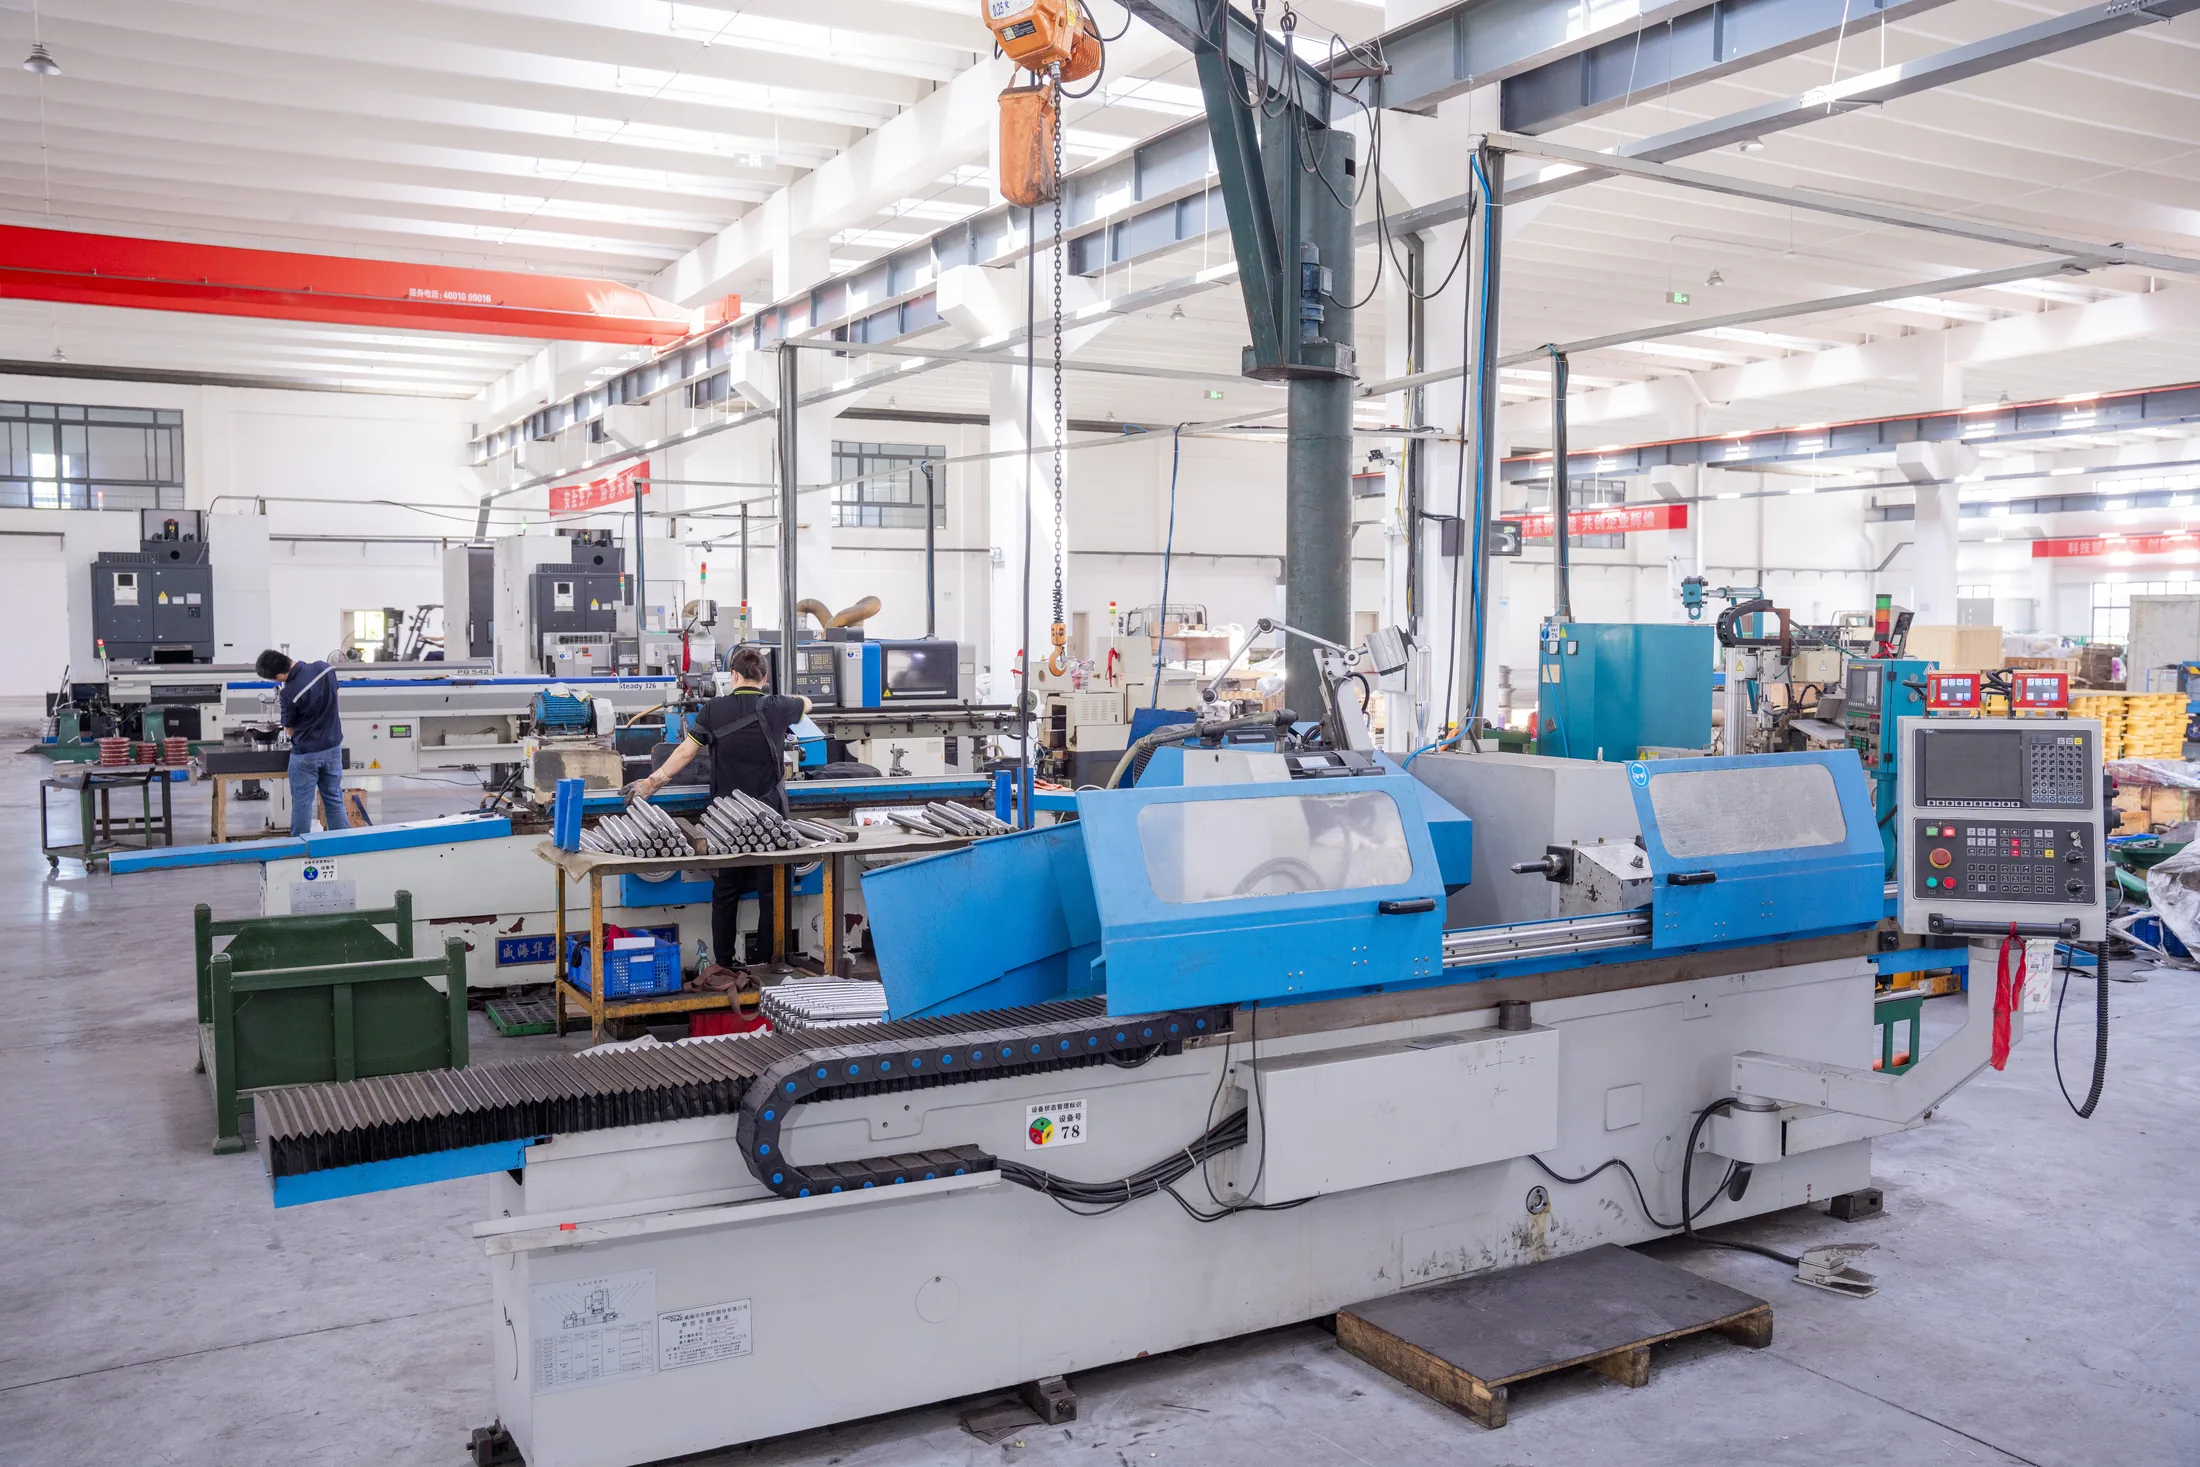
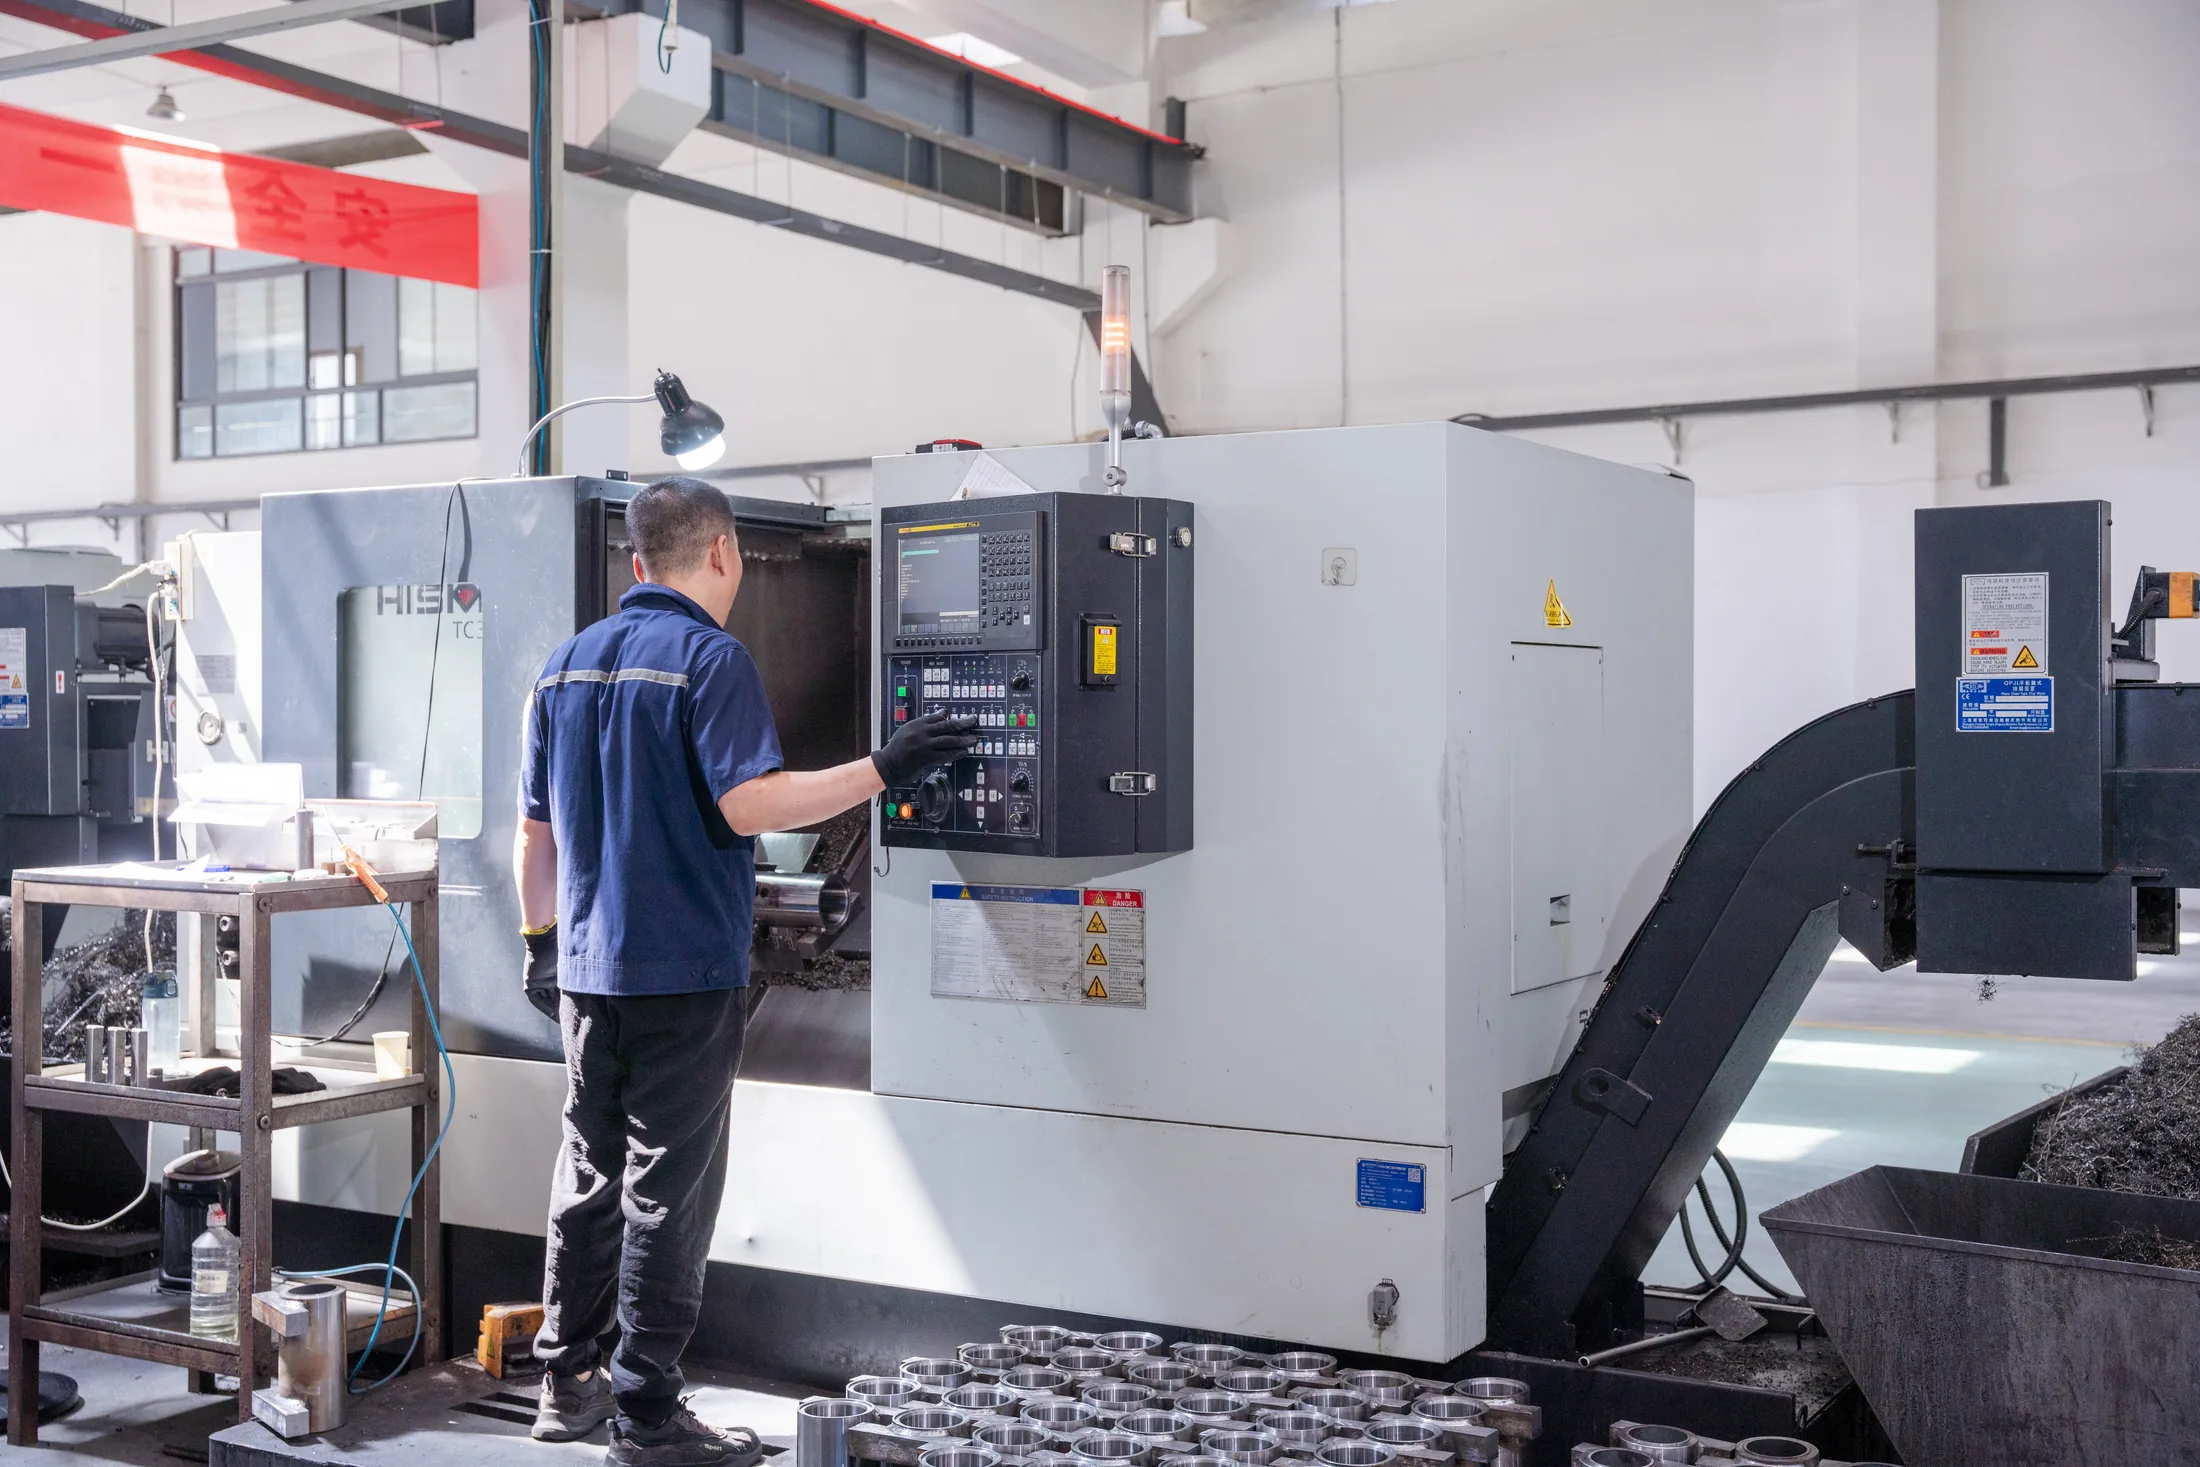
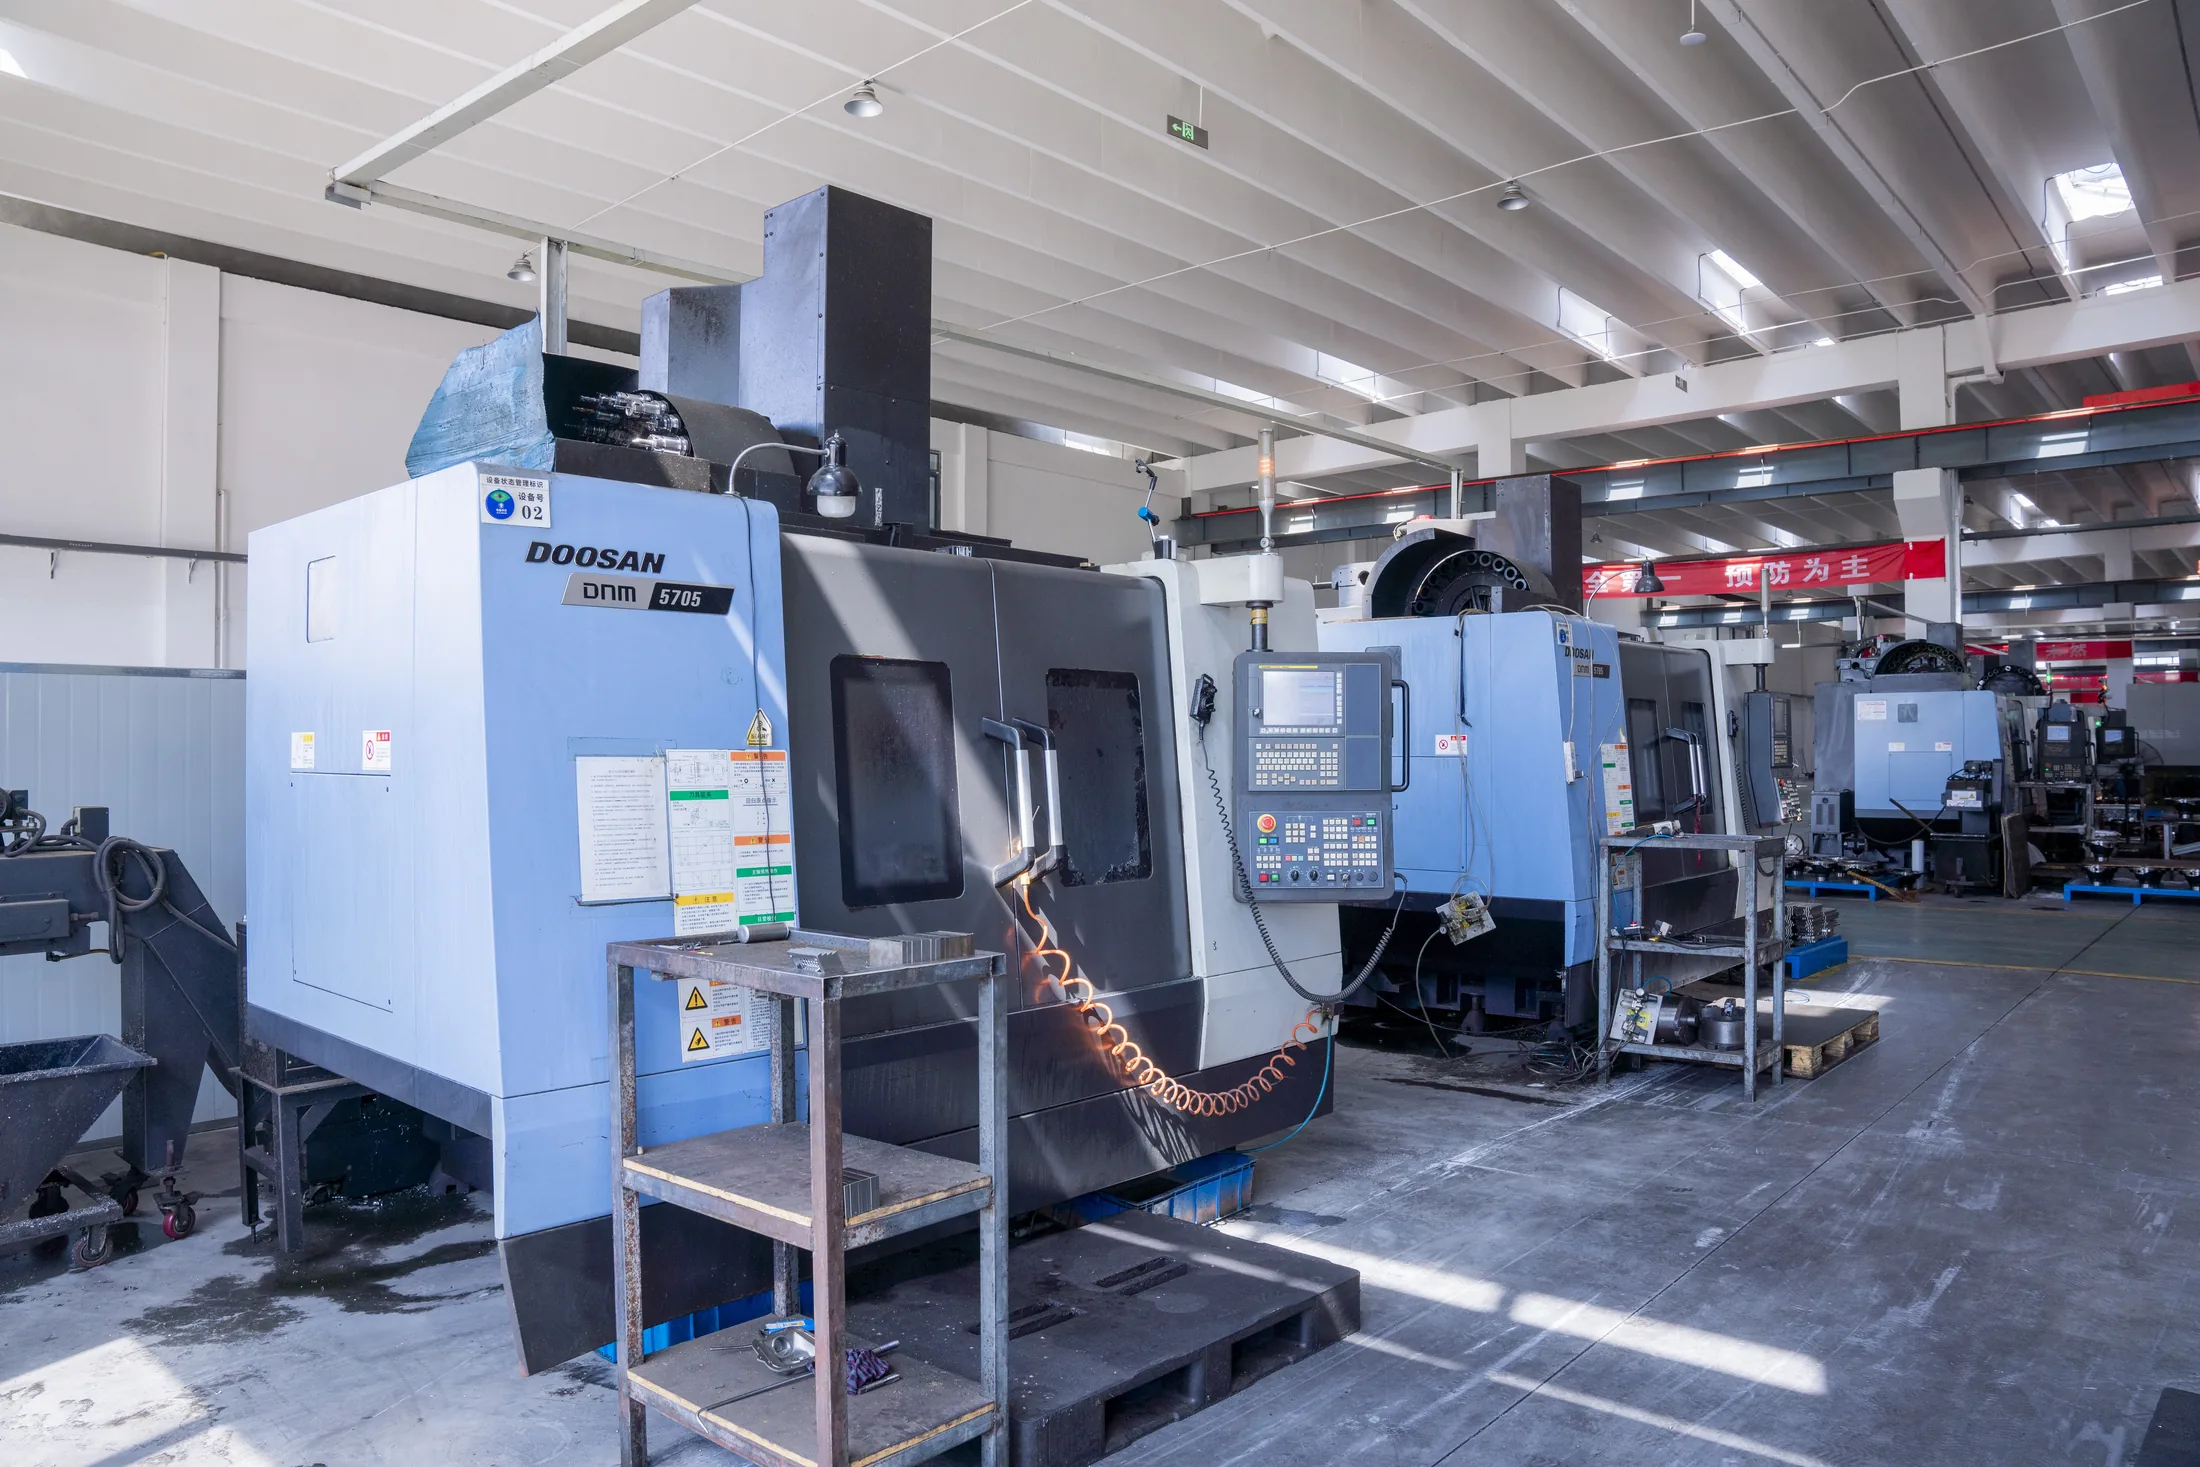
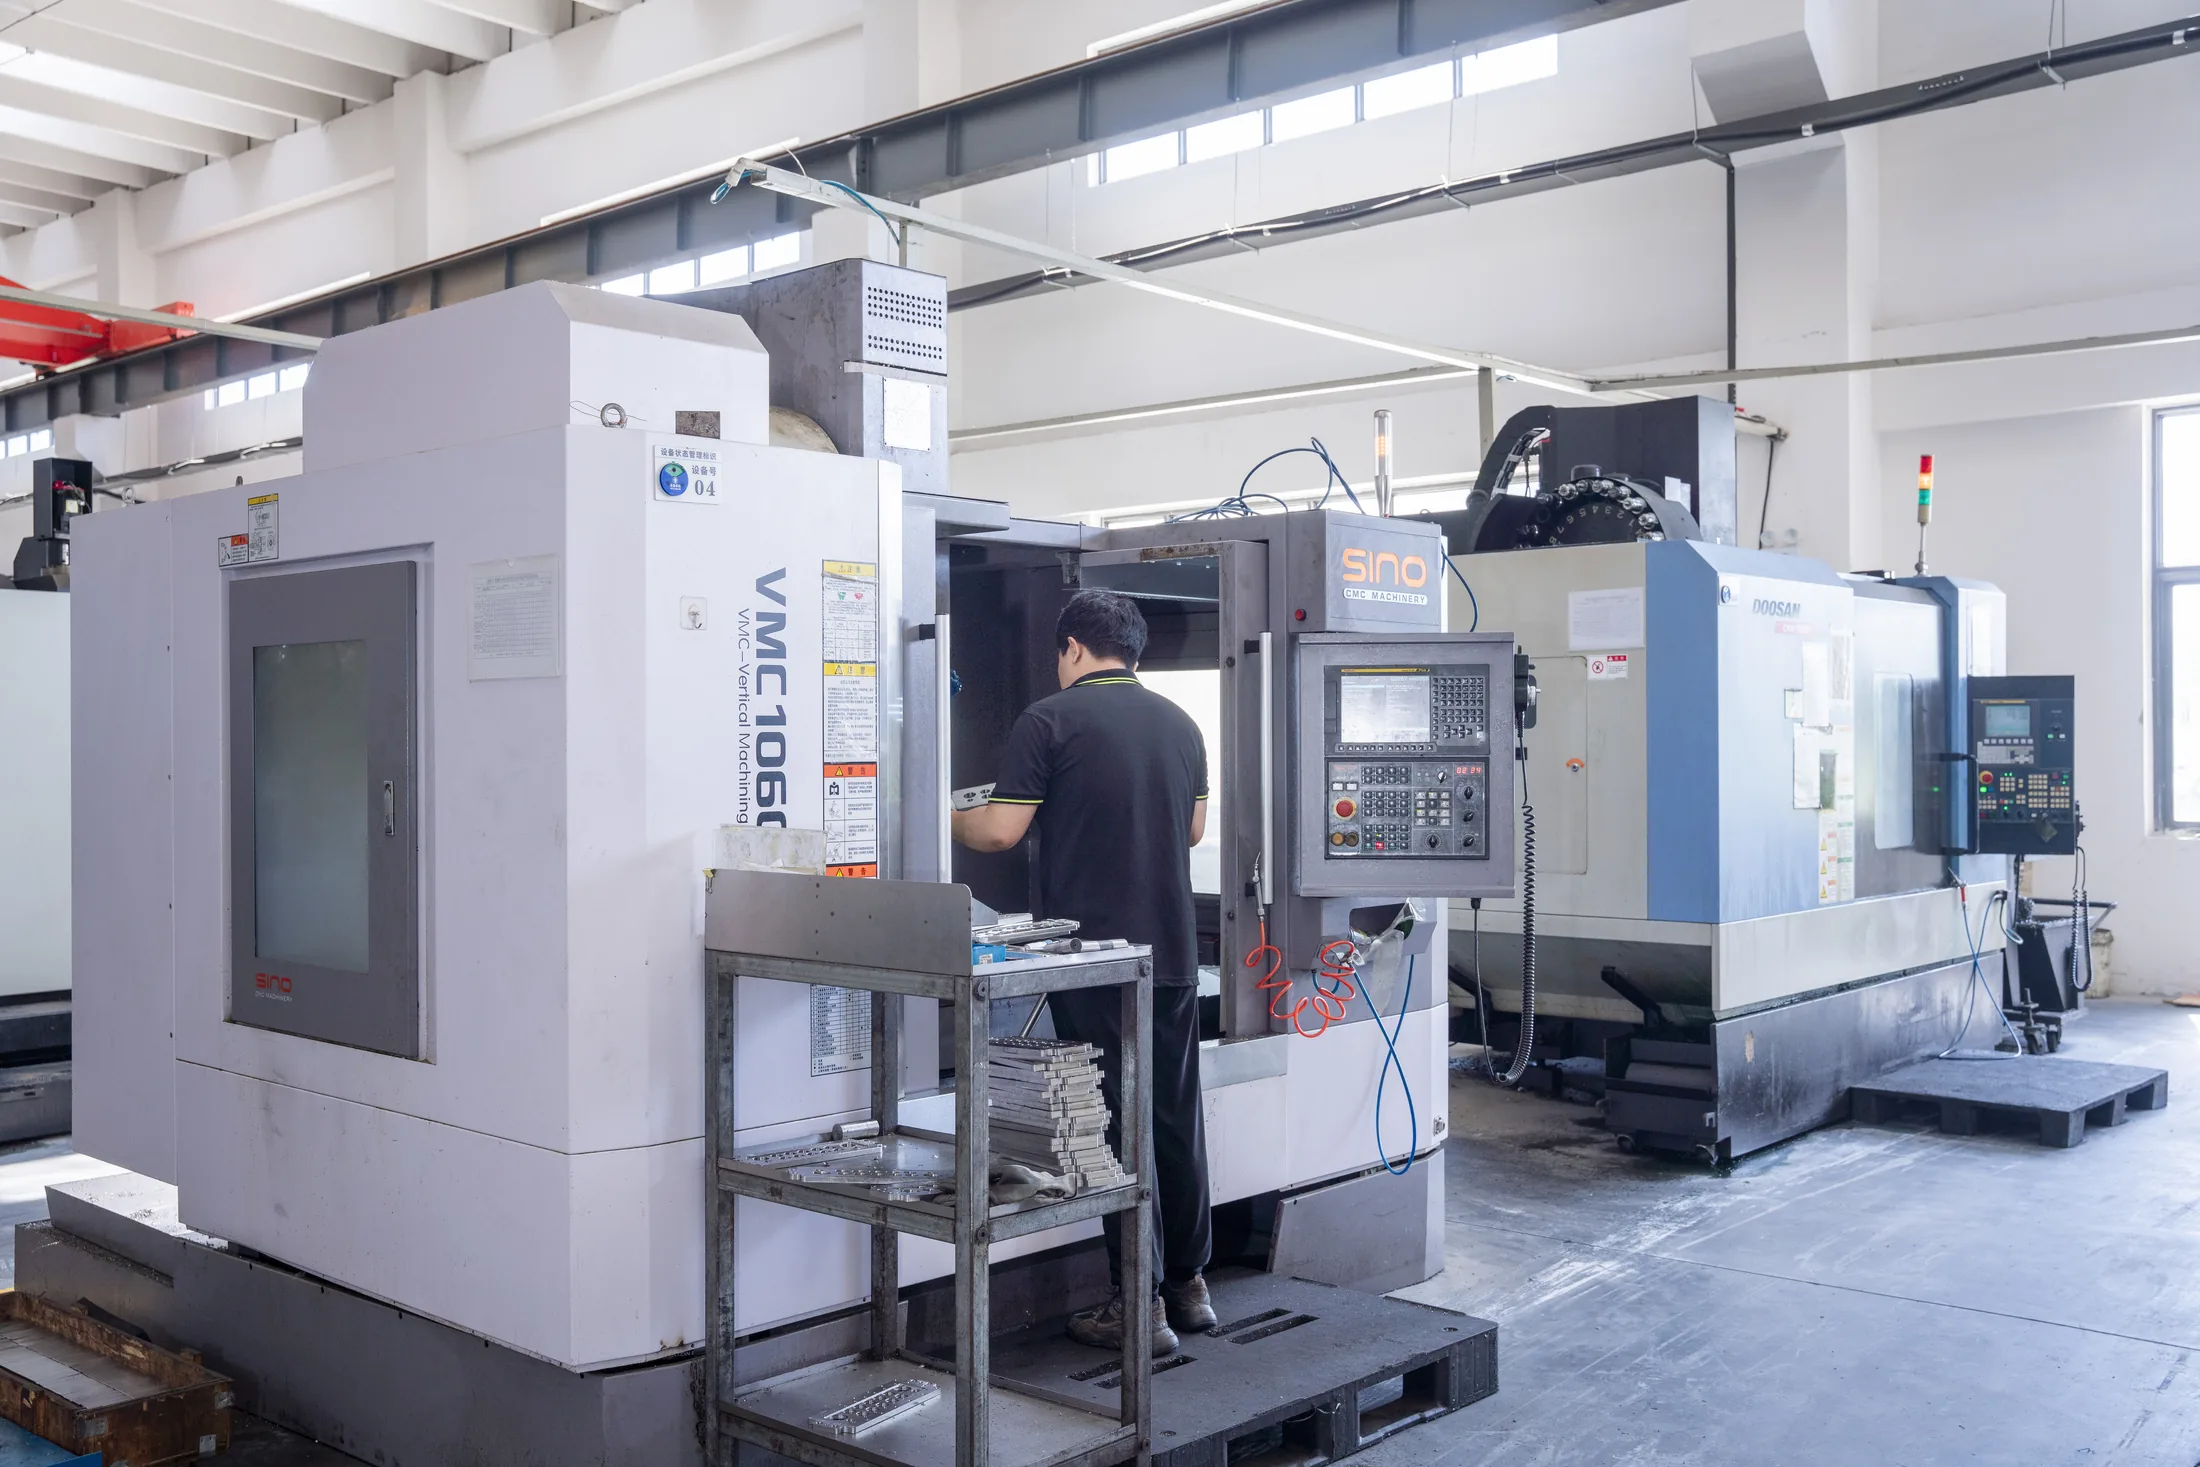
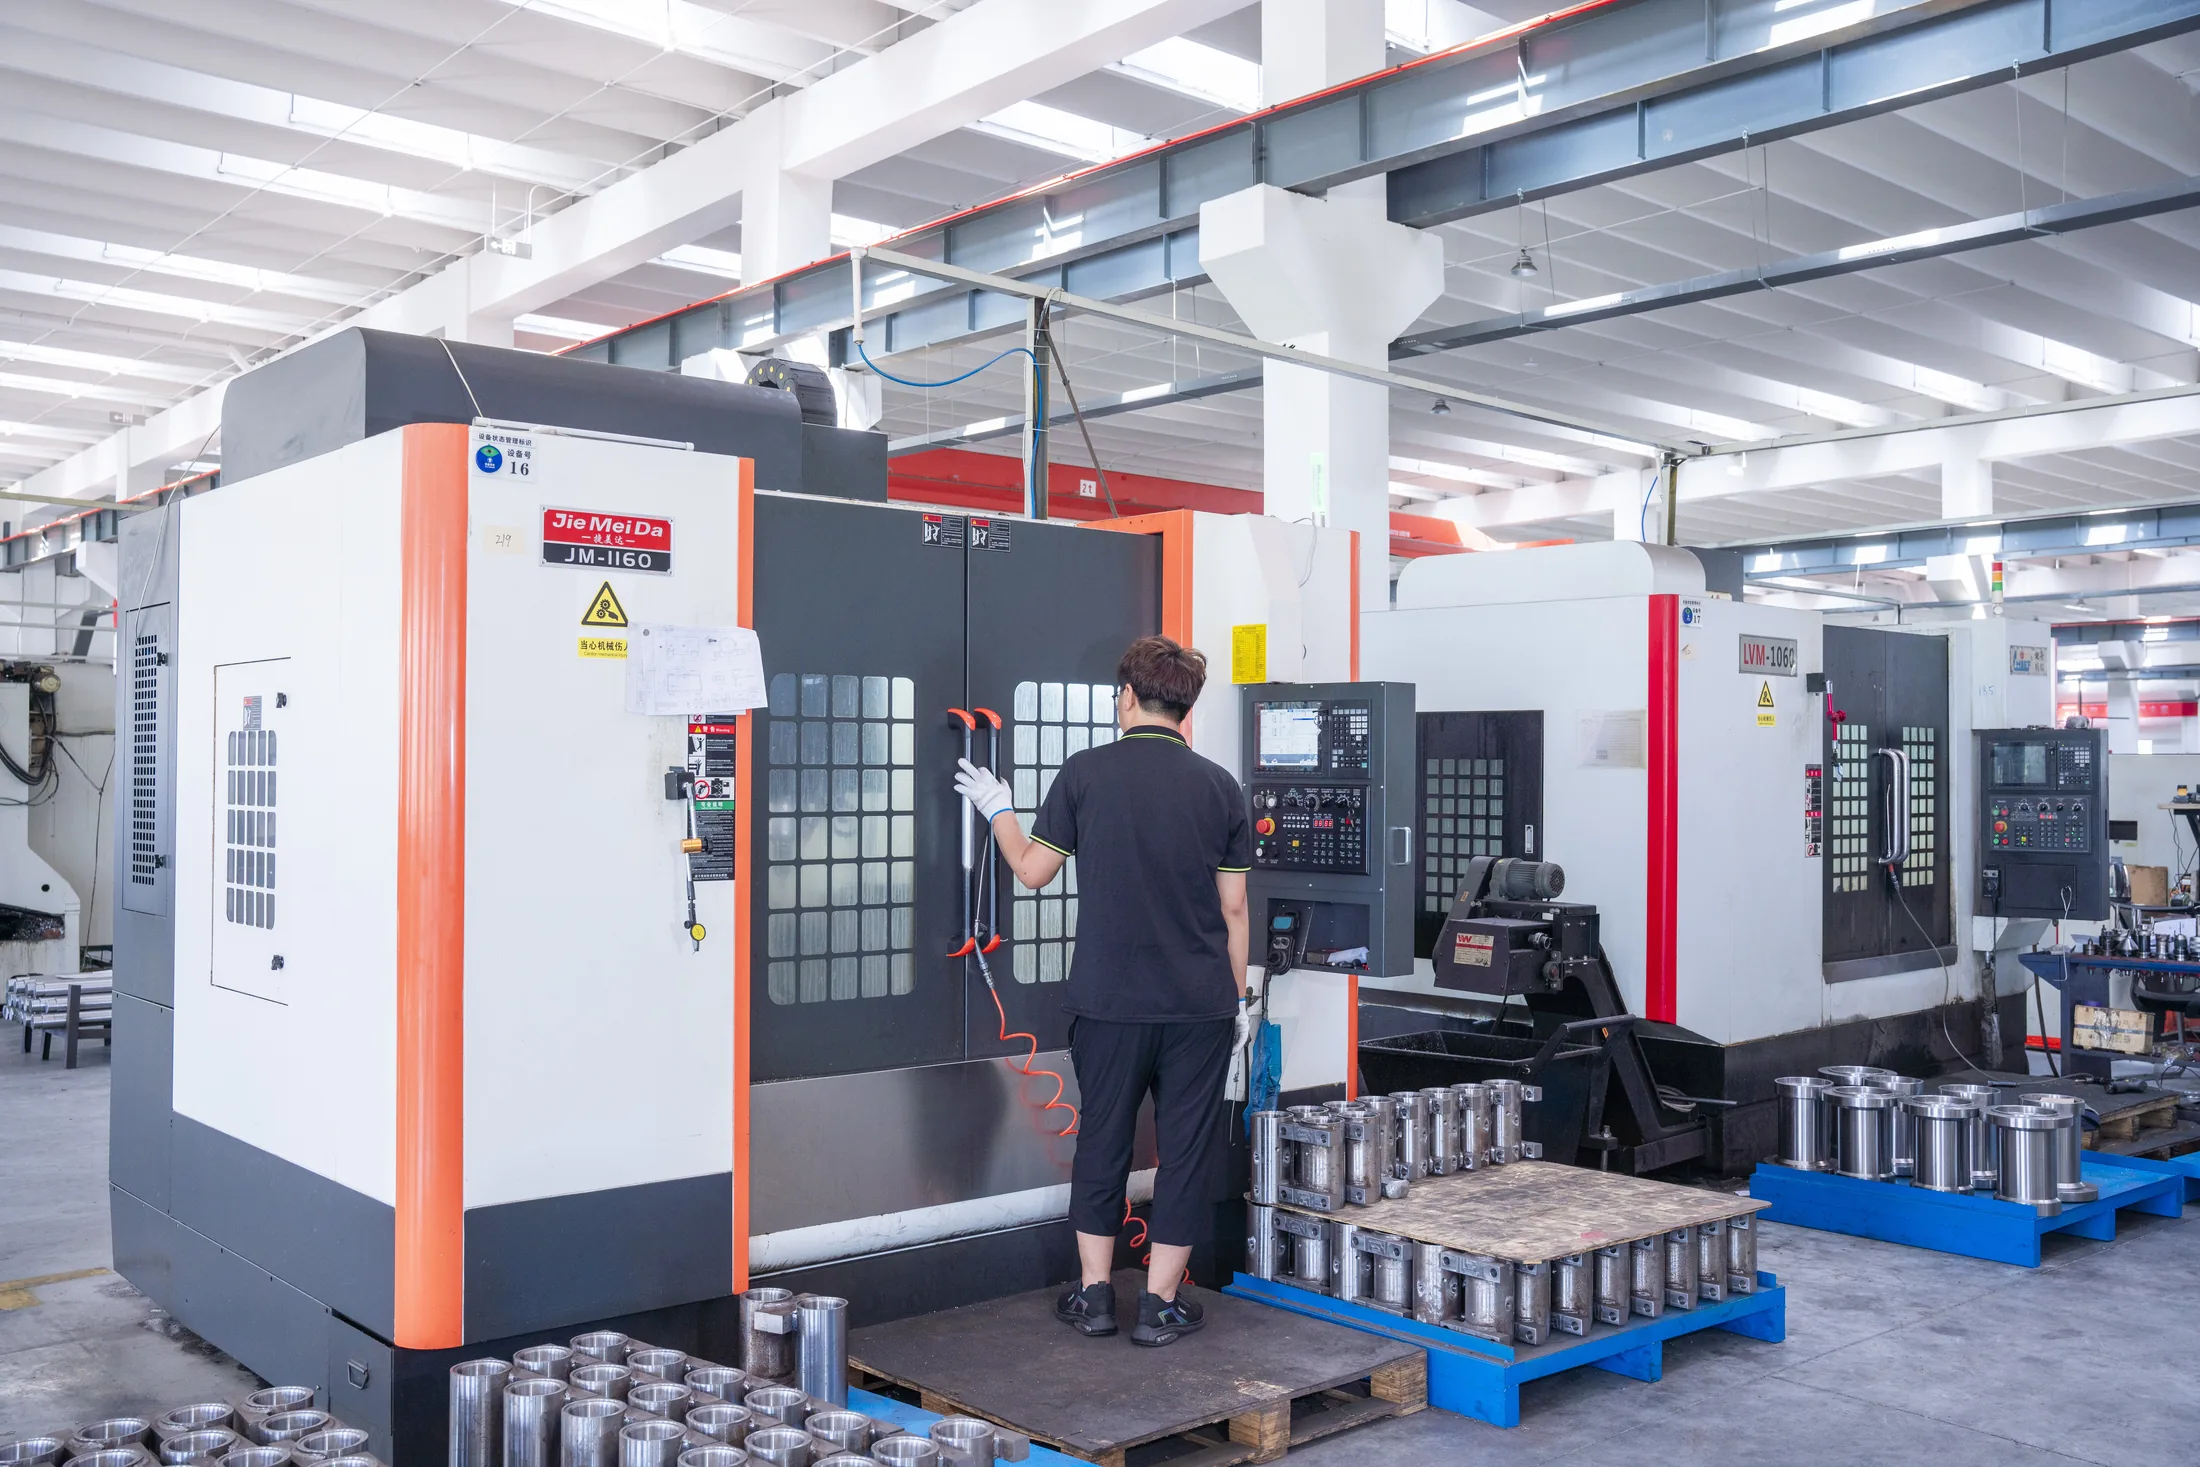
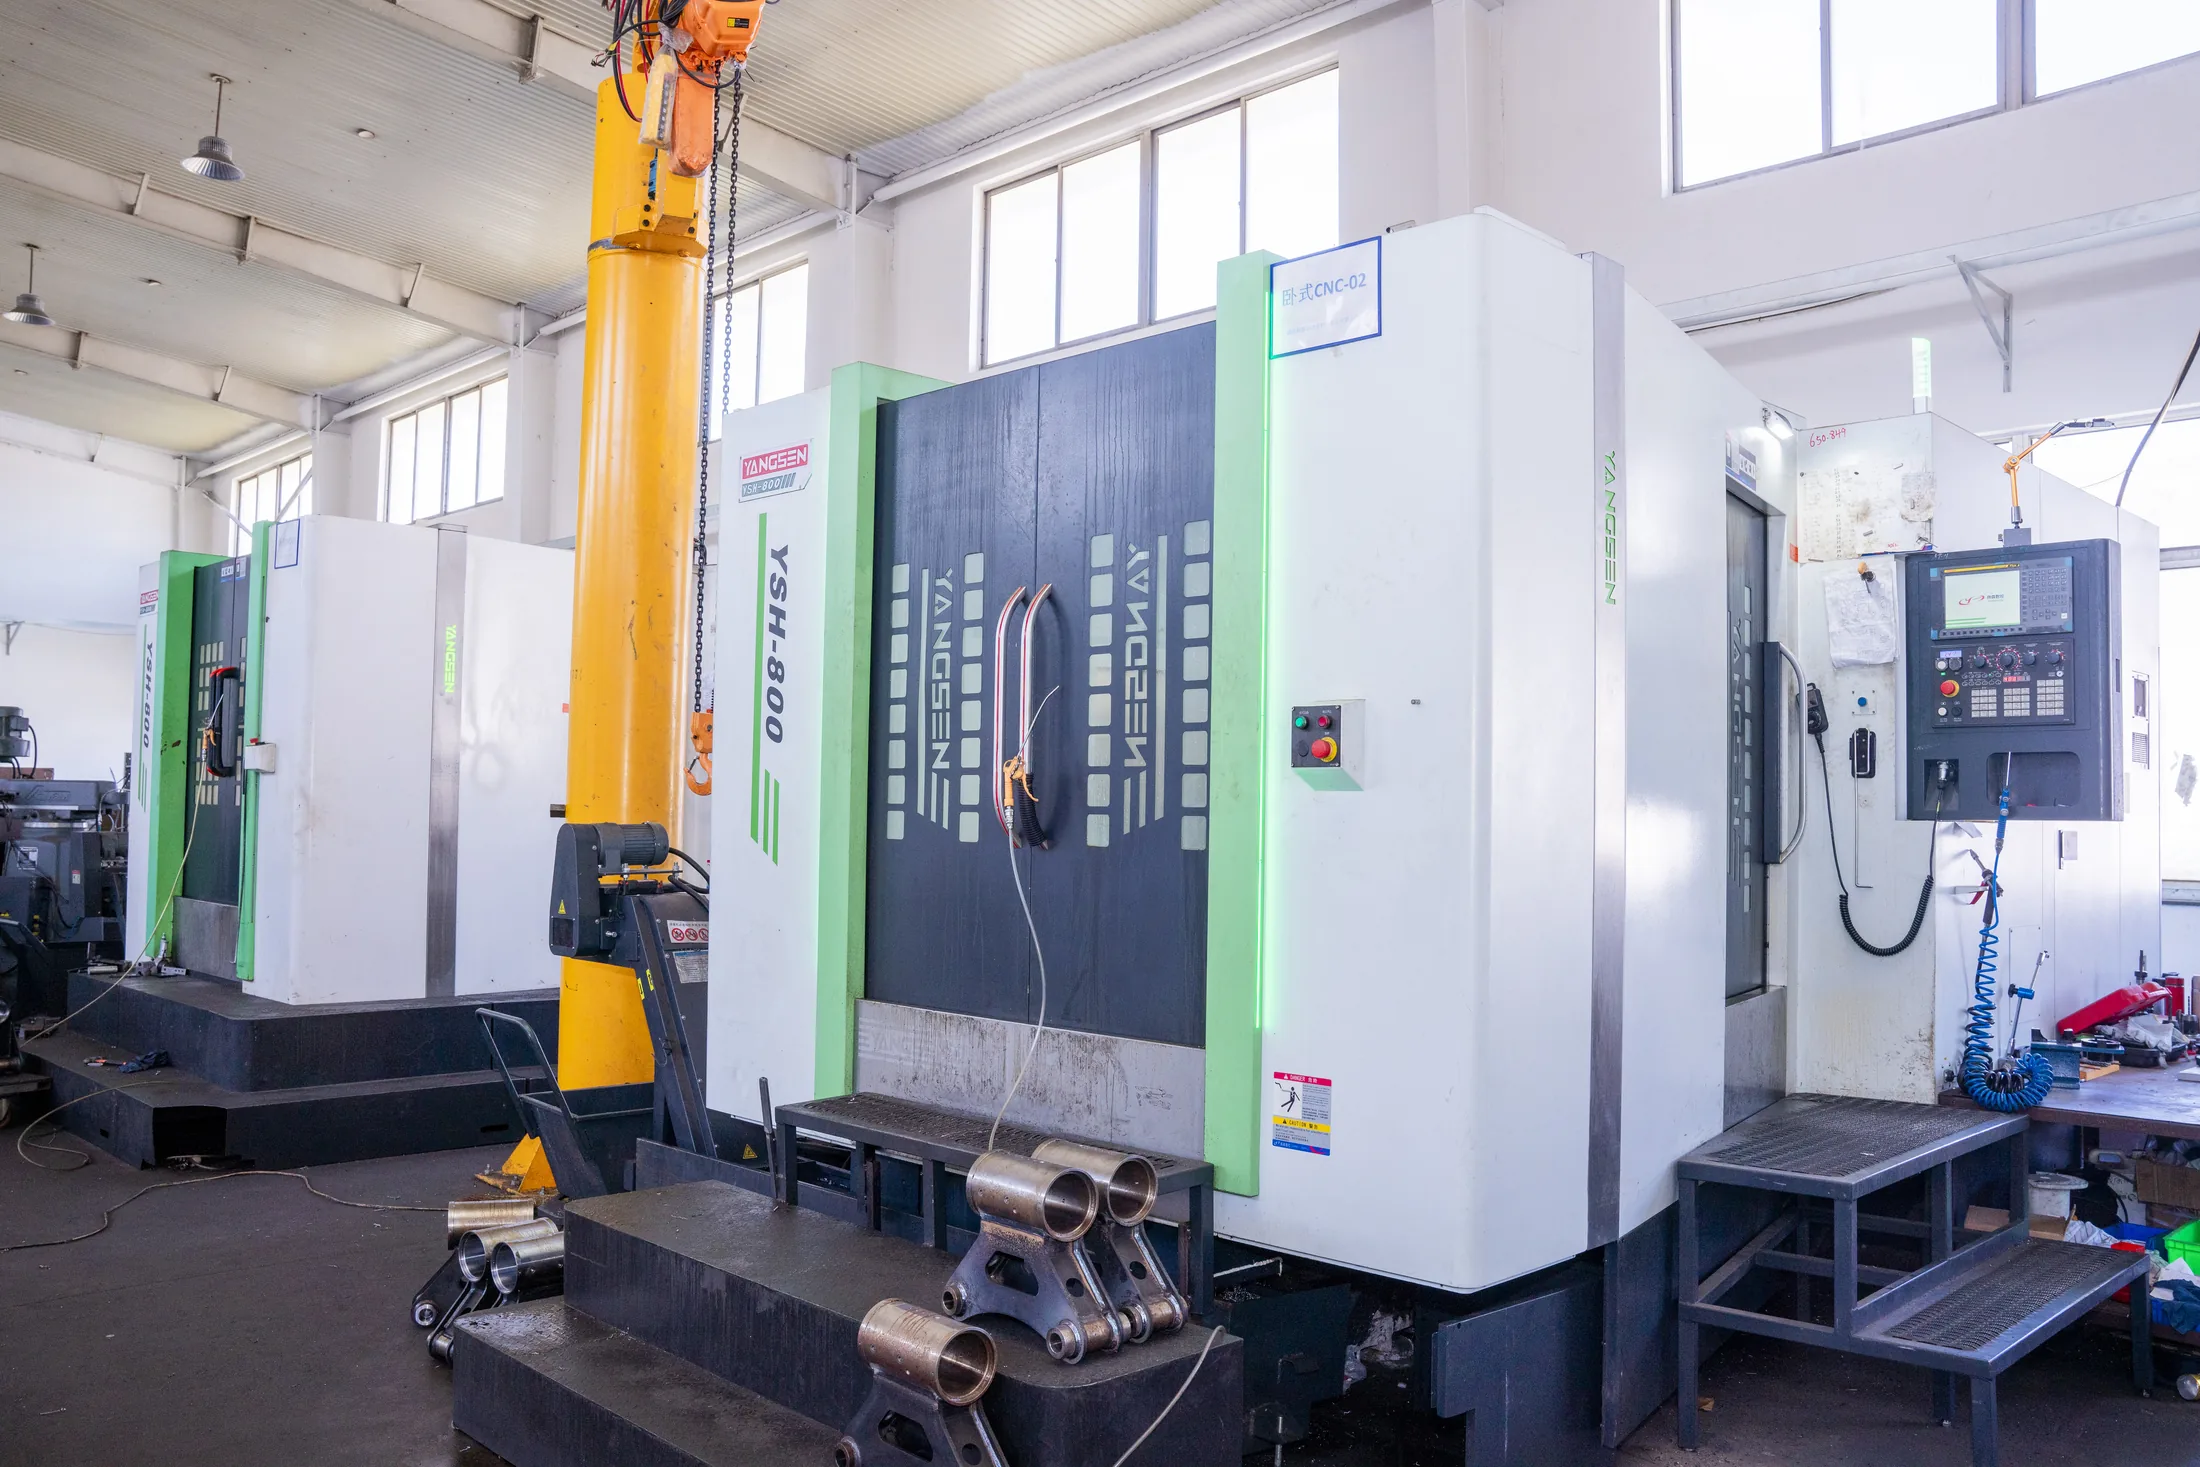
CNC turning & milling lines
Turning centres arranged in flow lines, with overhead crane coverage — spline grinding and finish machining are done in-house, not outsourced. See the full machine park.
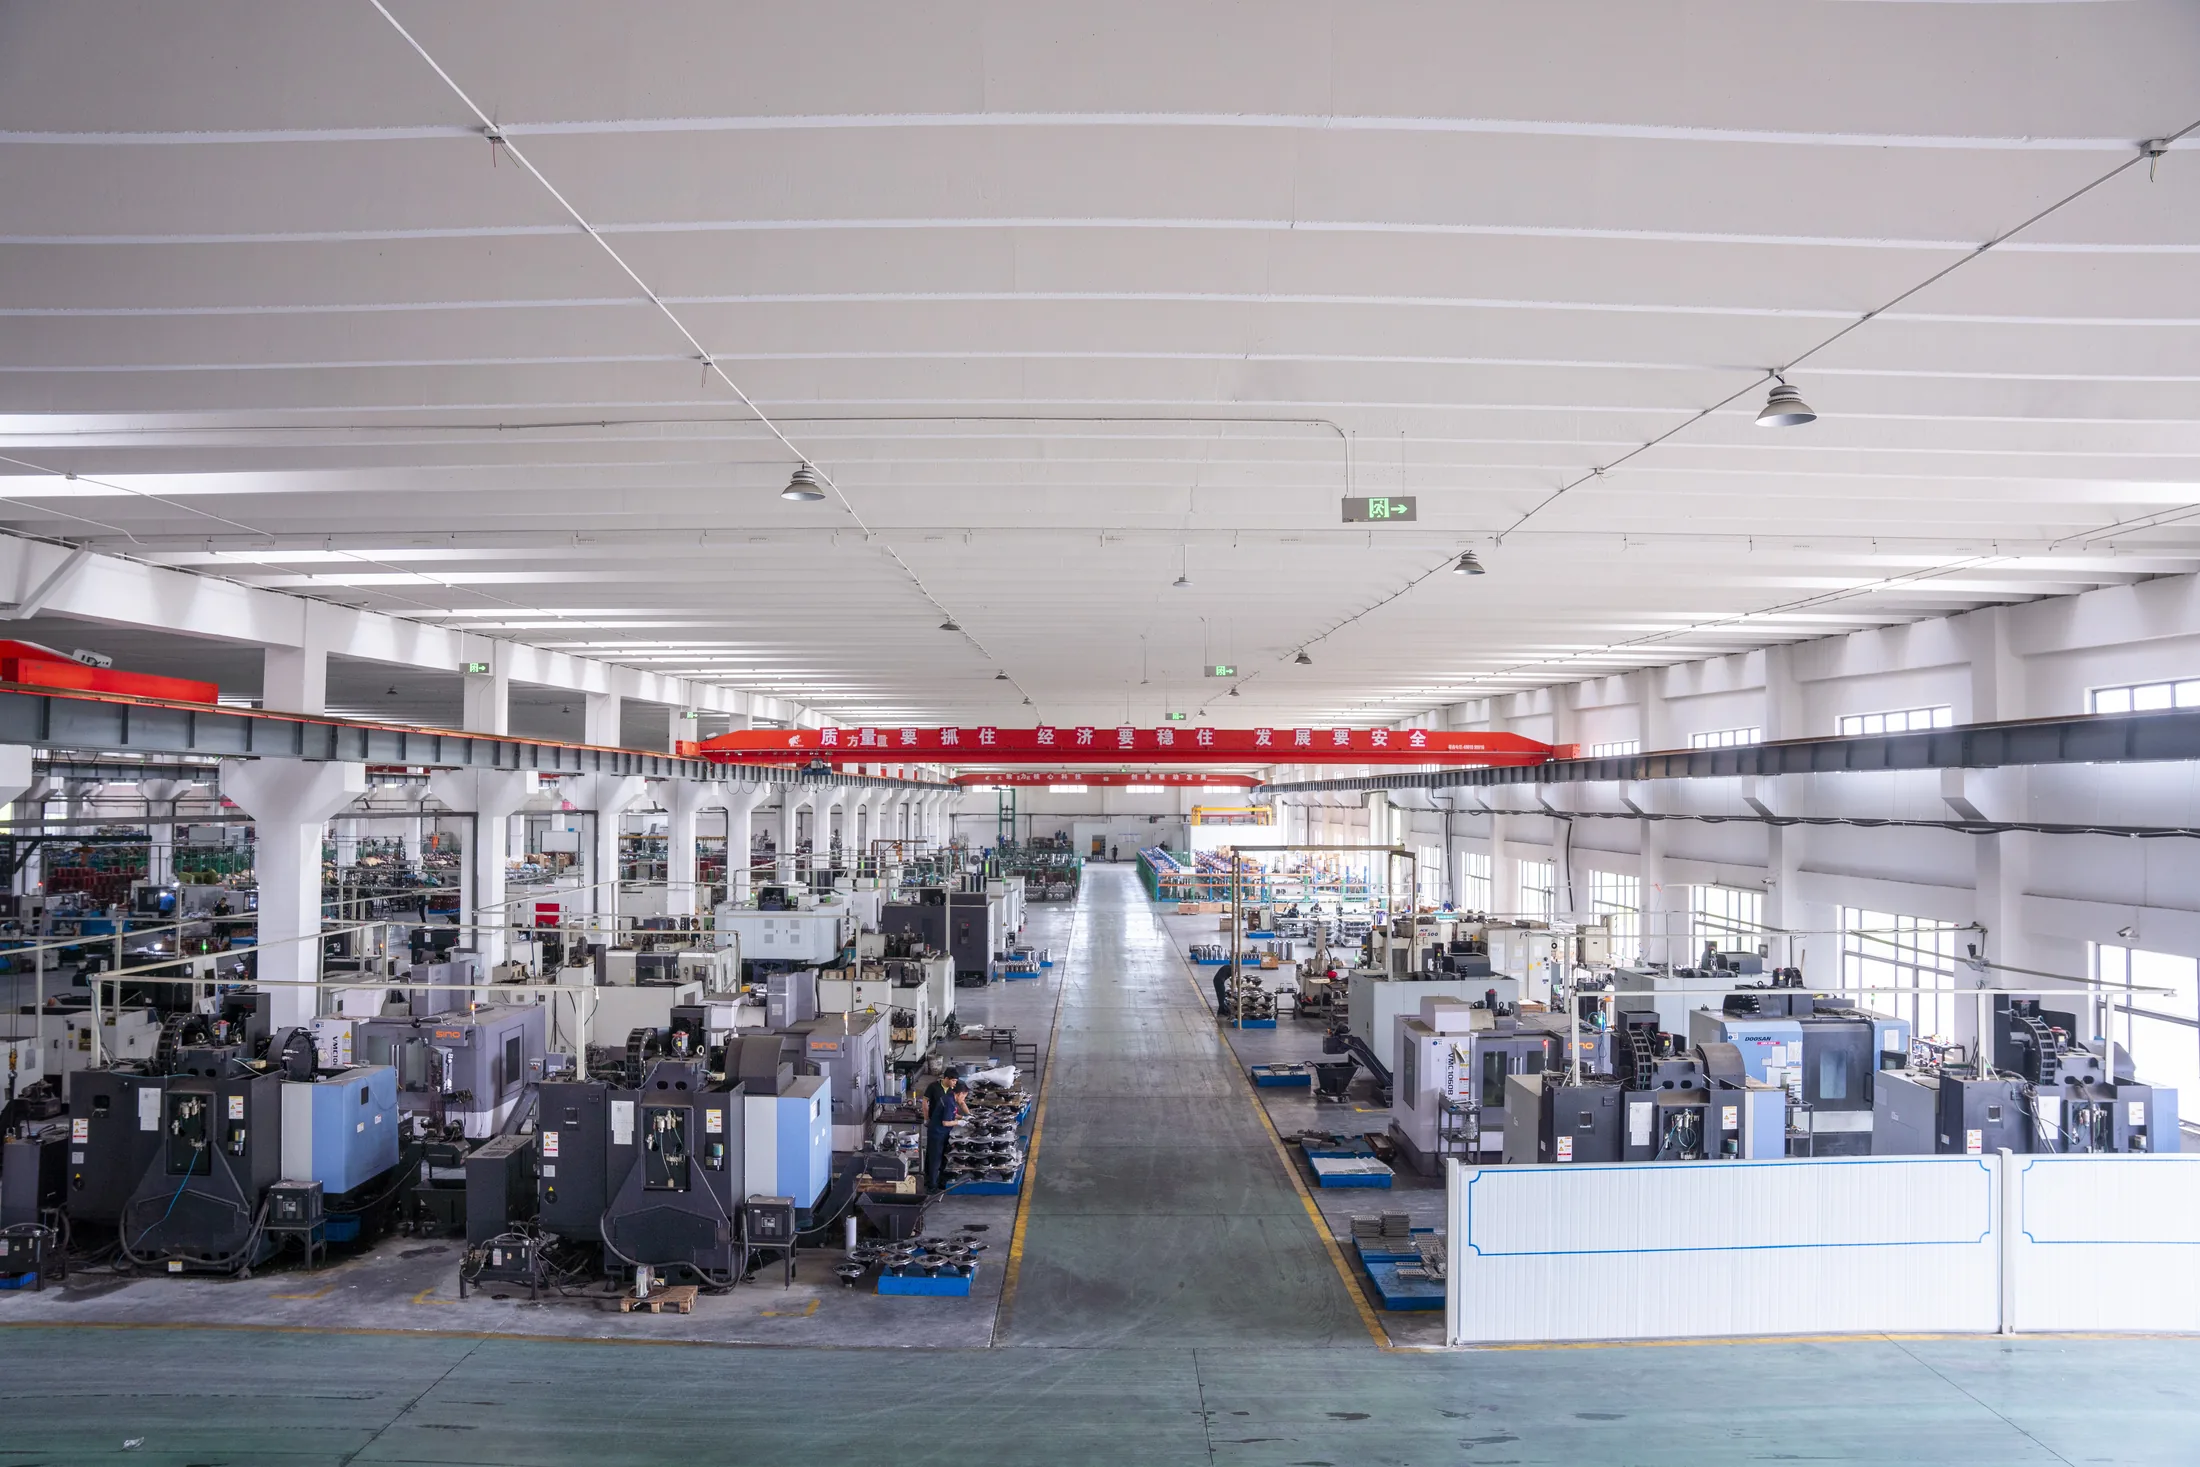
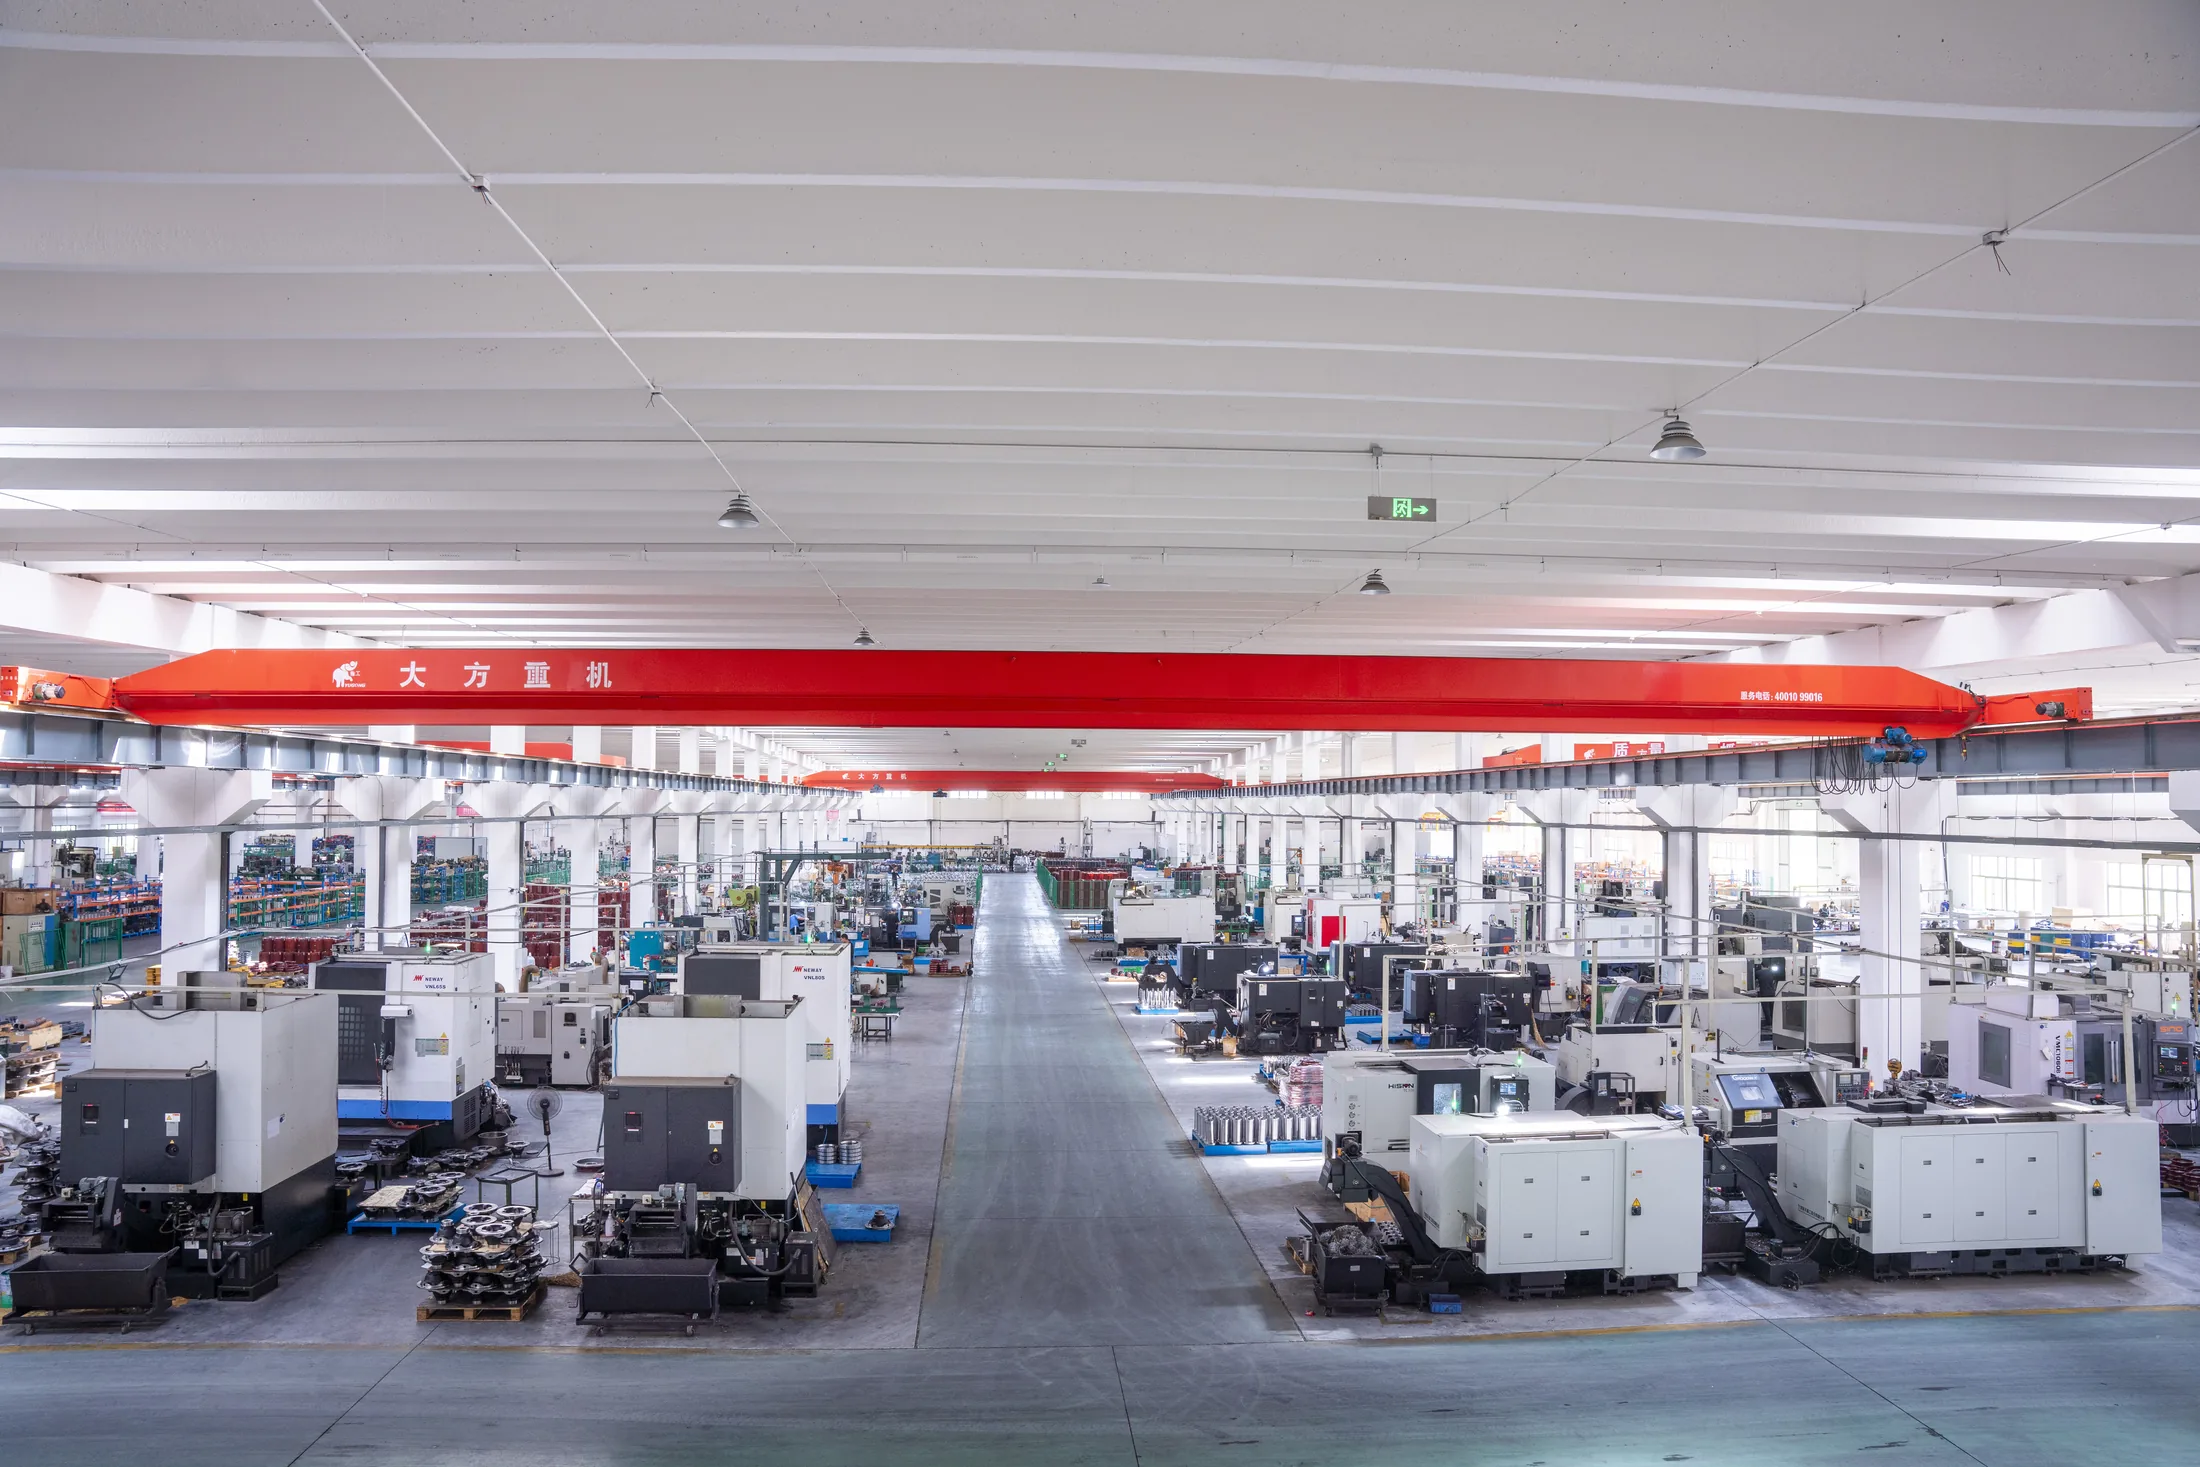
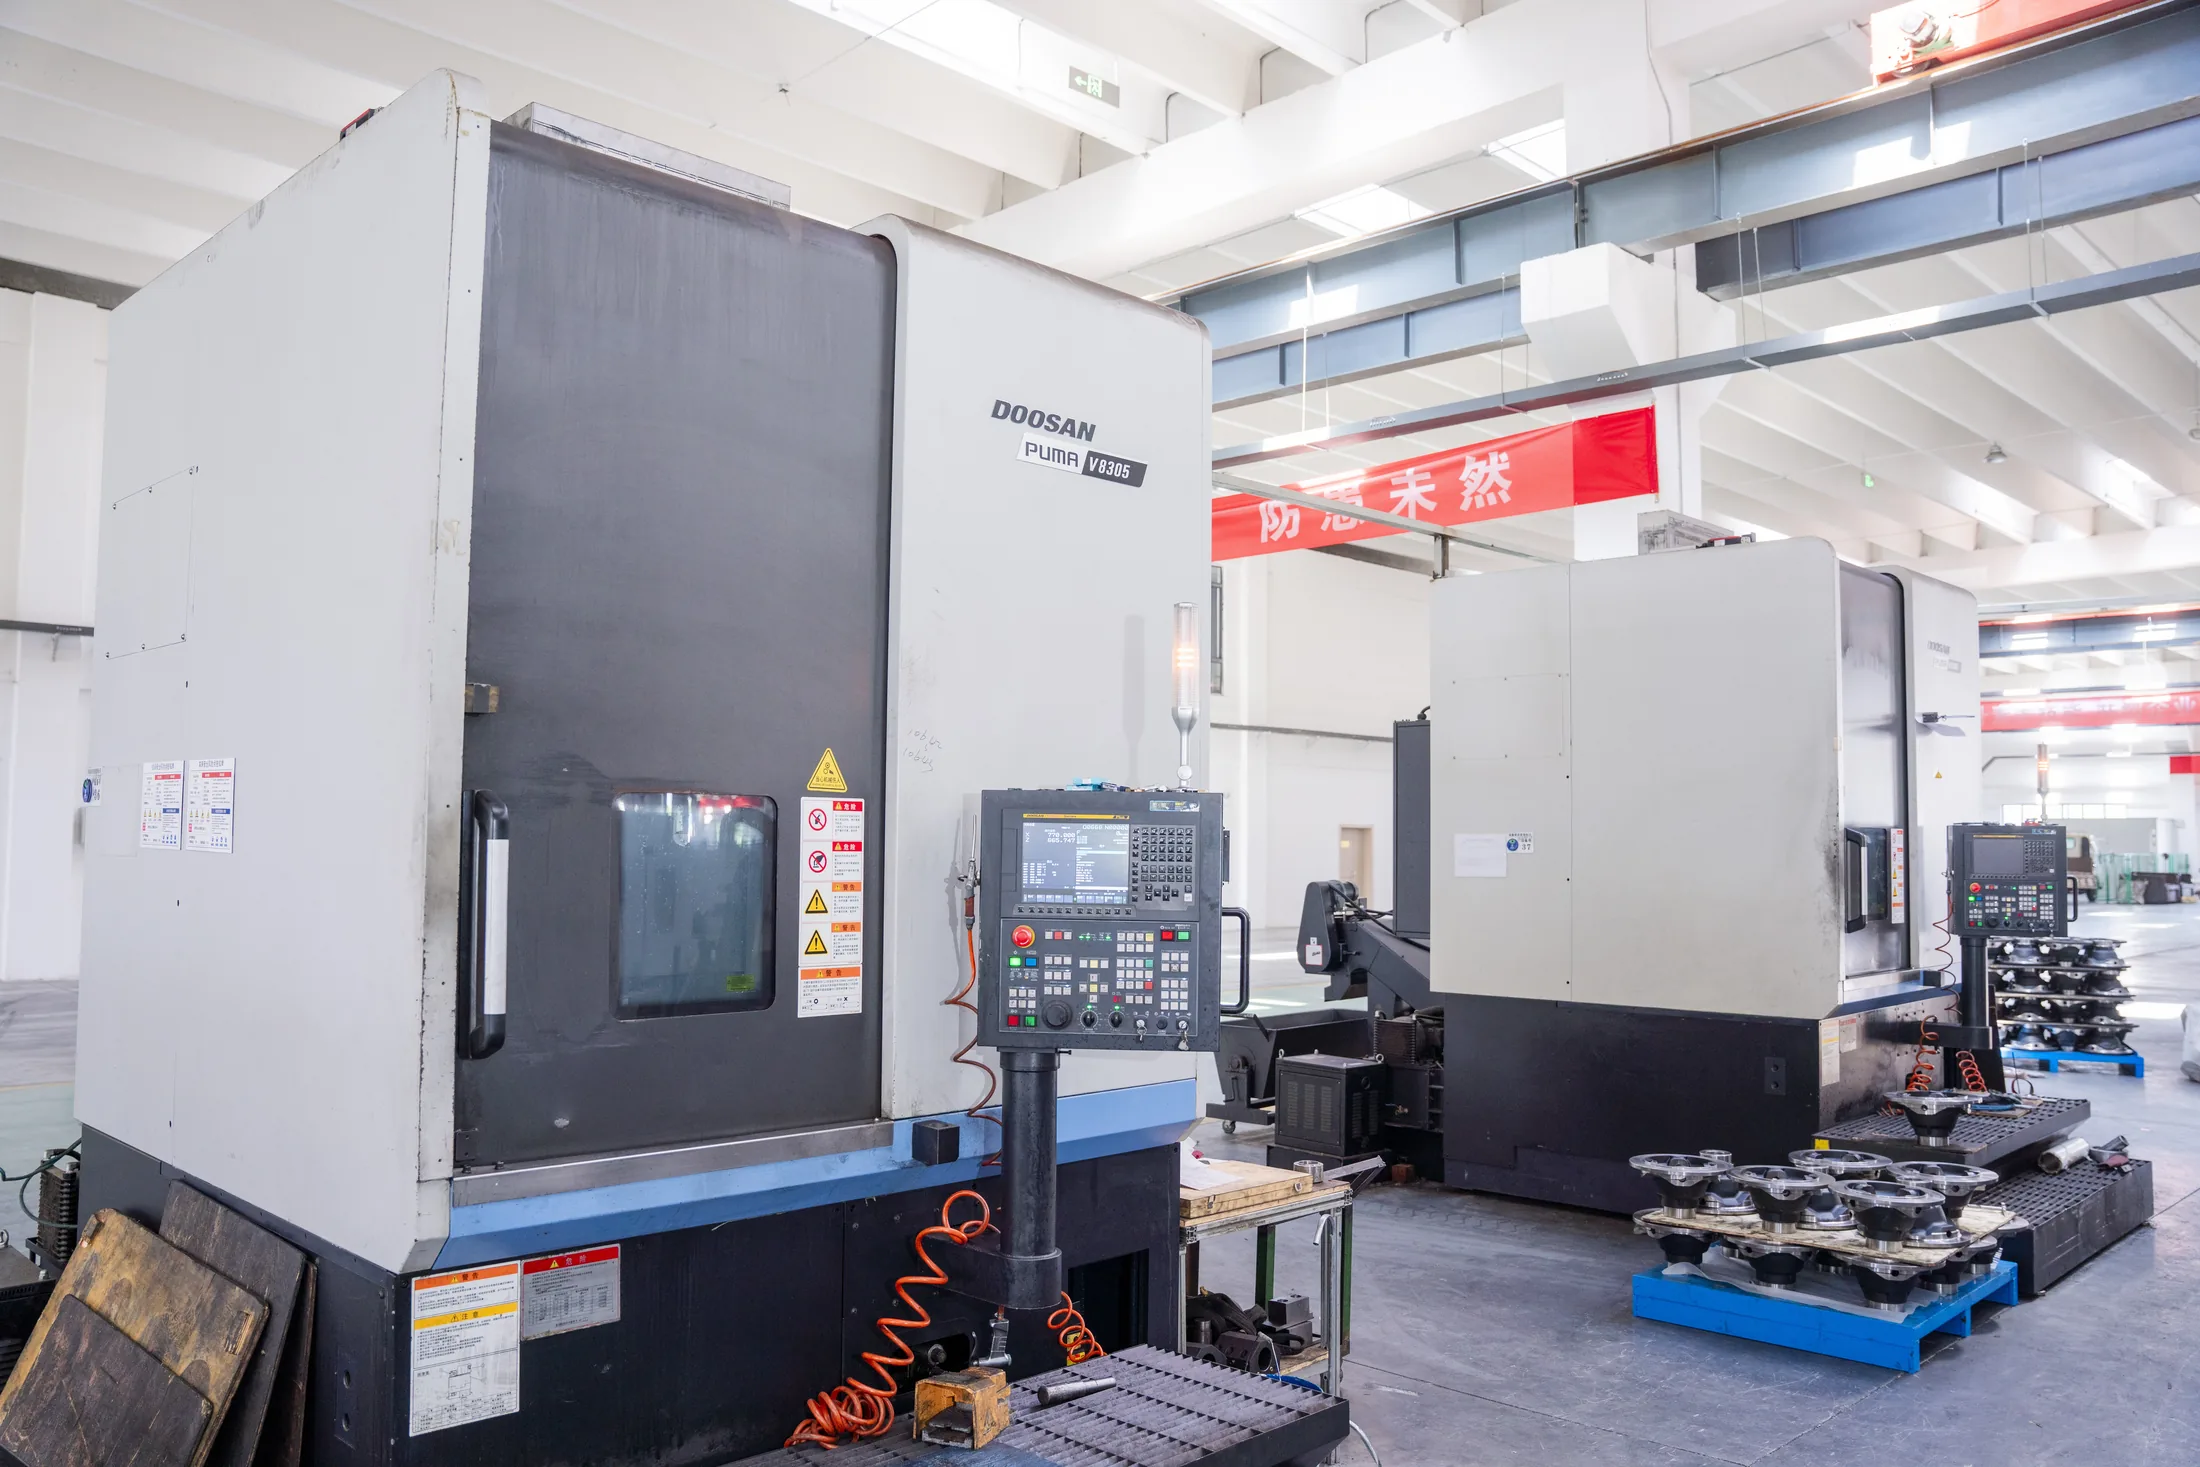
Big flanges, one chucking
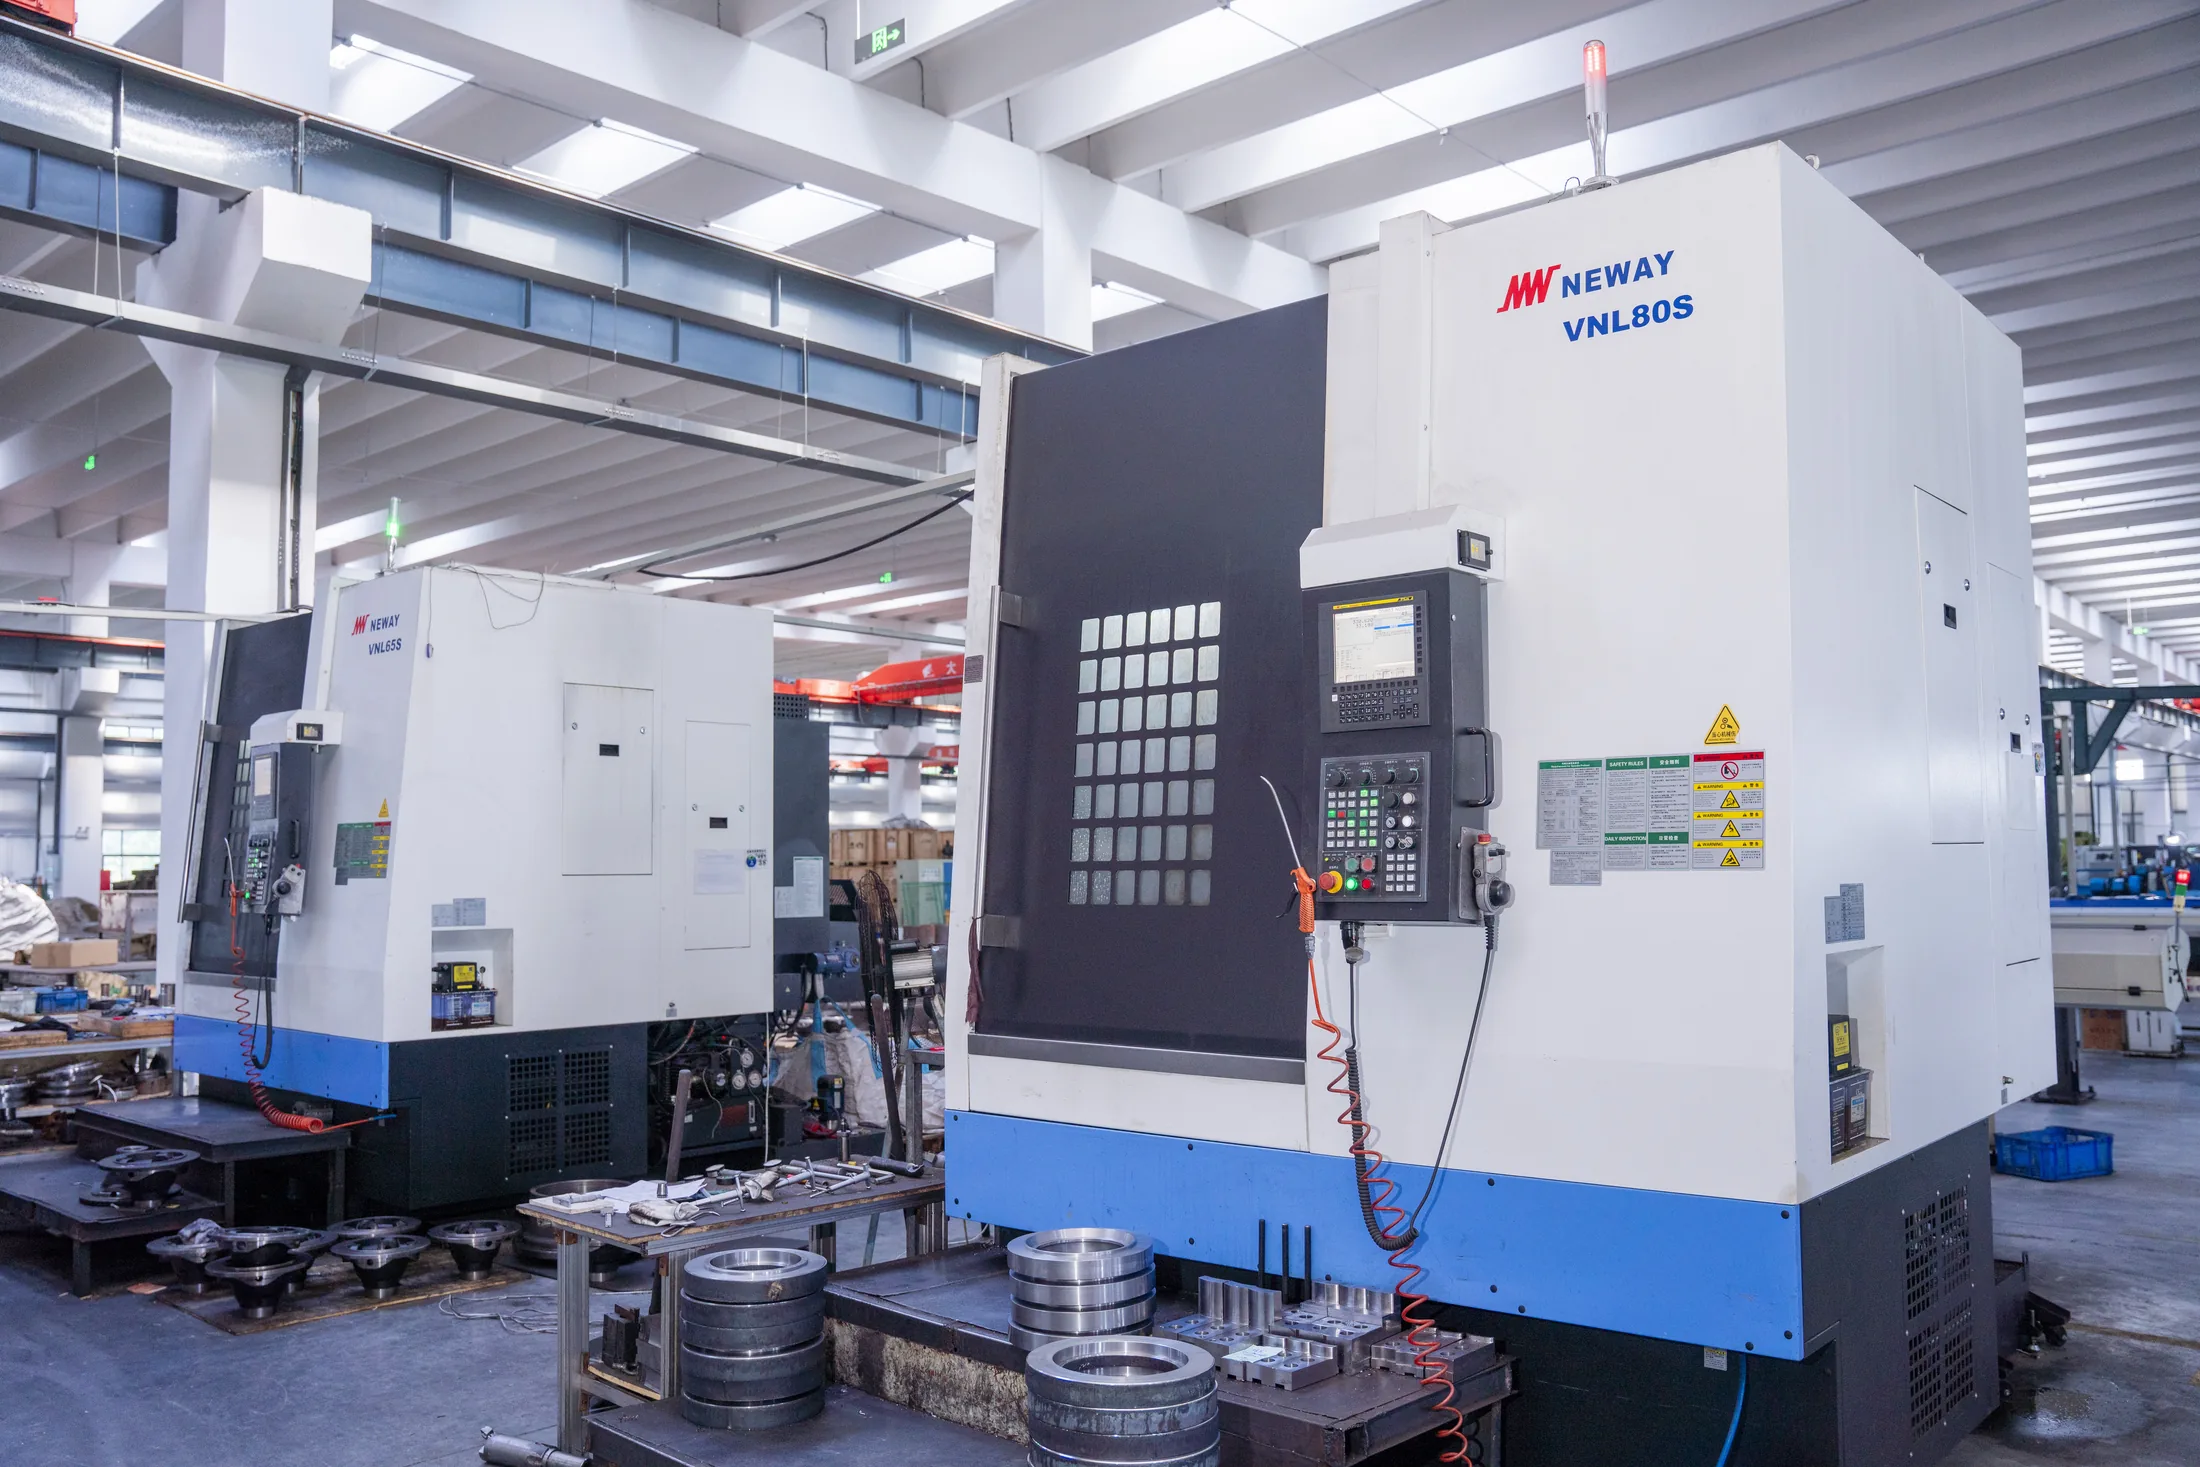
Shafts, pistons, pins
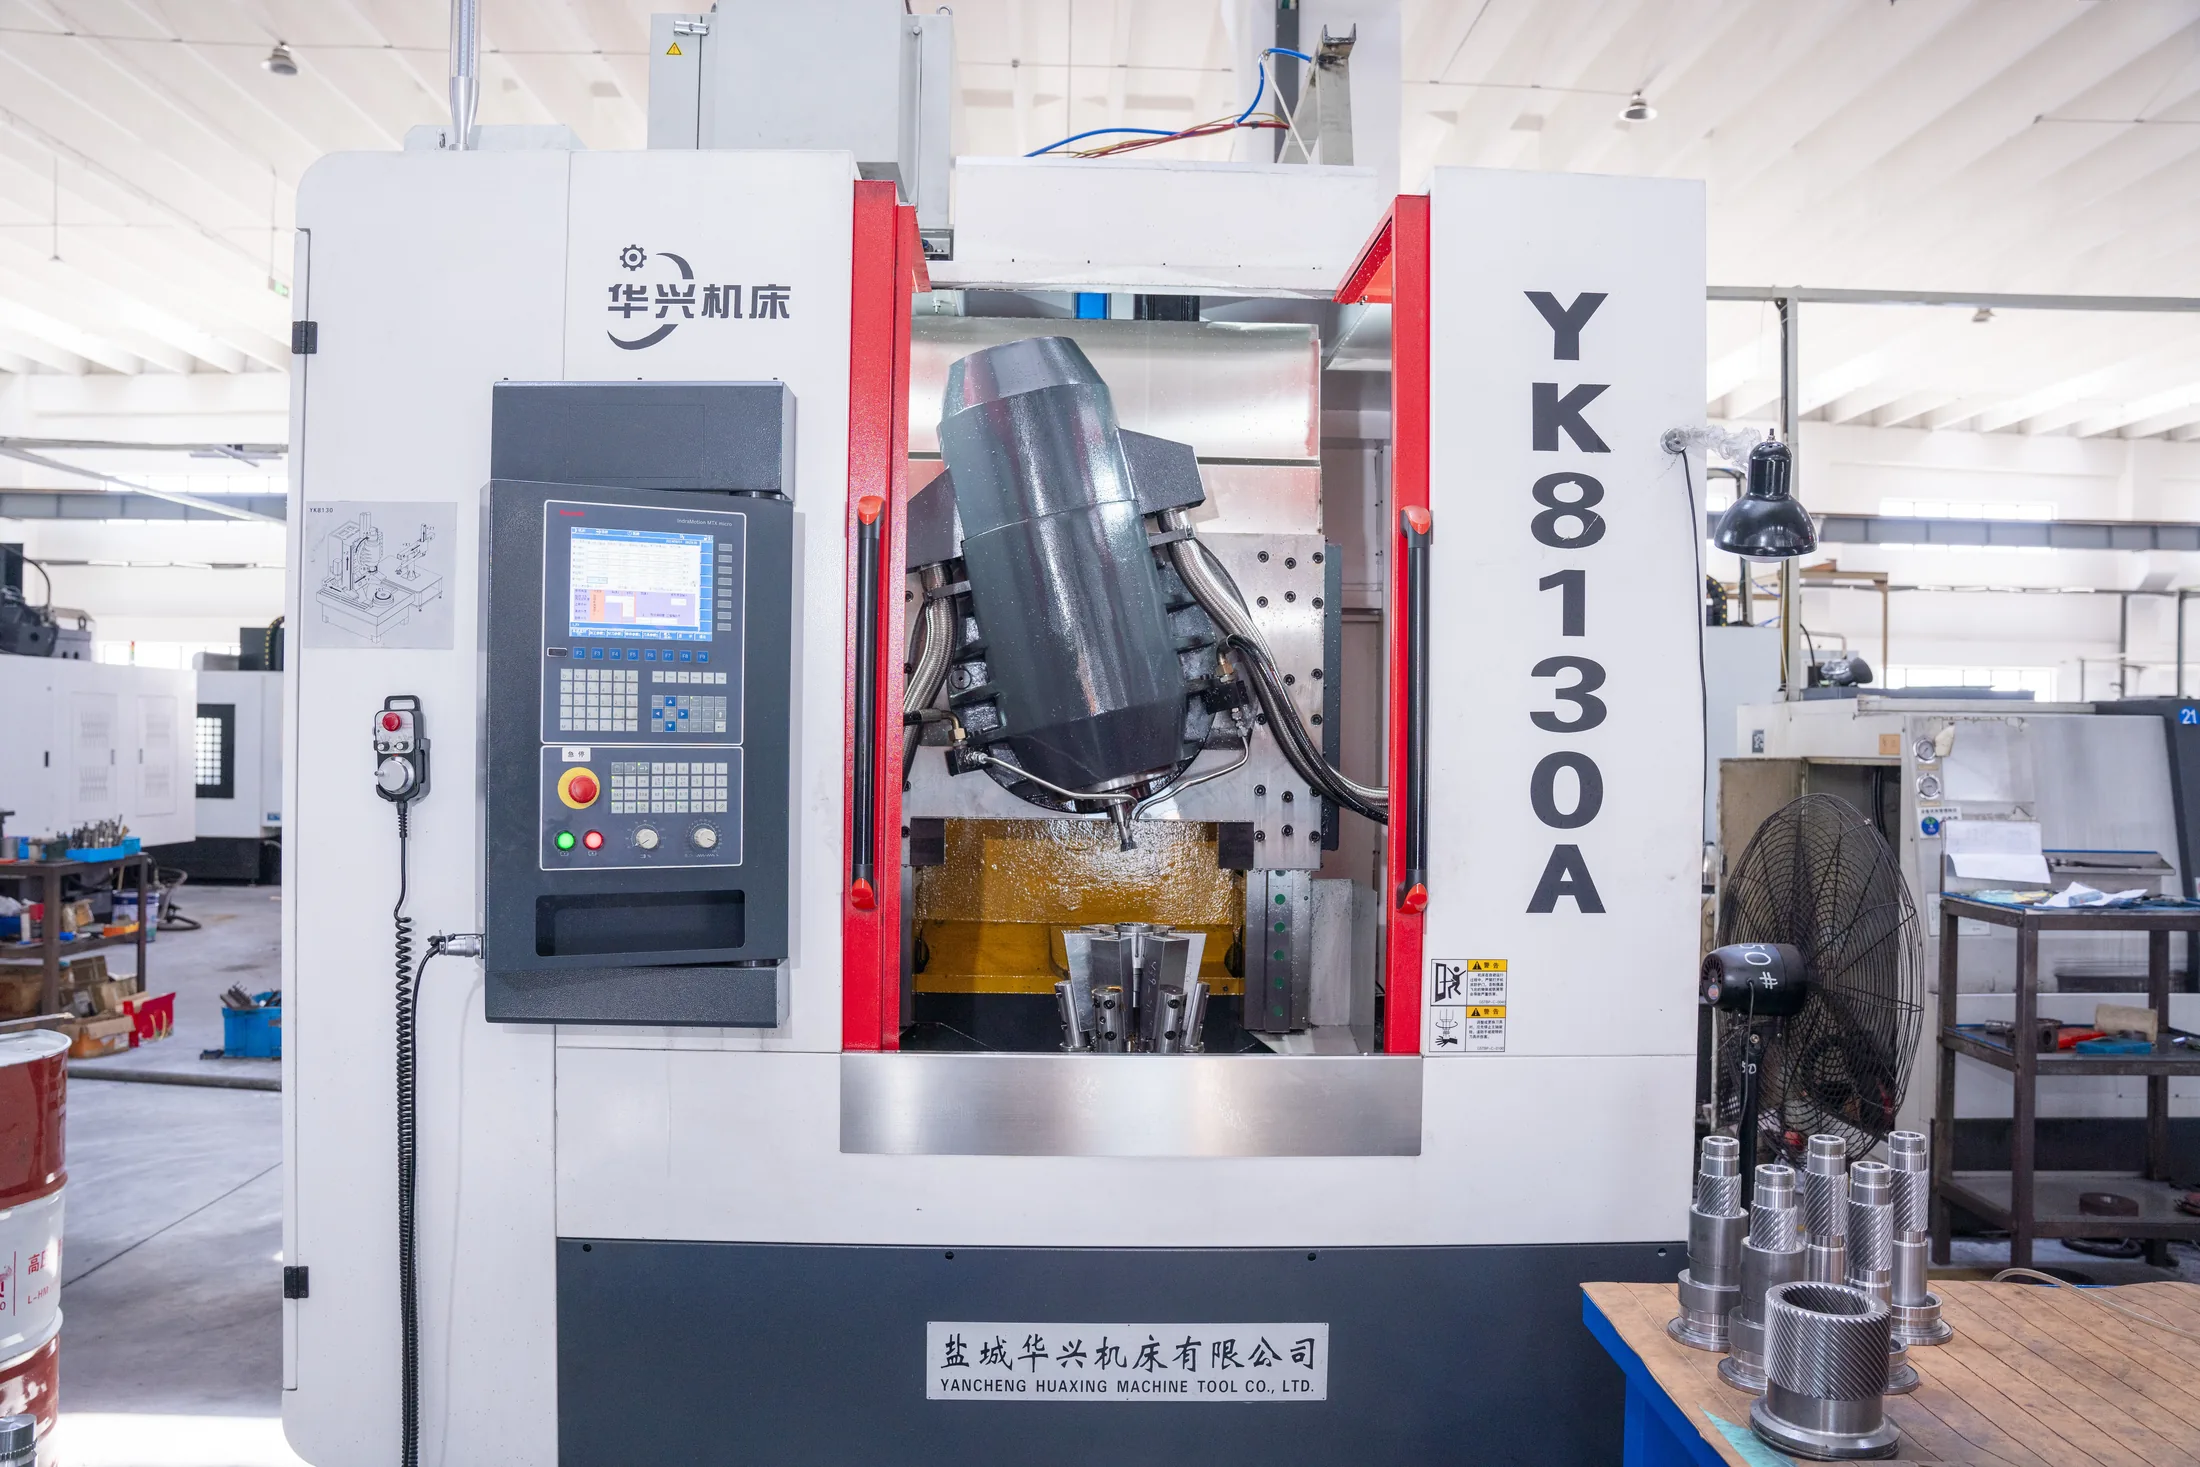
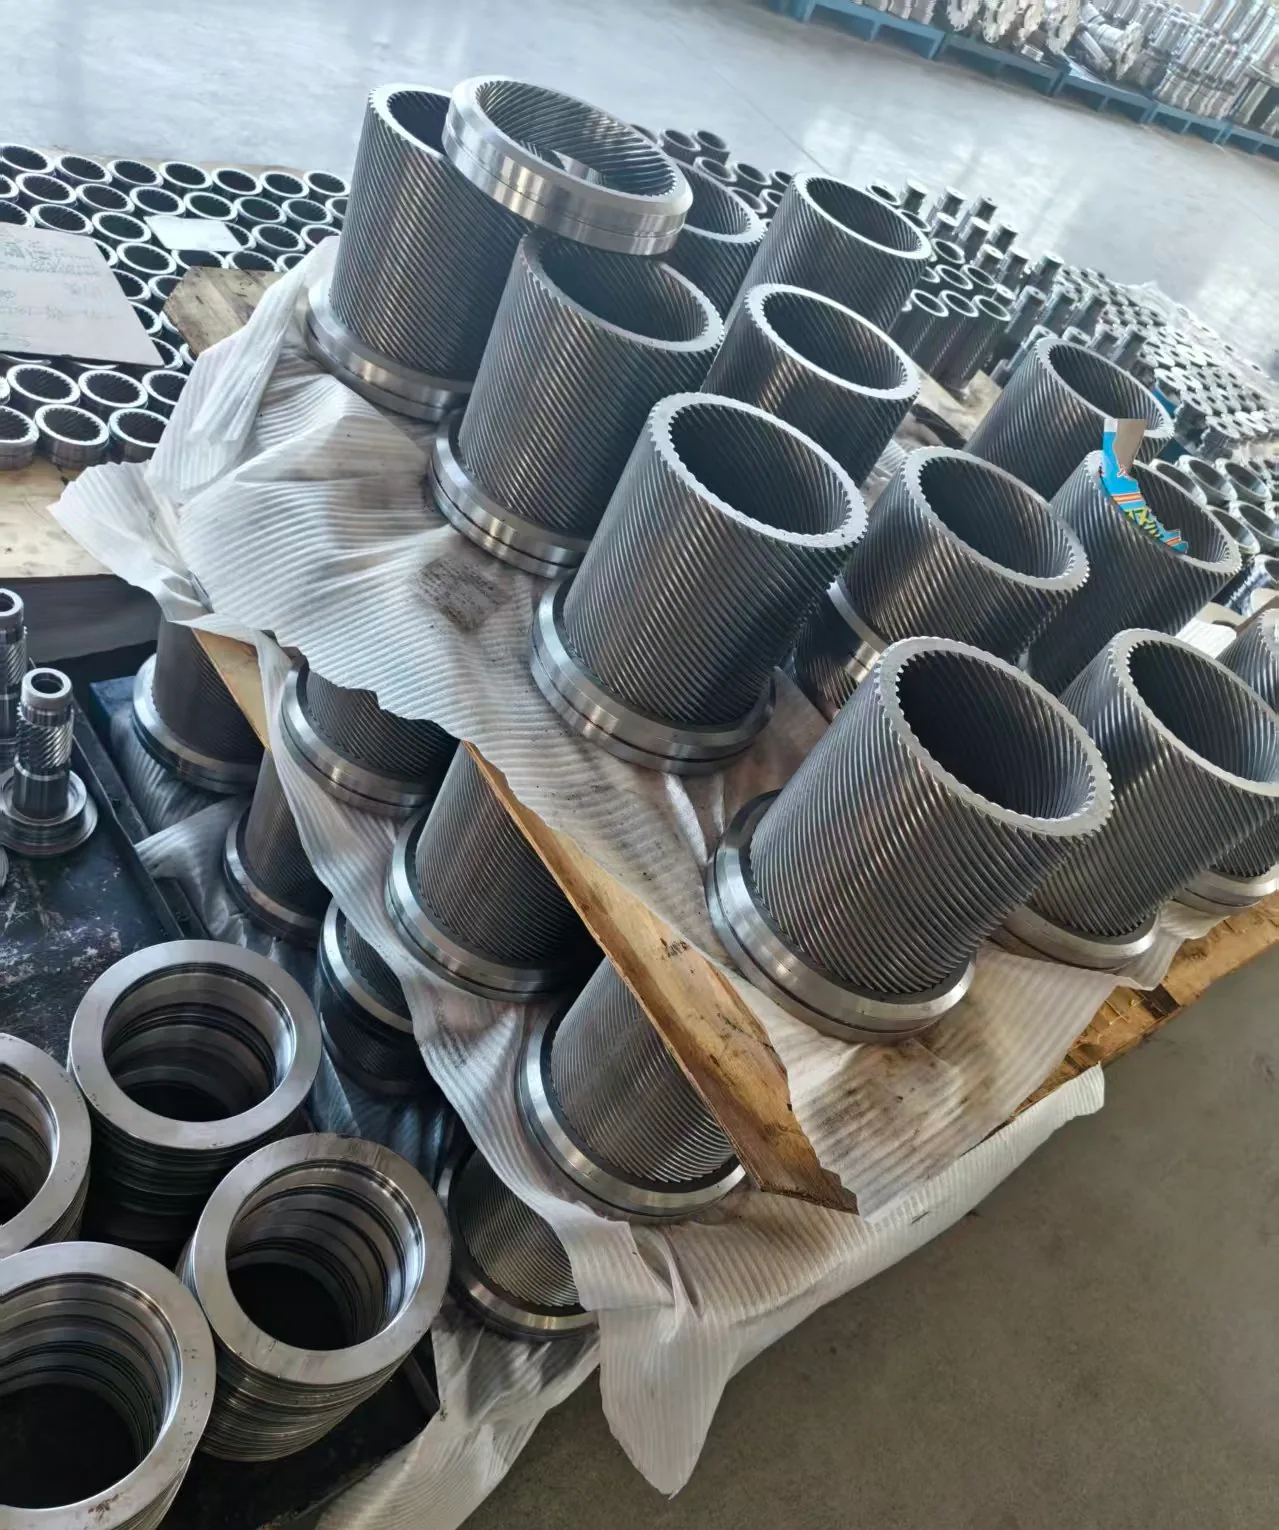
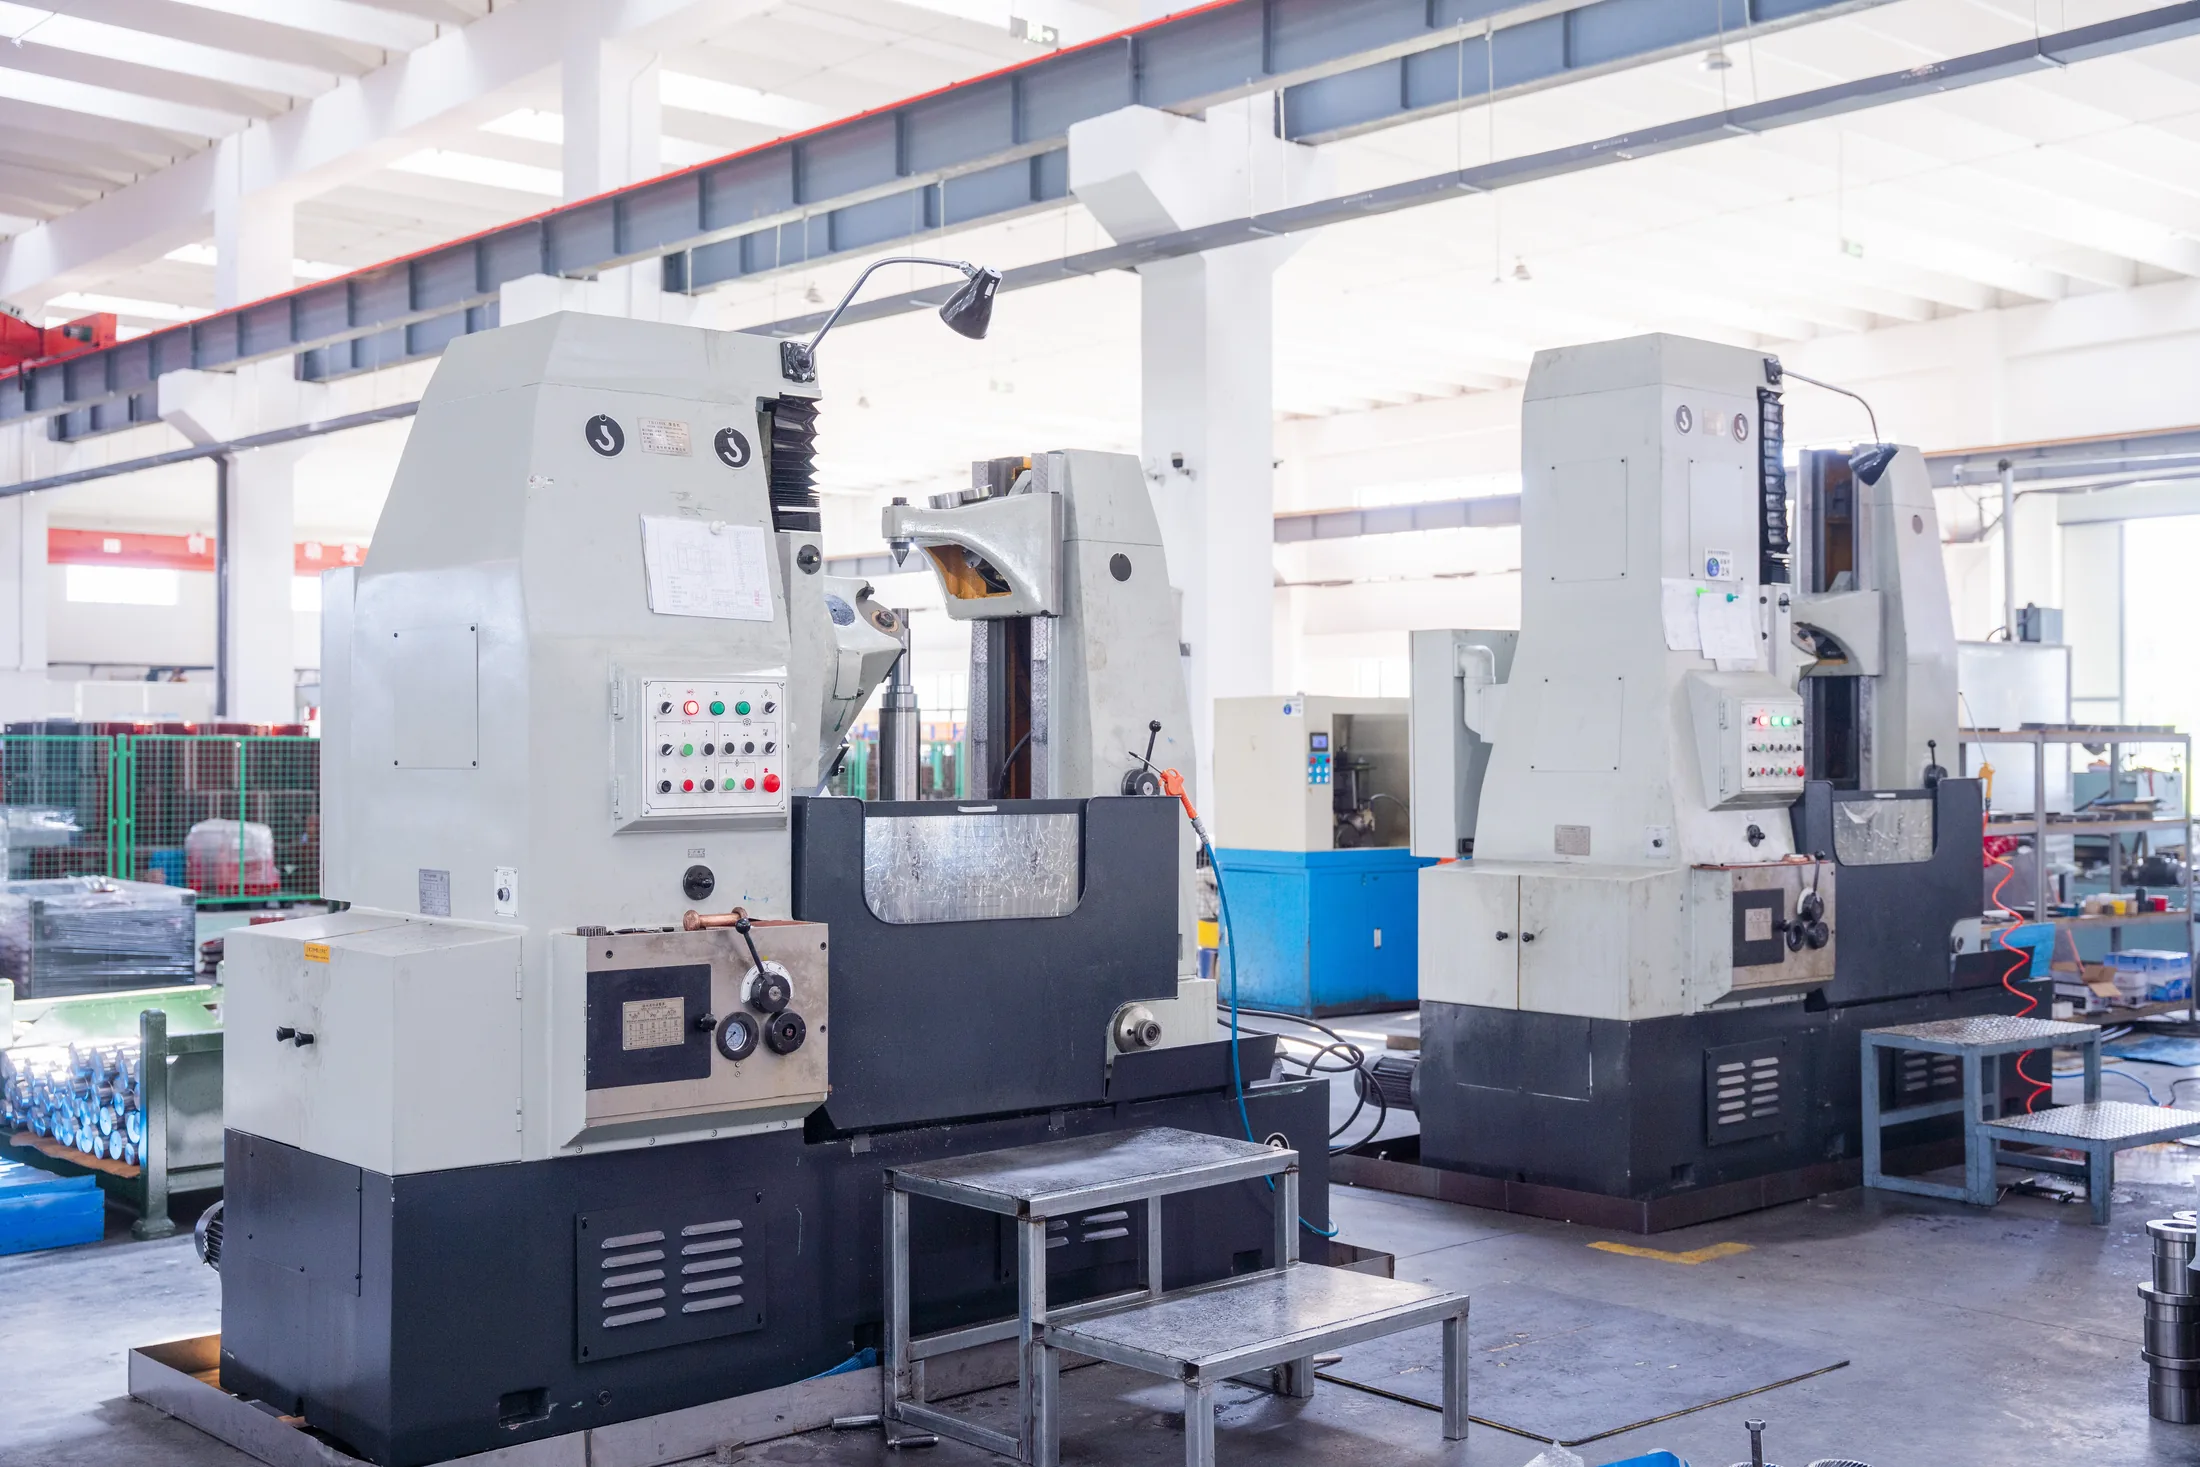
Helical spline manufacturing
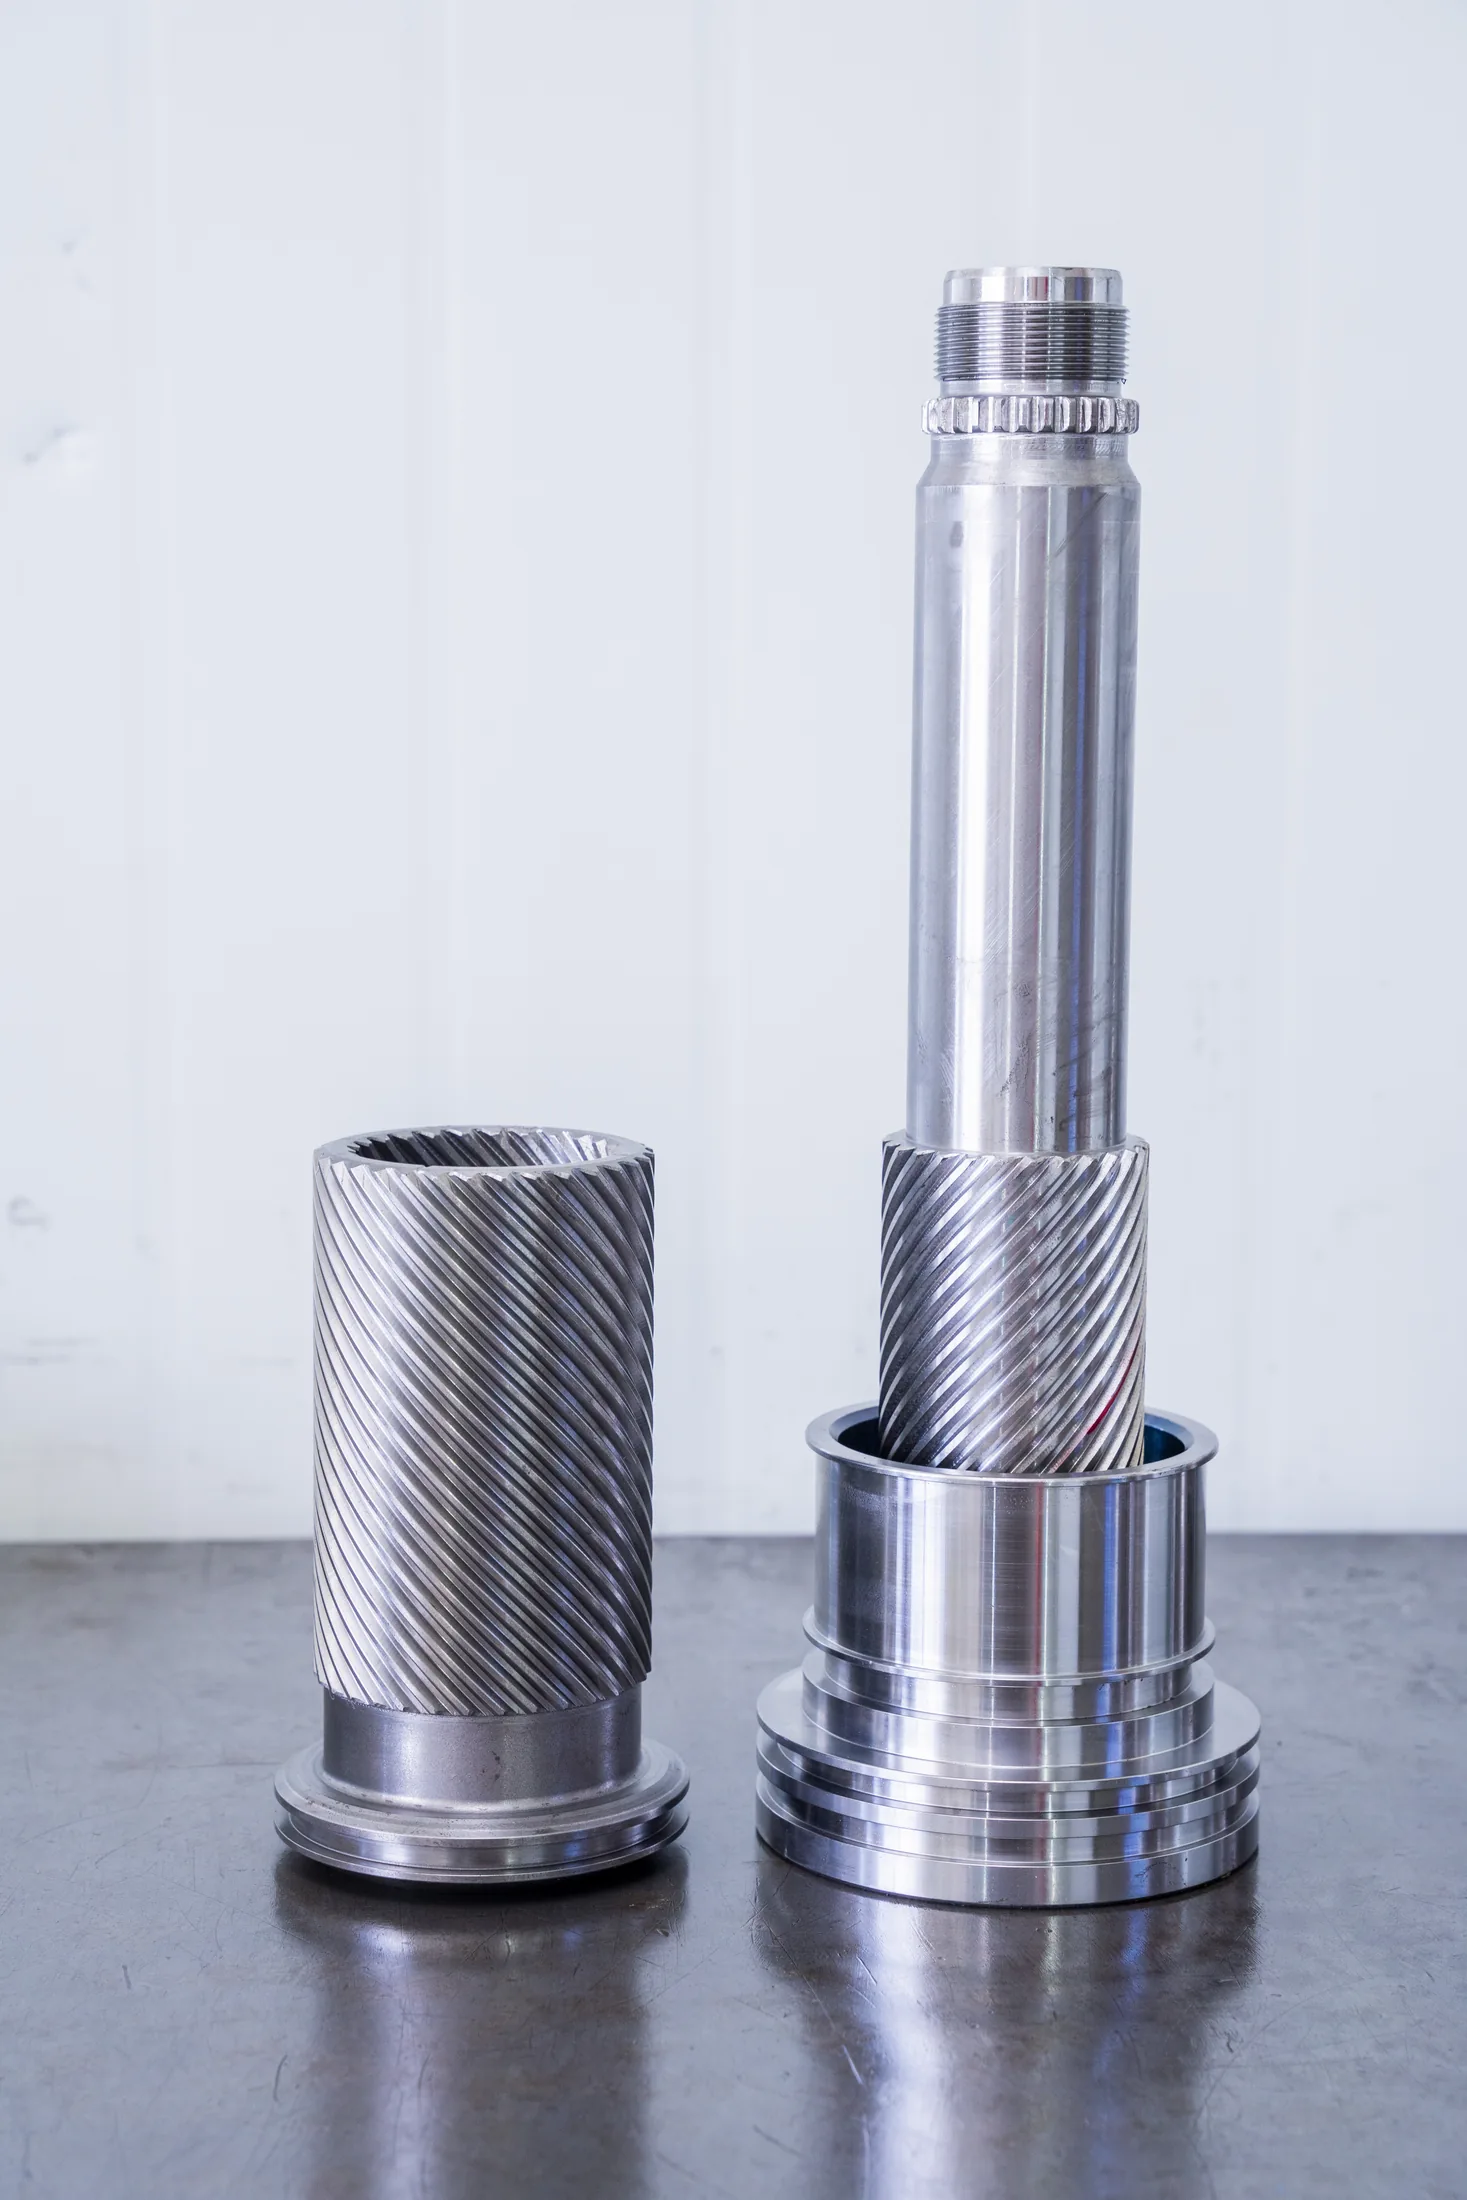
Whirling-milling cuts the multi-start helical spline in one clamping — this is the process most competitors outsource, and the reason our spline sets stay matched from blank to assembly.
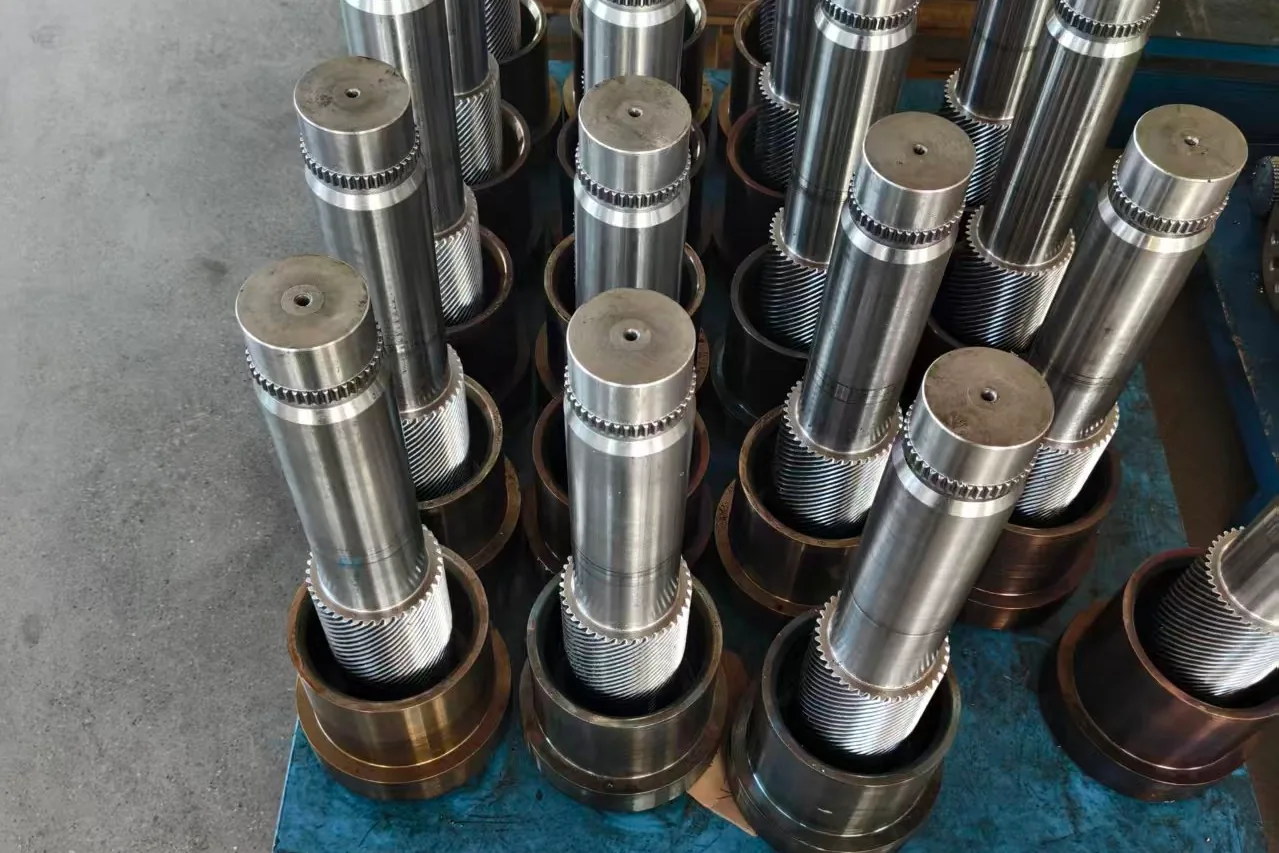
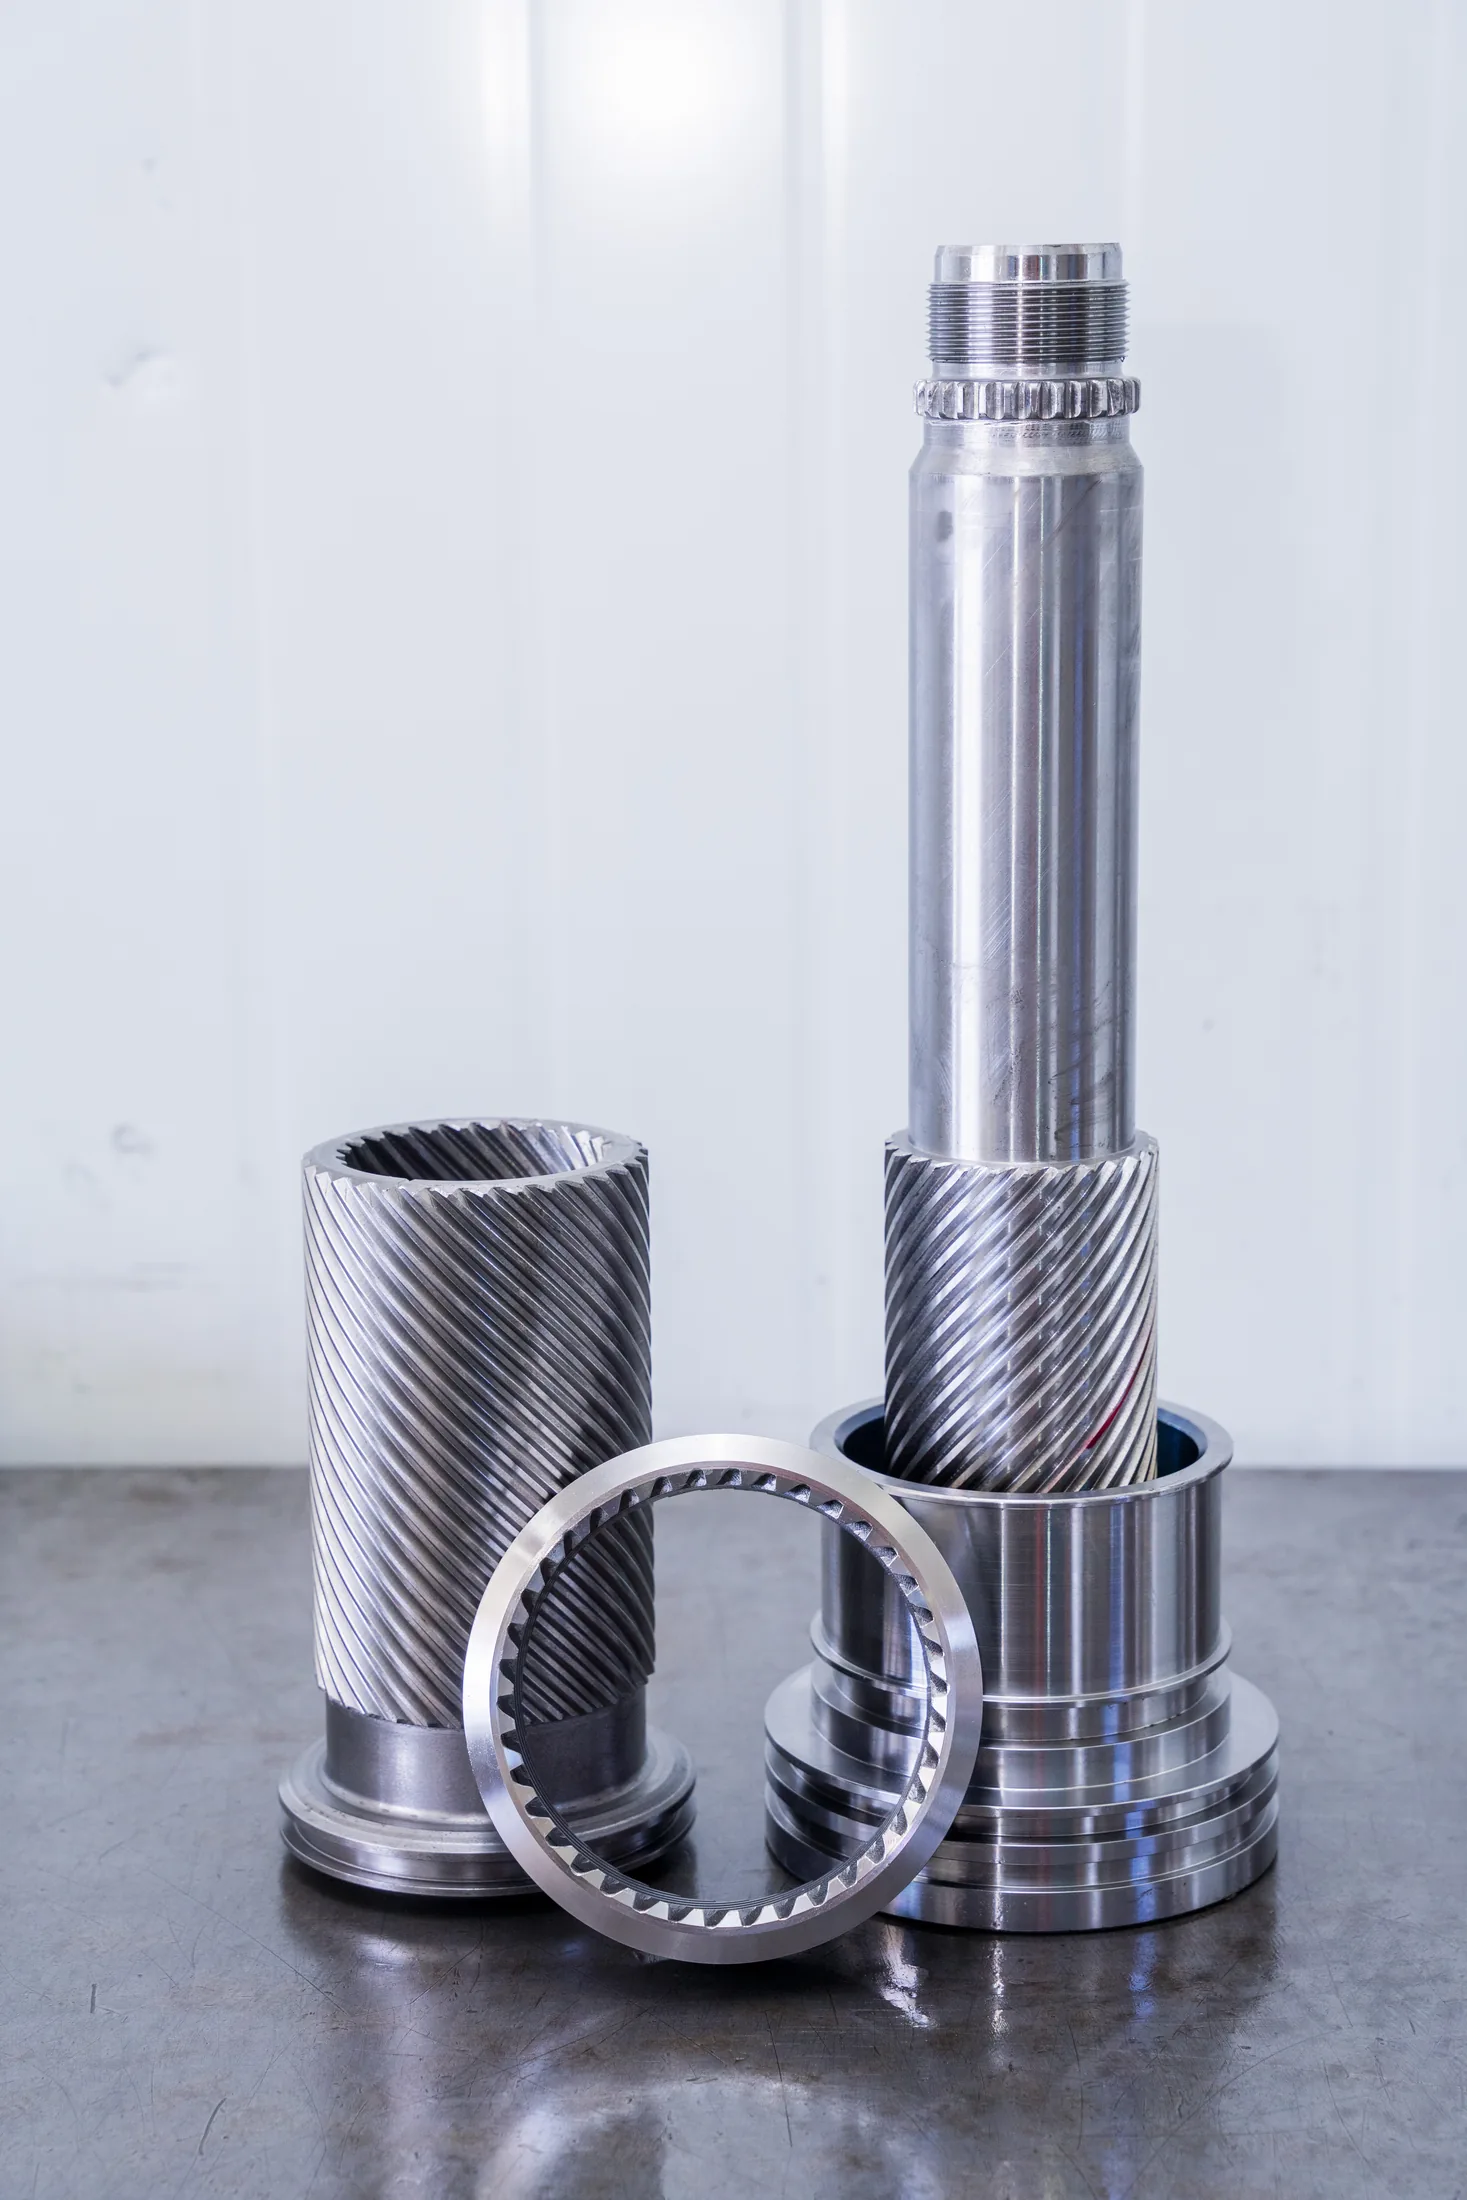
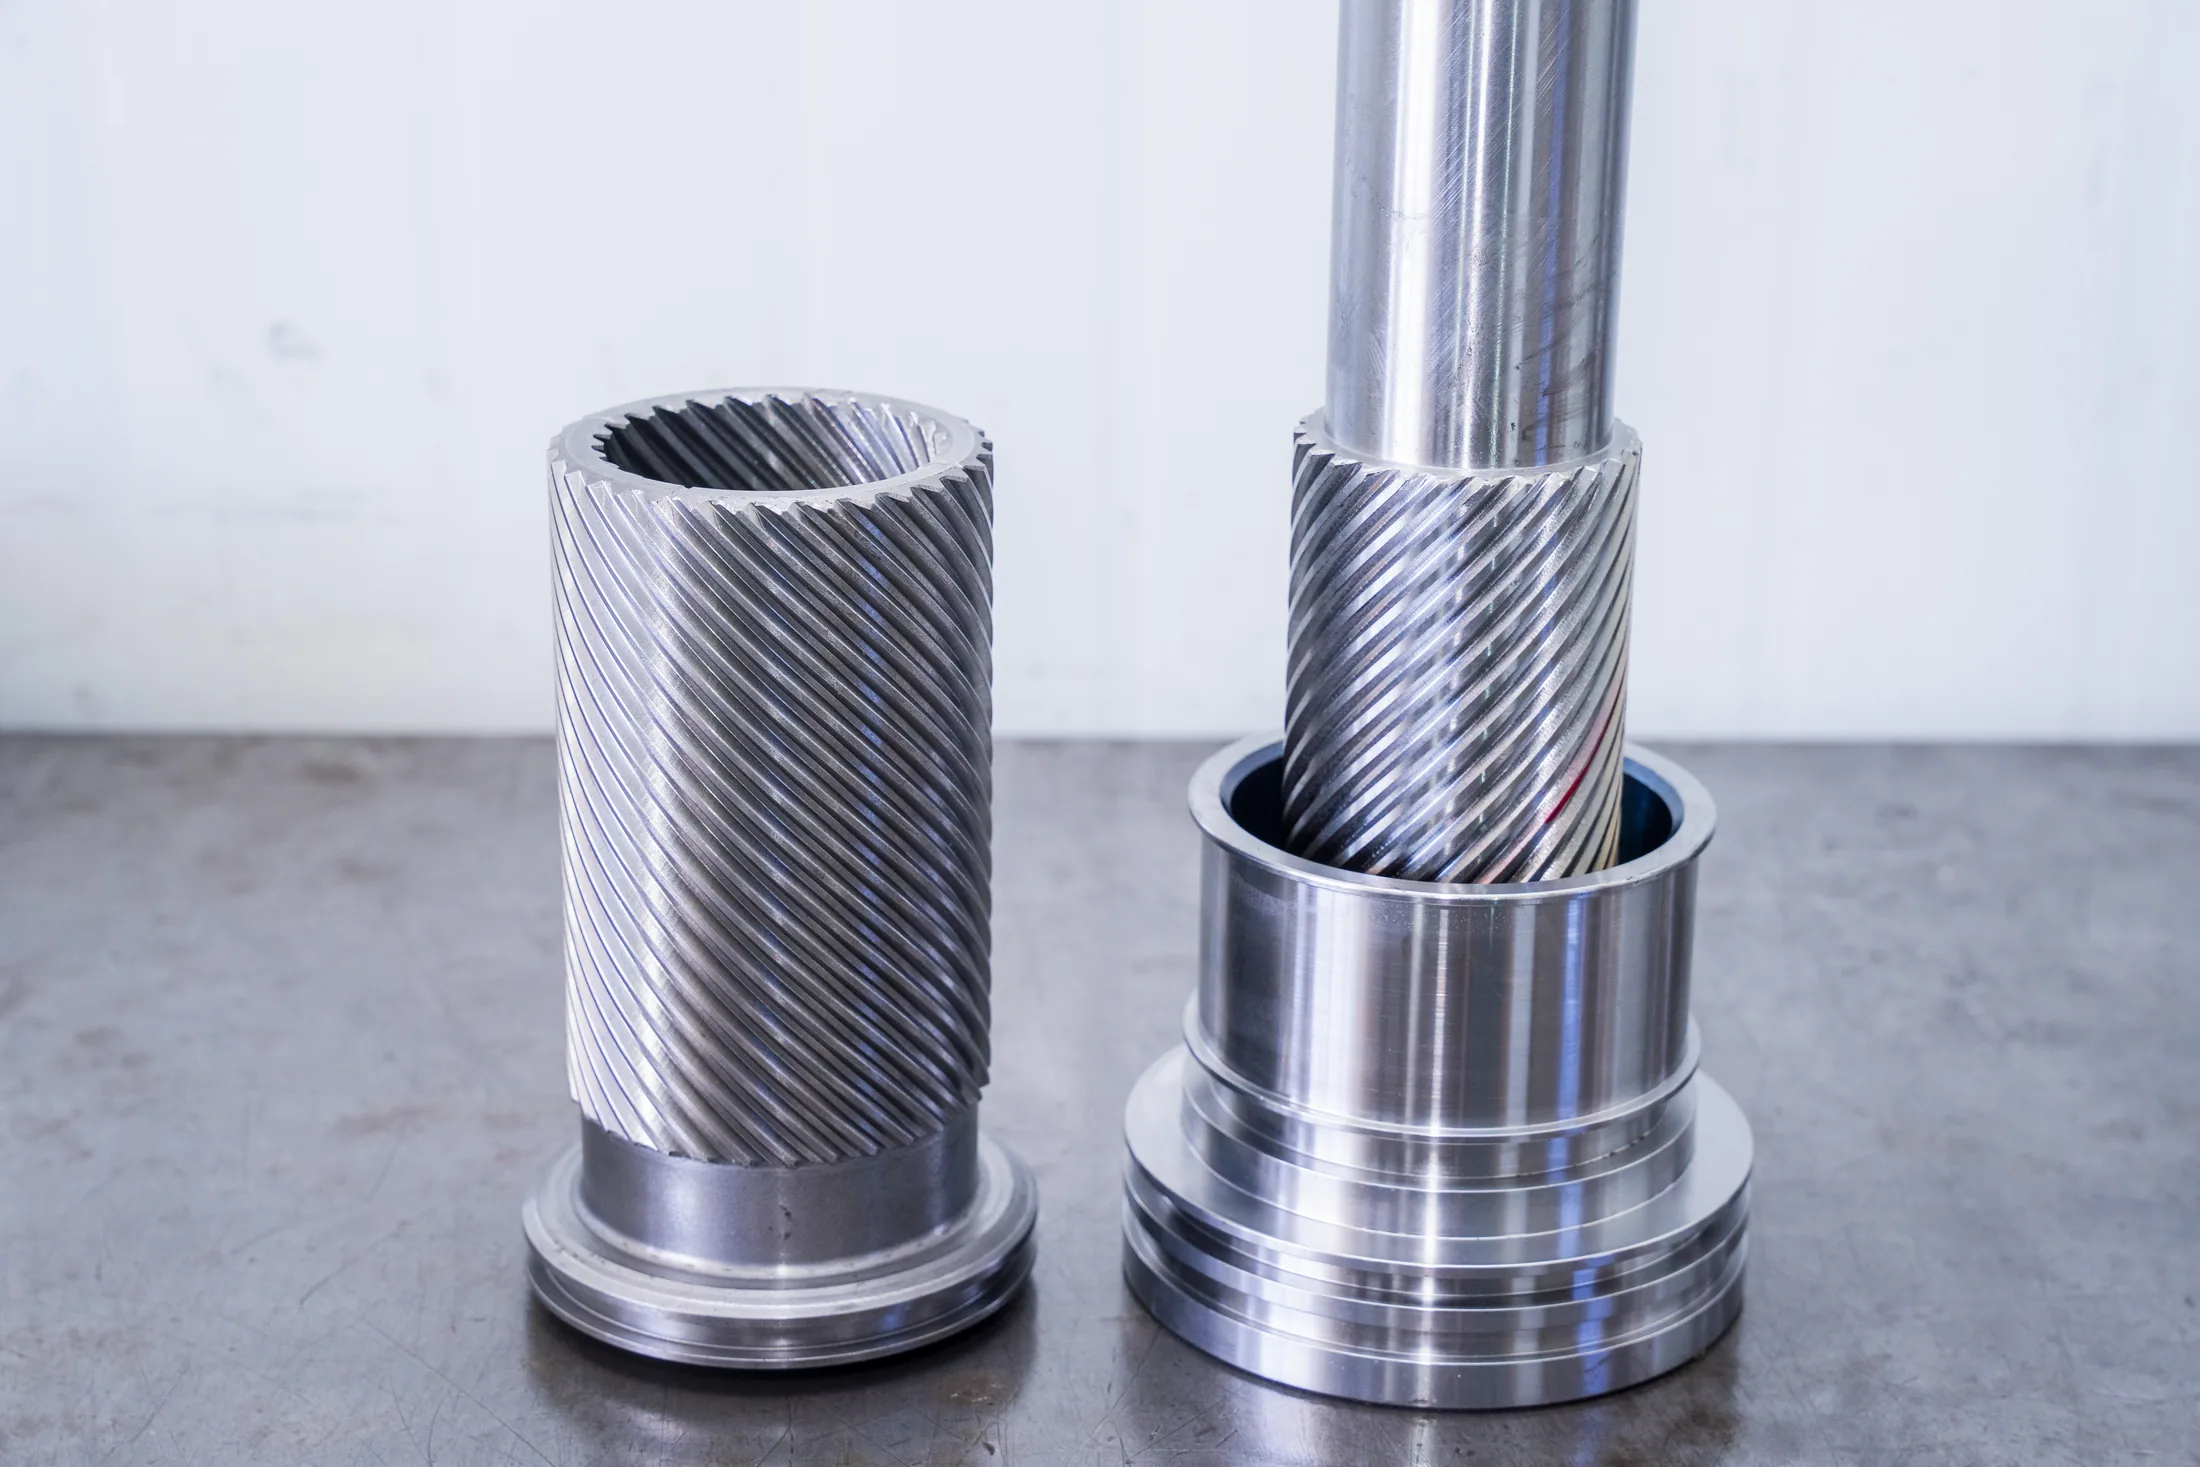
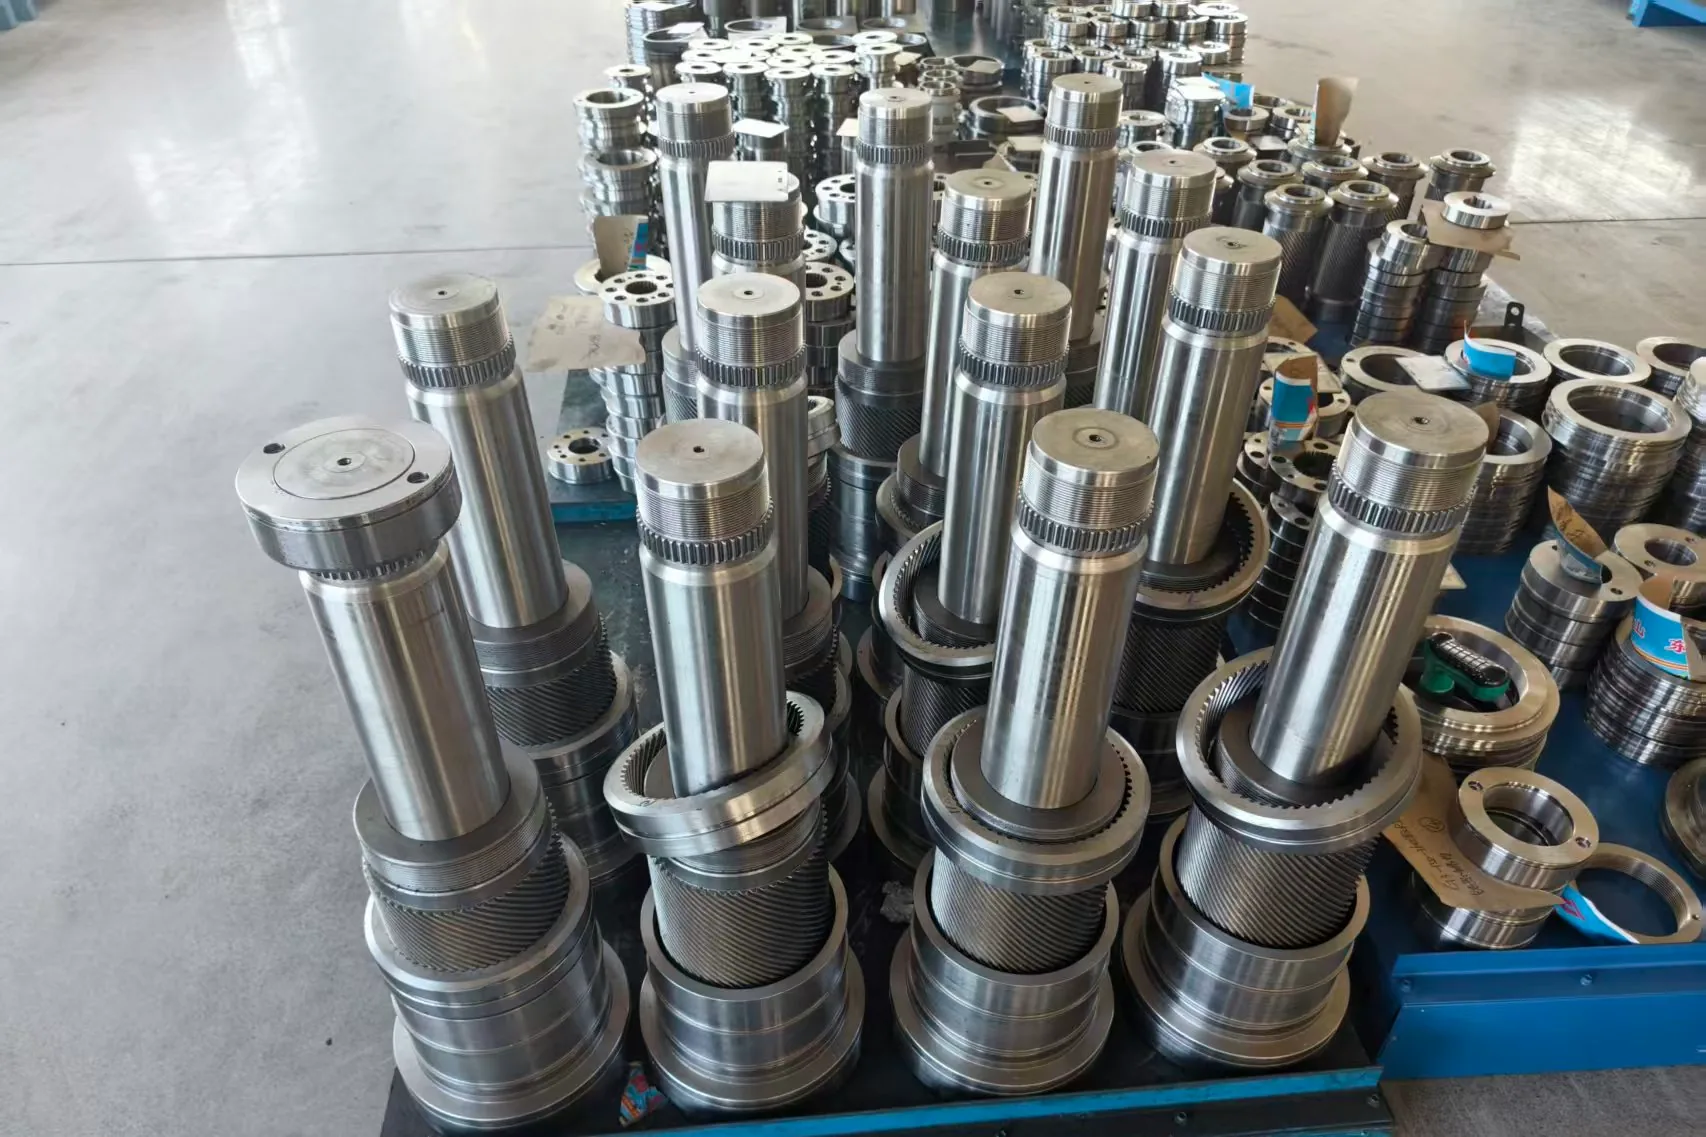
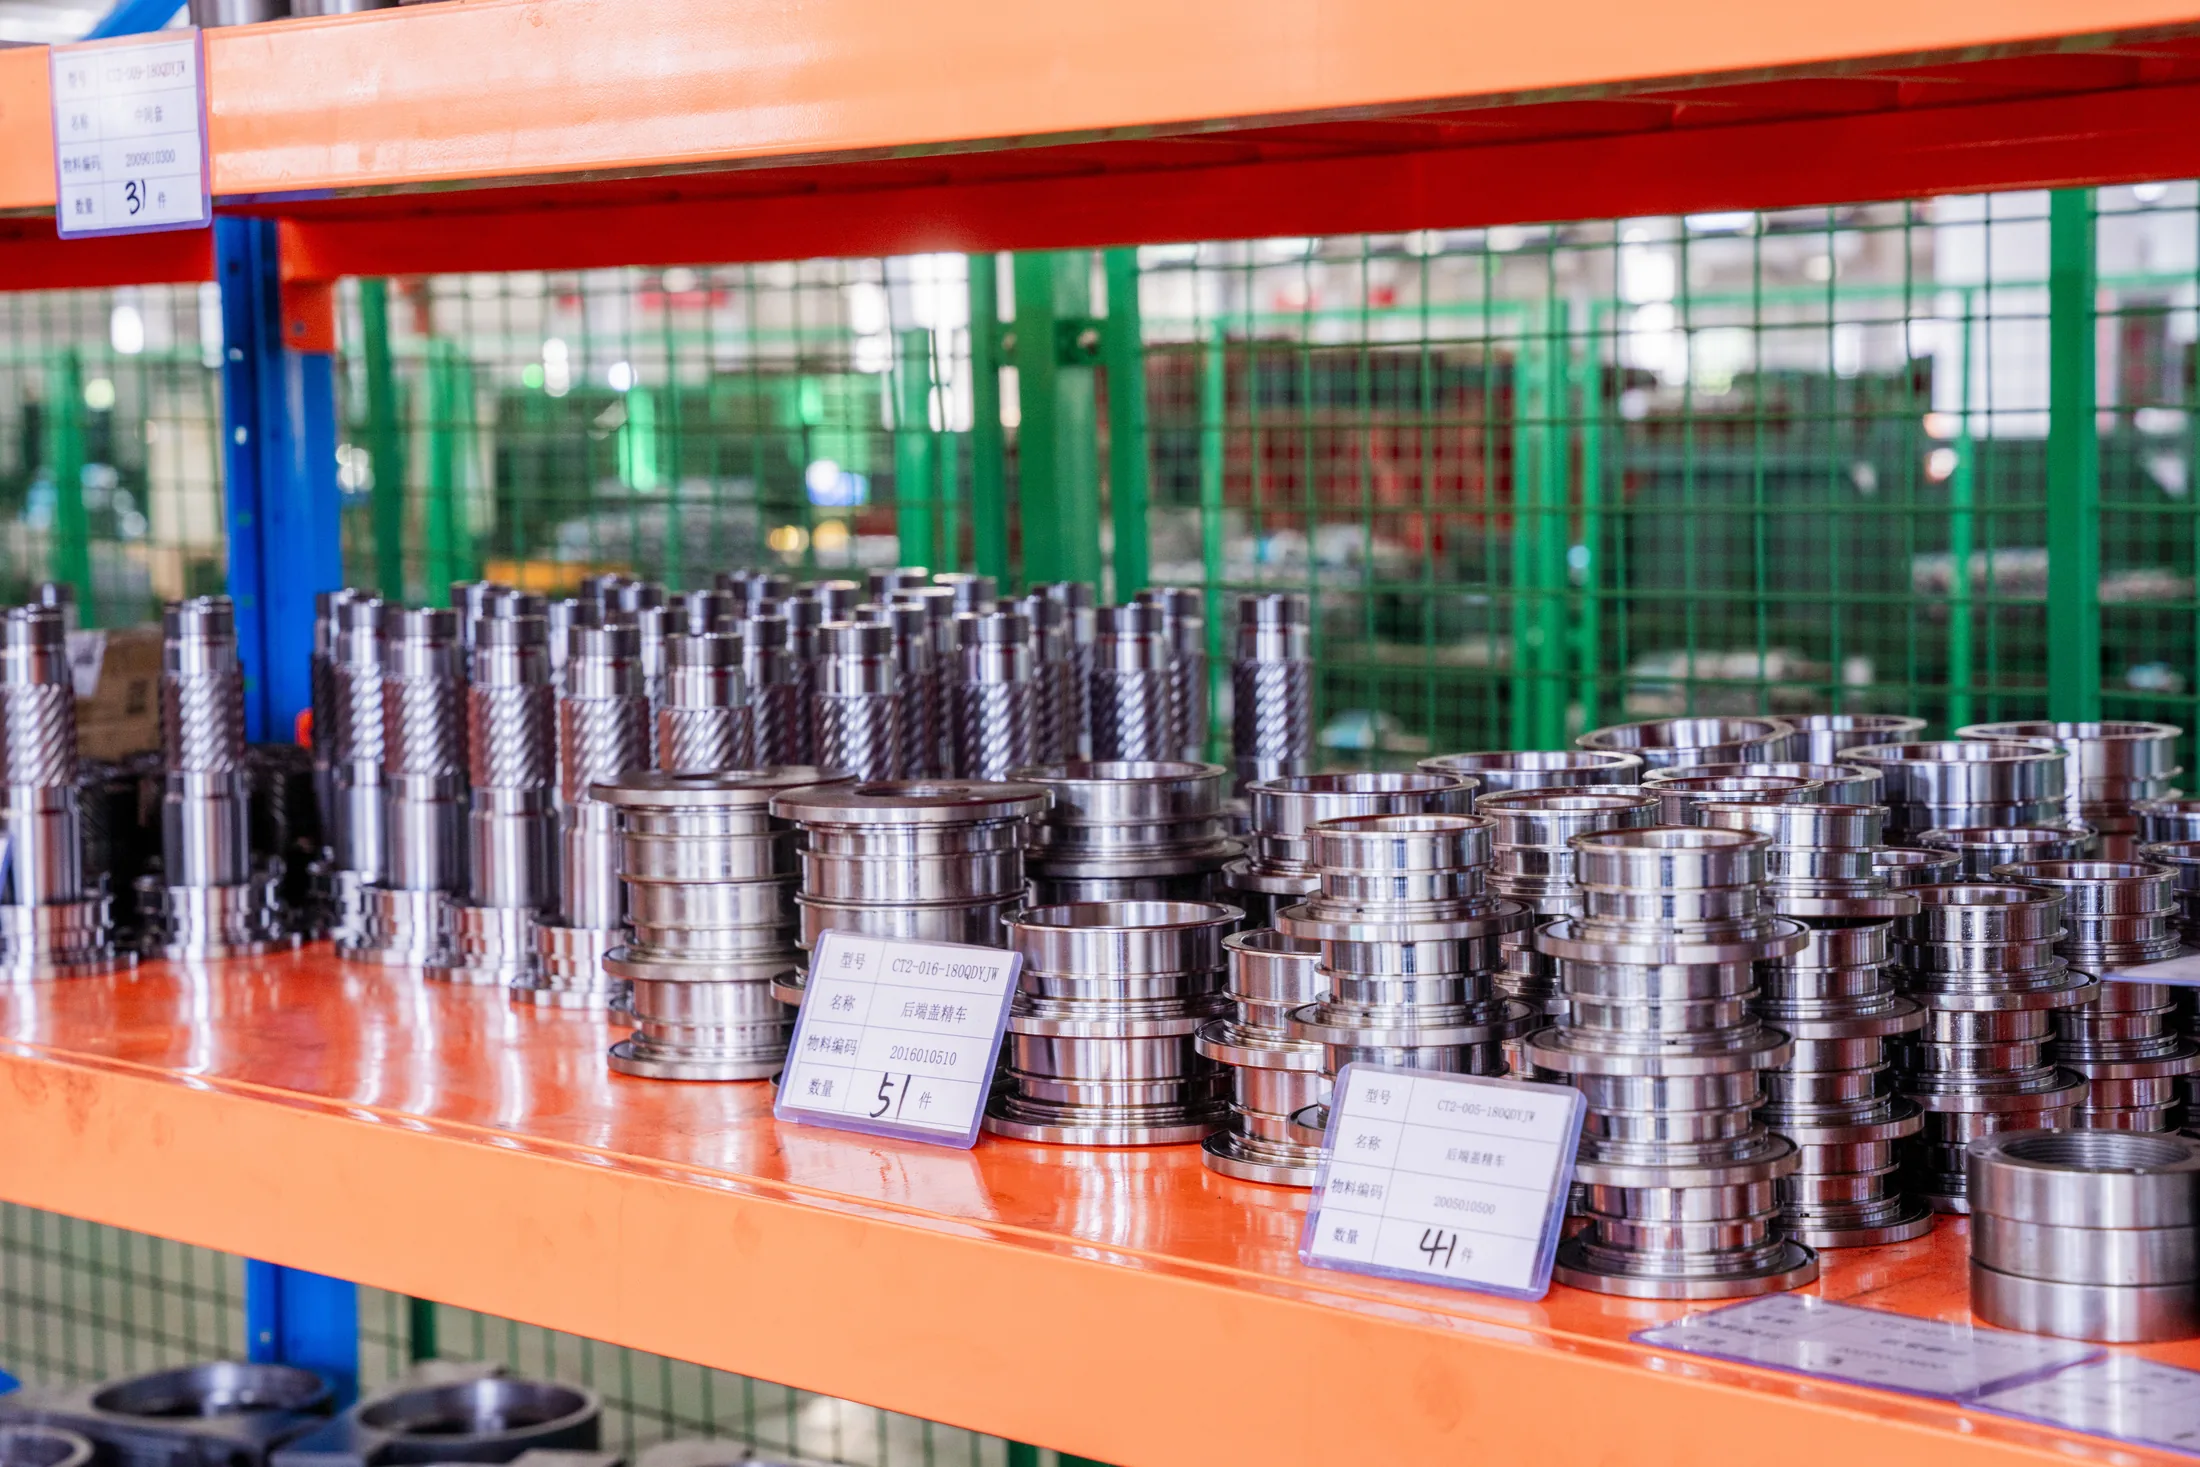
The helical spline set
Output shaft, piston and ring gear — the three parts that decide an actuator's life. Finish-ground here, batch-labelled and batch-traceable.
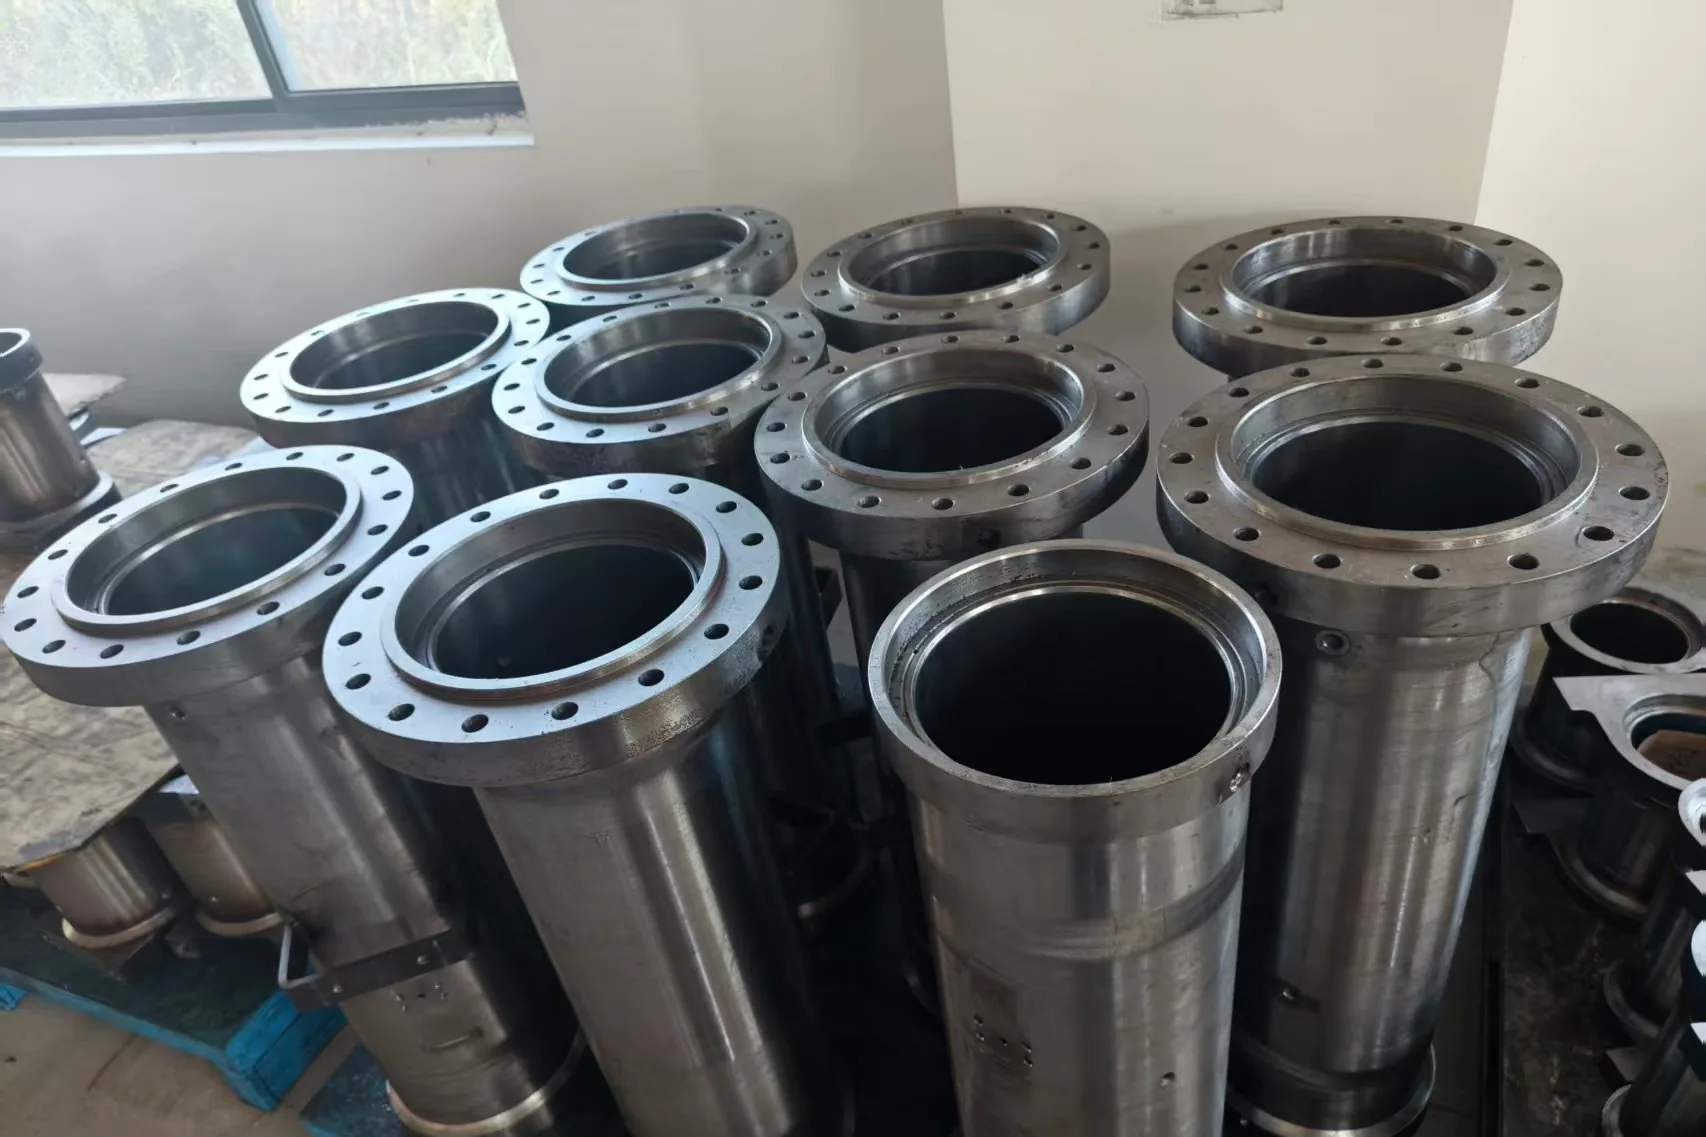
Housings, end caps, valve blocks
The rest of the floor
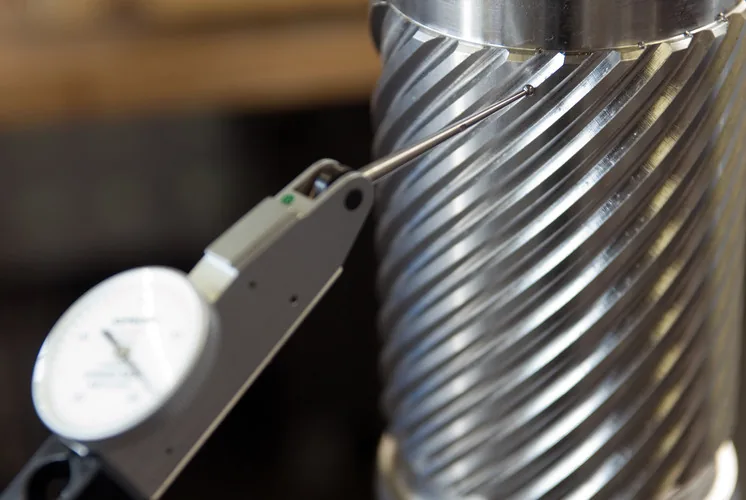
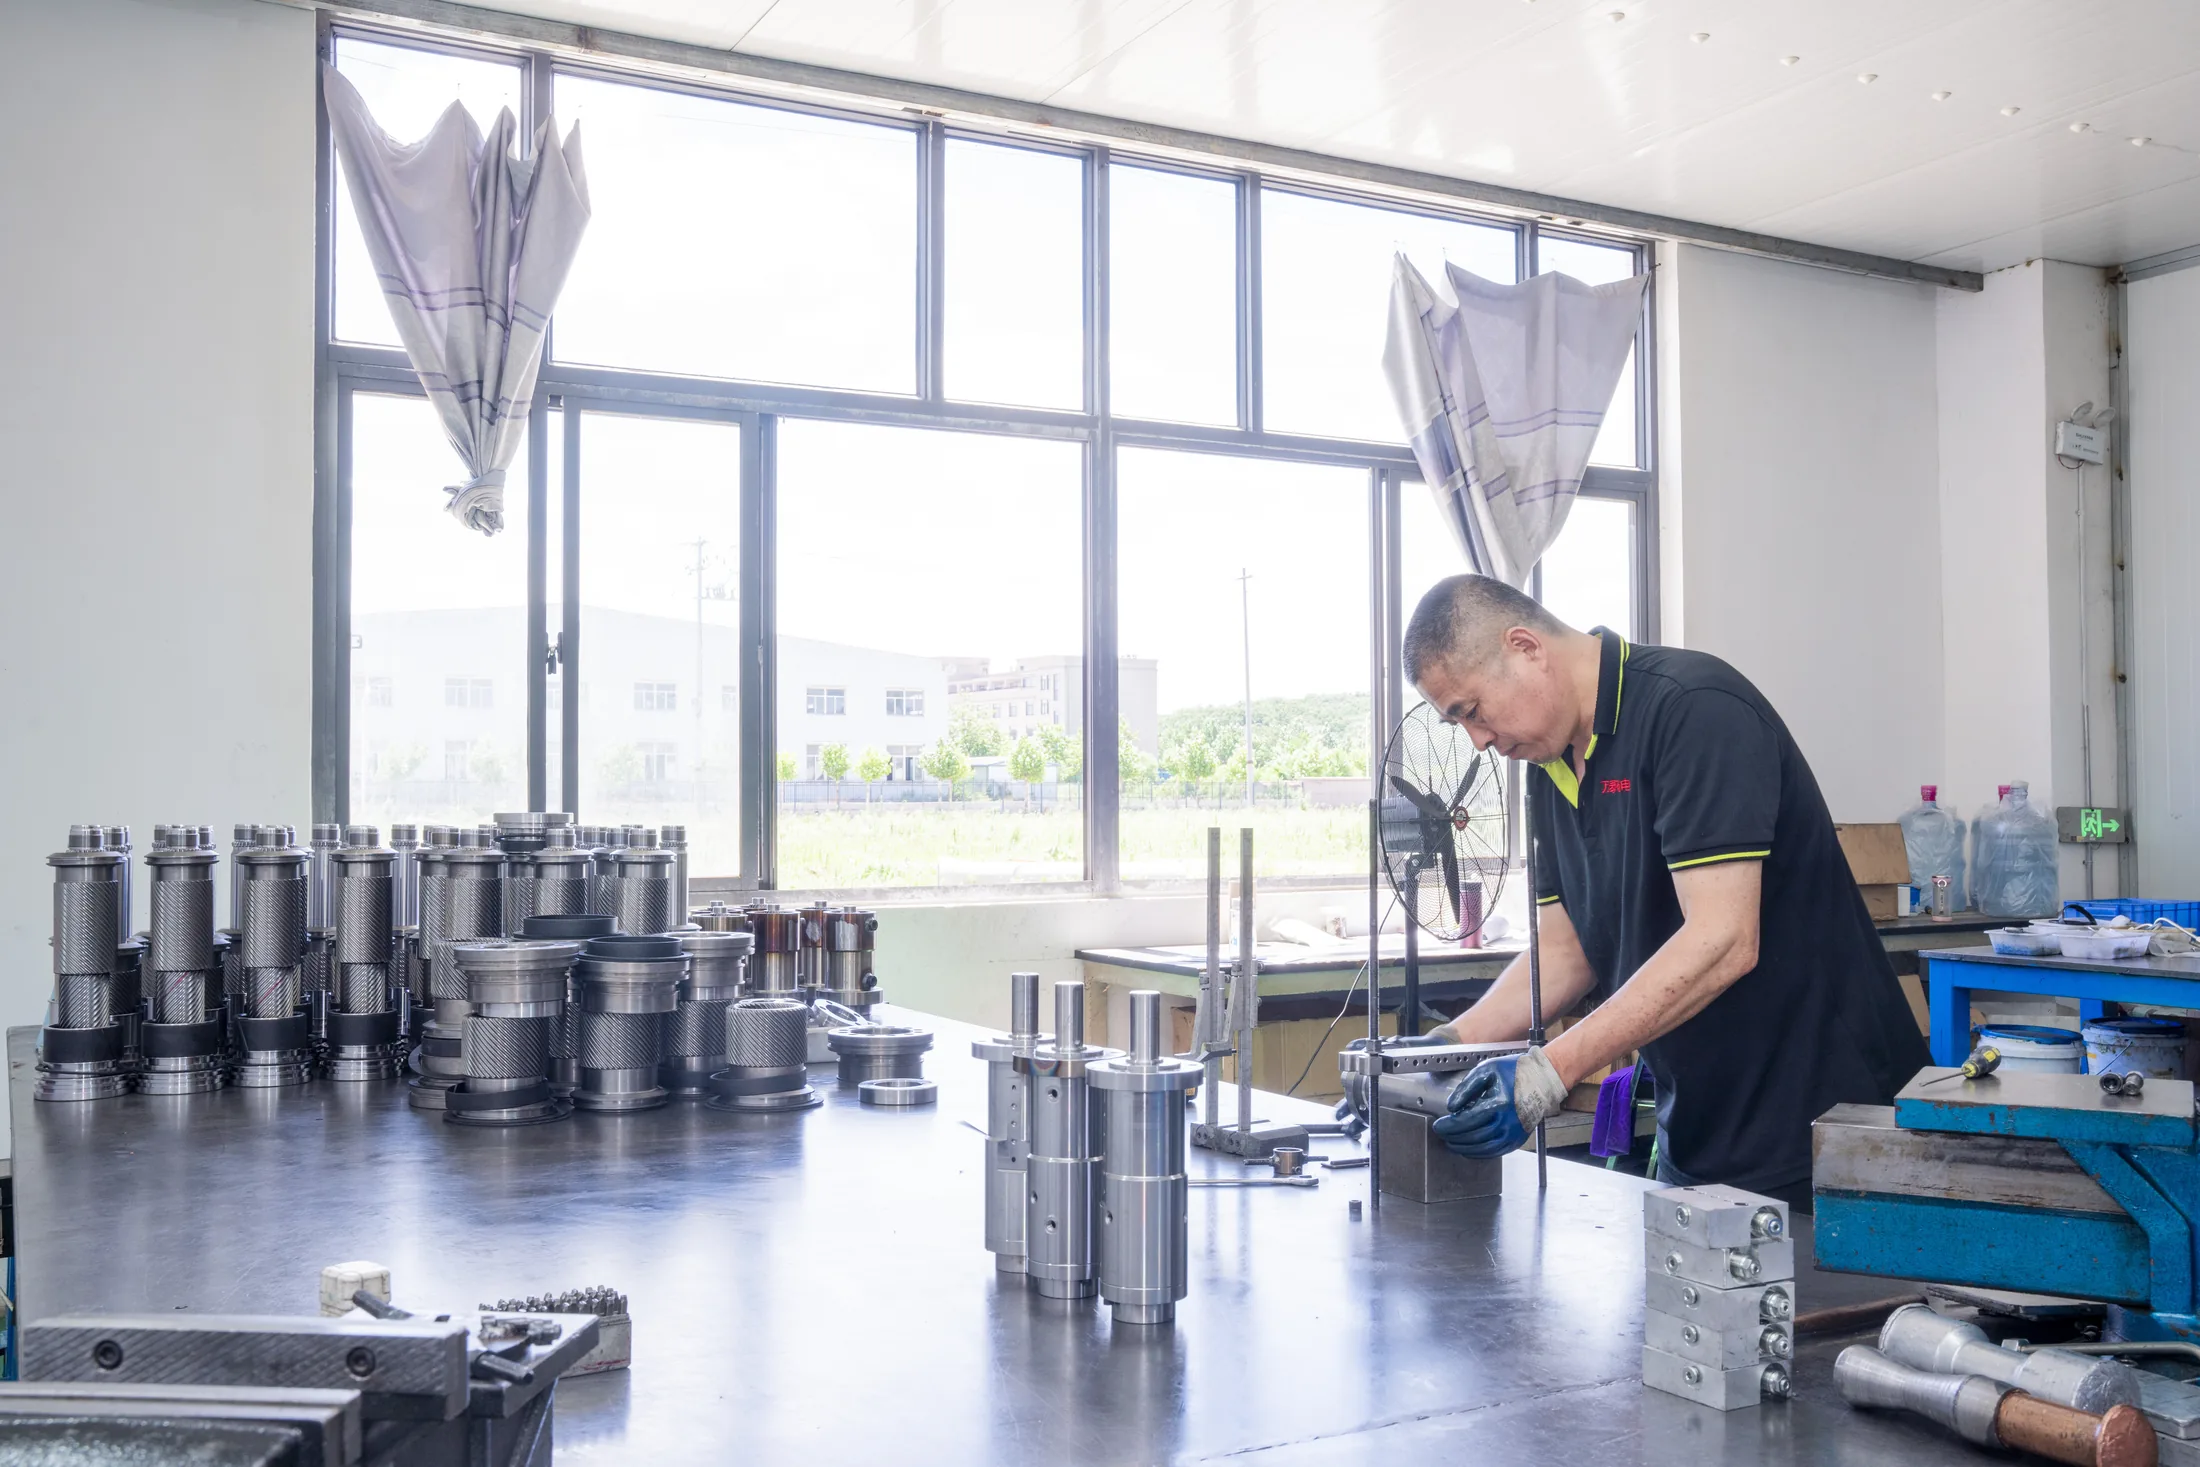
Inspection and measurement
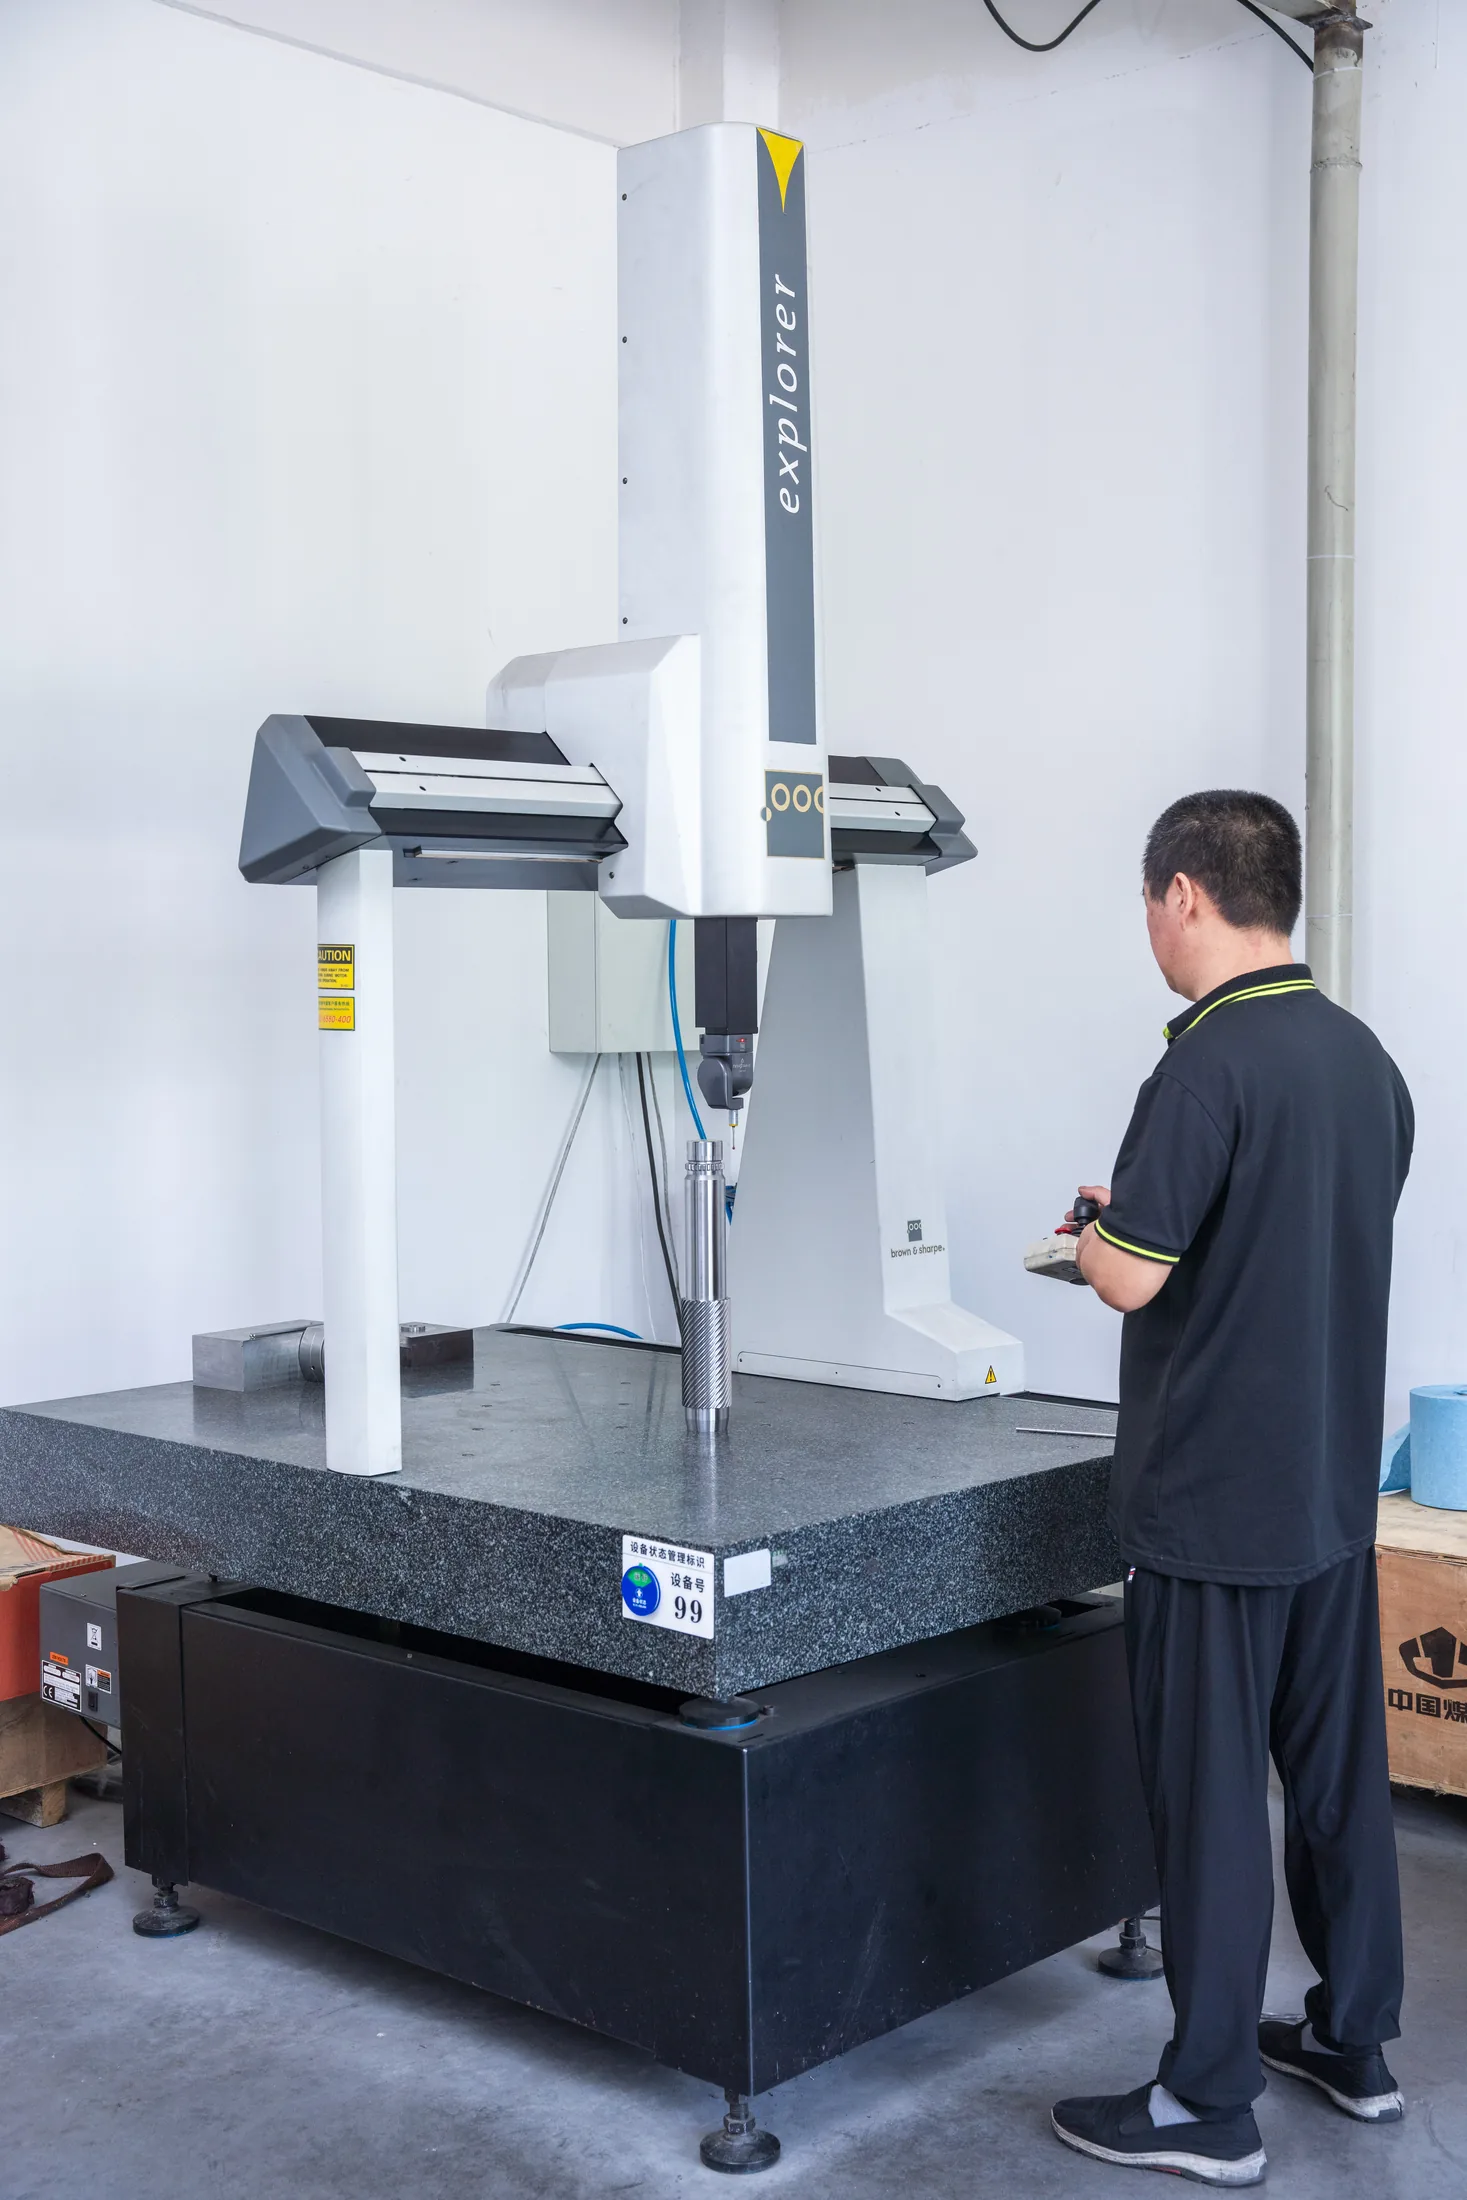
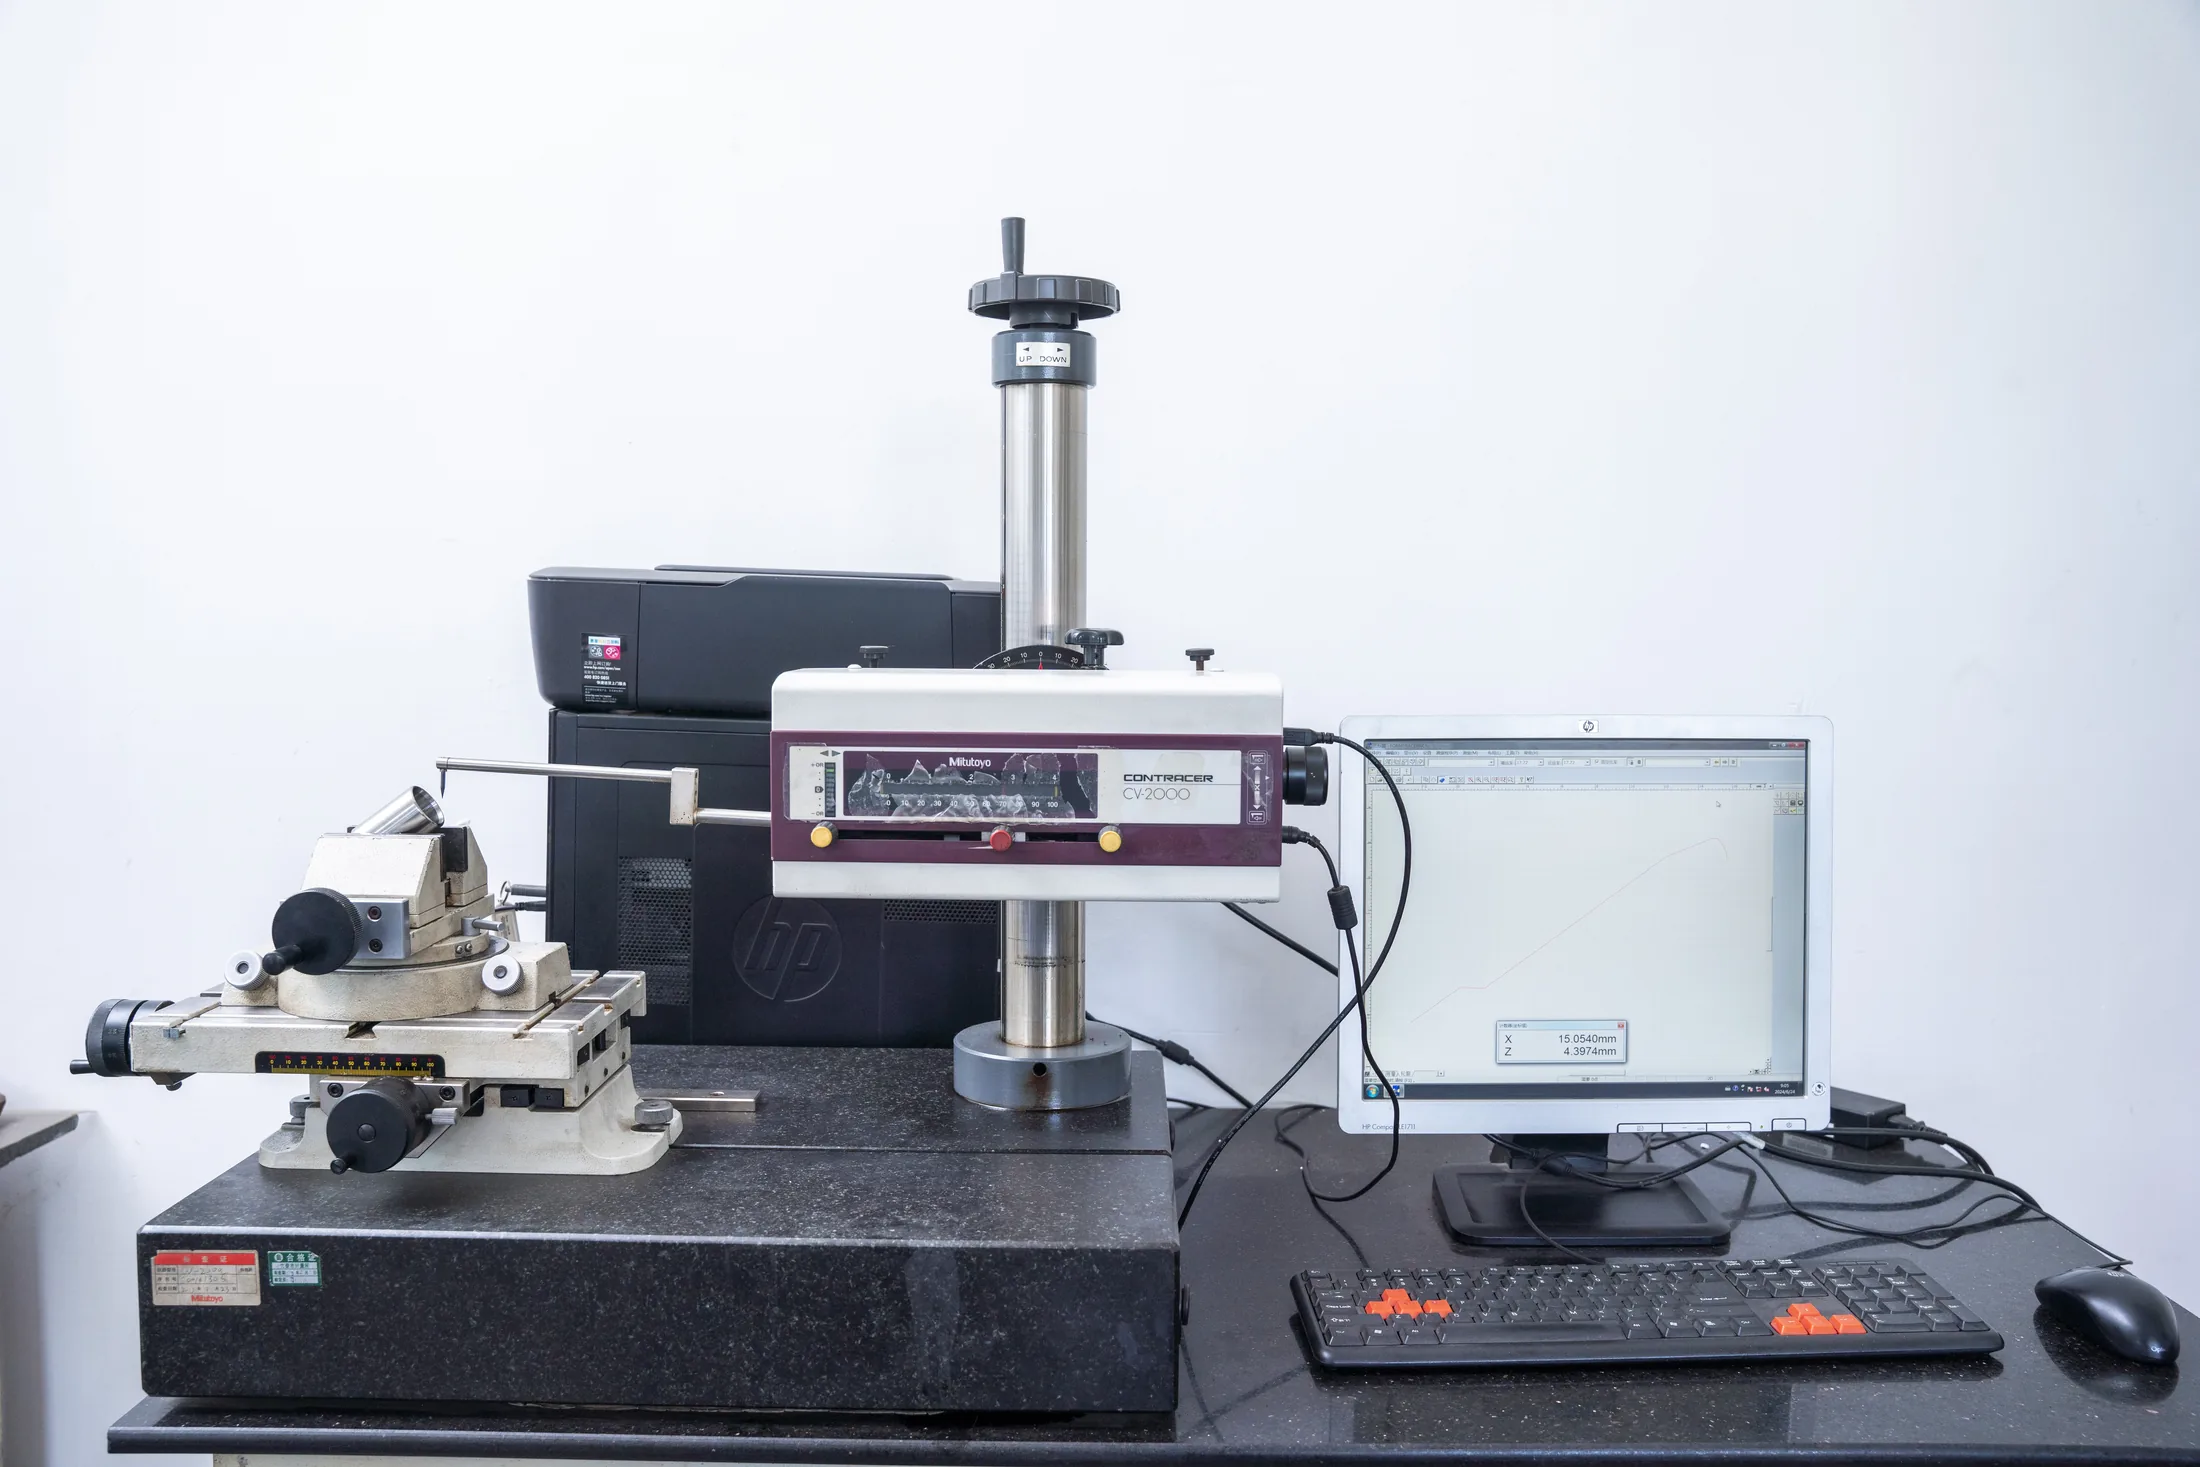
First articles, batch samples and custom prototypes are verified on the CMM and contour machine before they reach the test rig — spline profiles, flange run-out, port positions, bore sizes. Reports are supplied with every custom order.
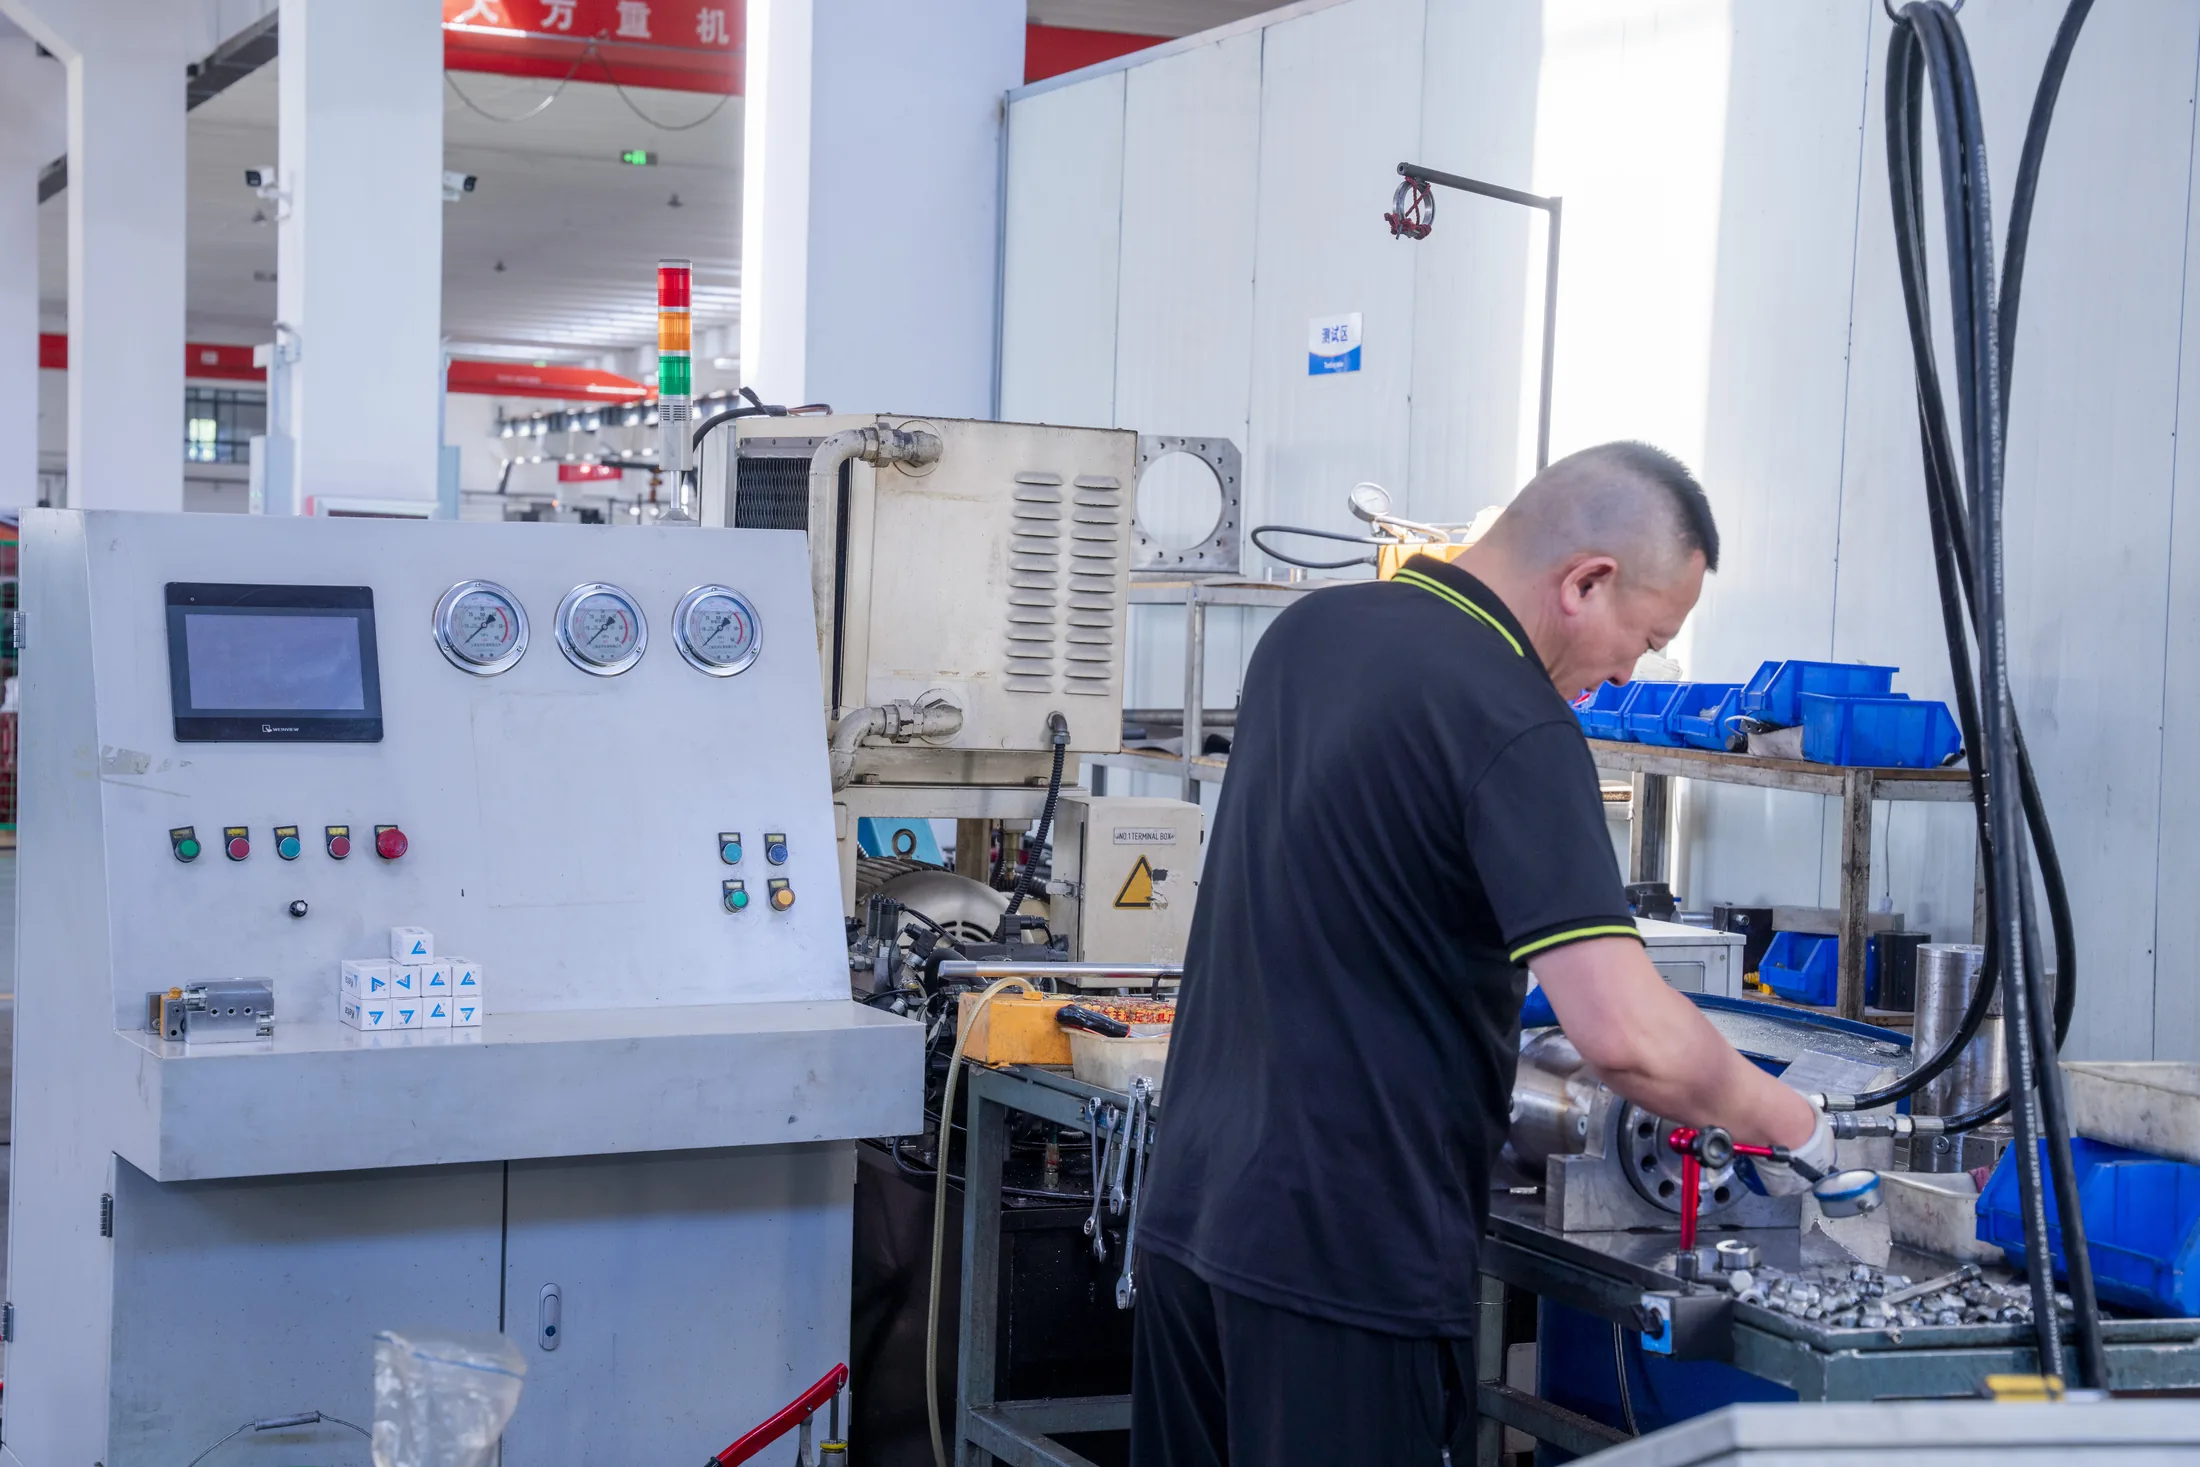
Assembly and testing
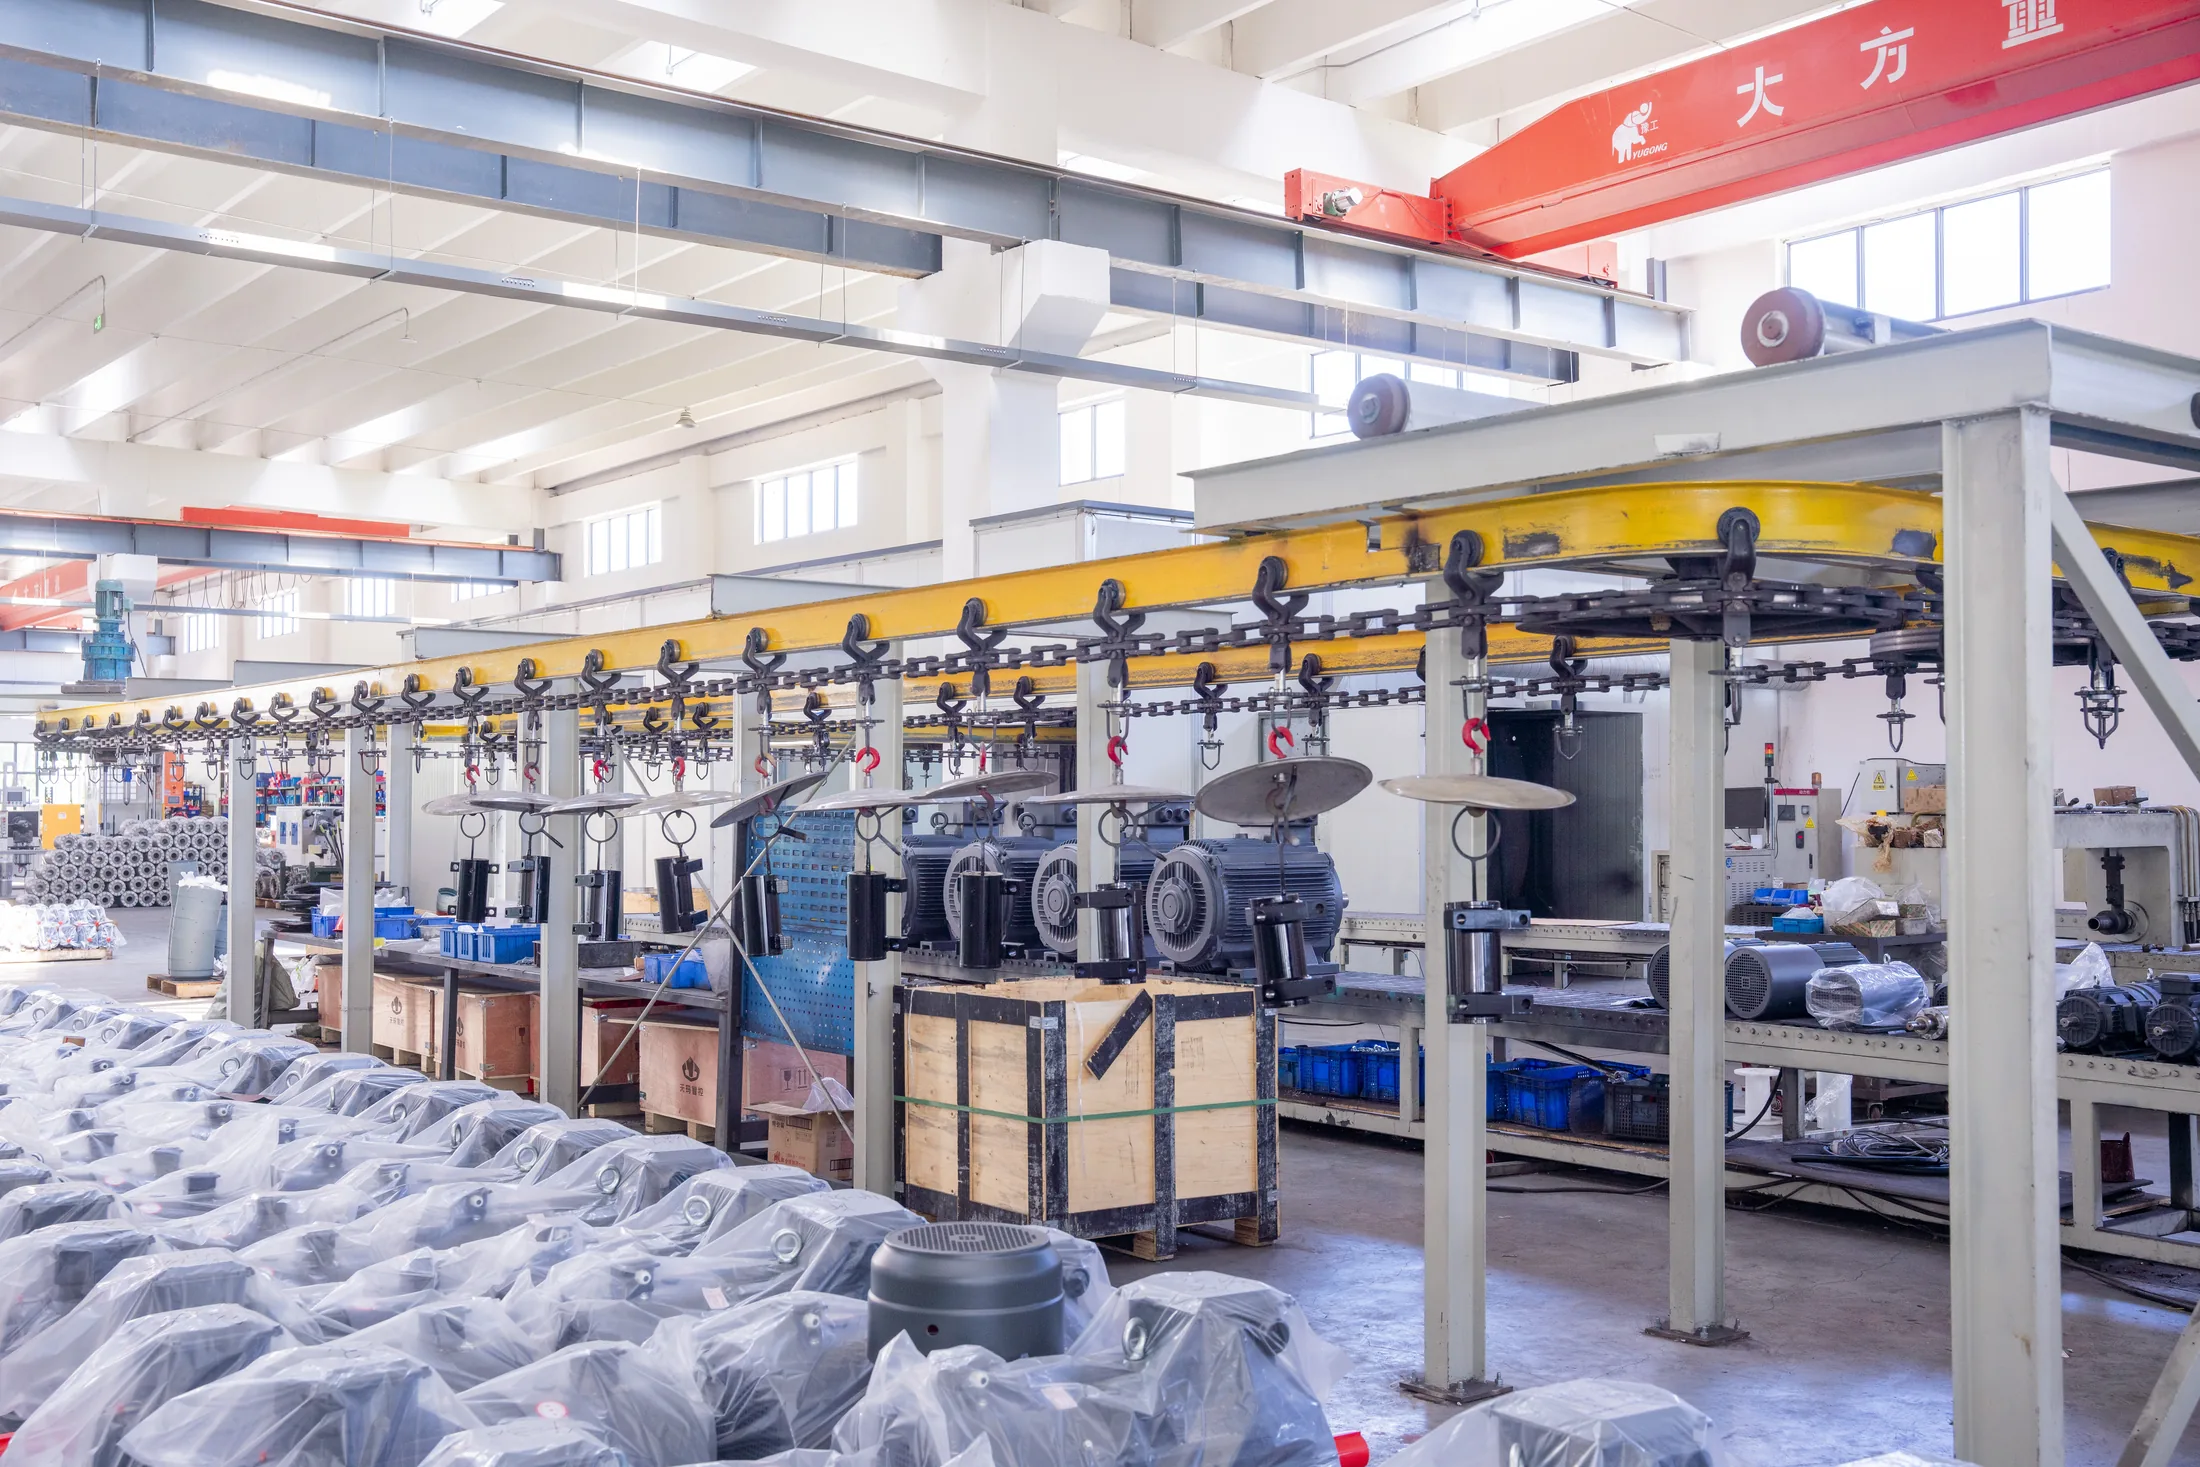
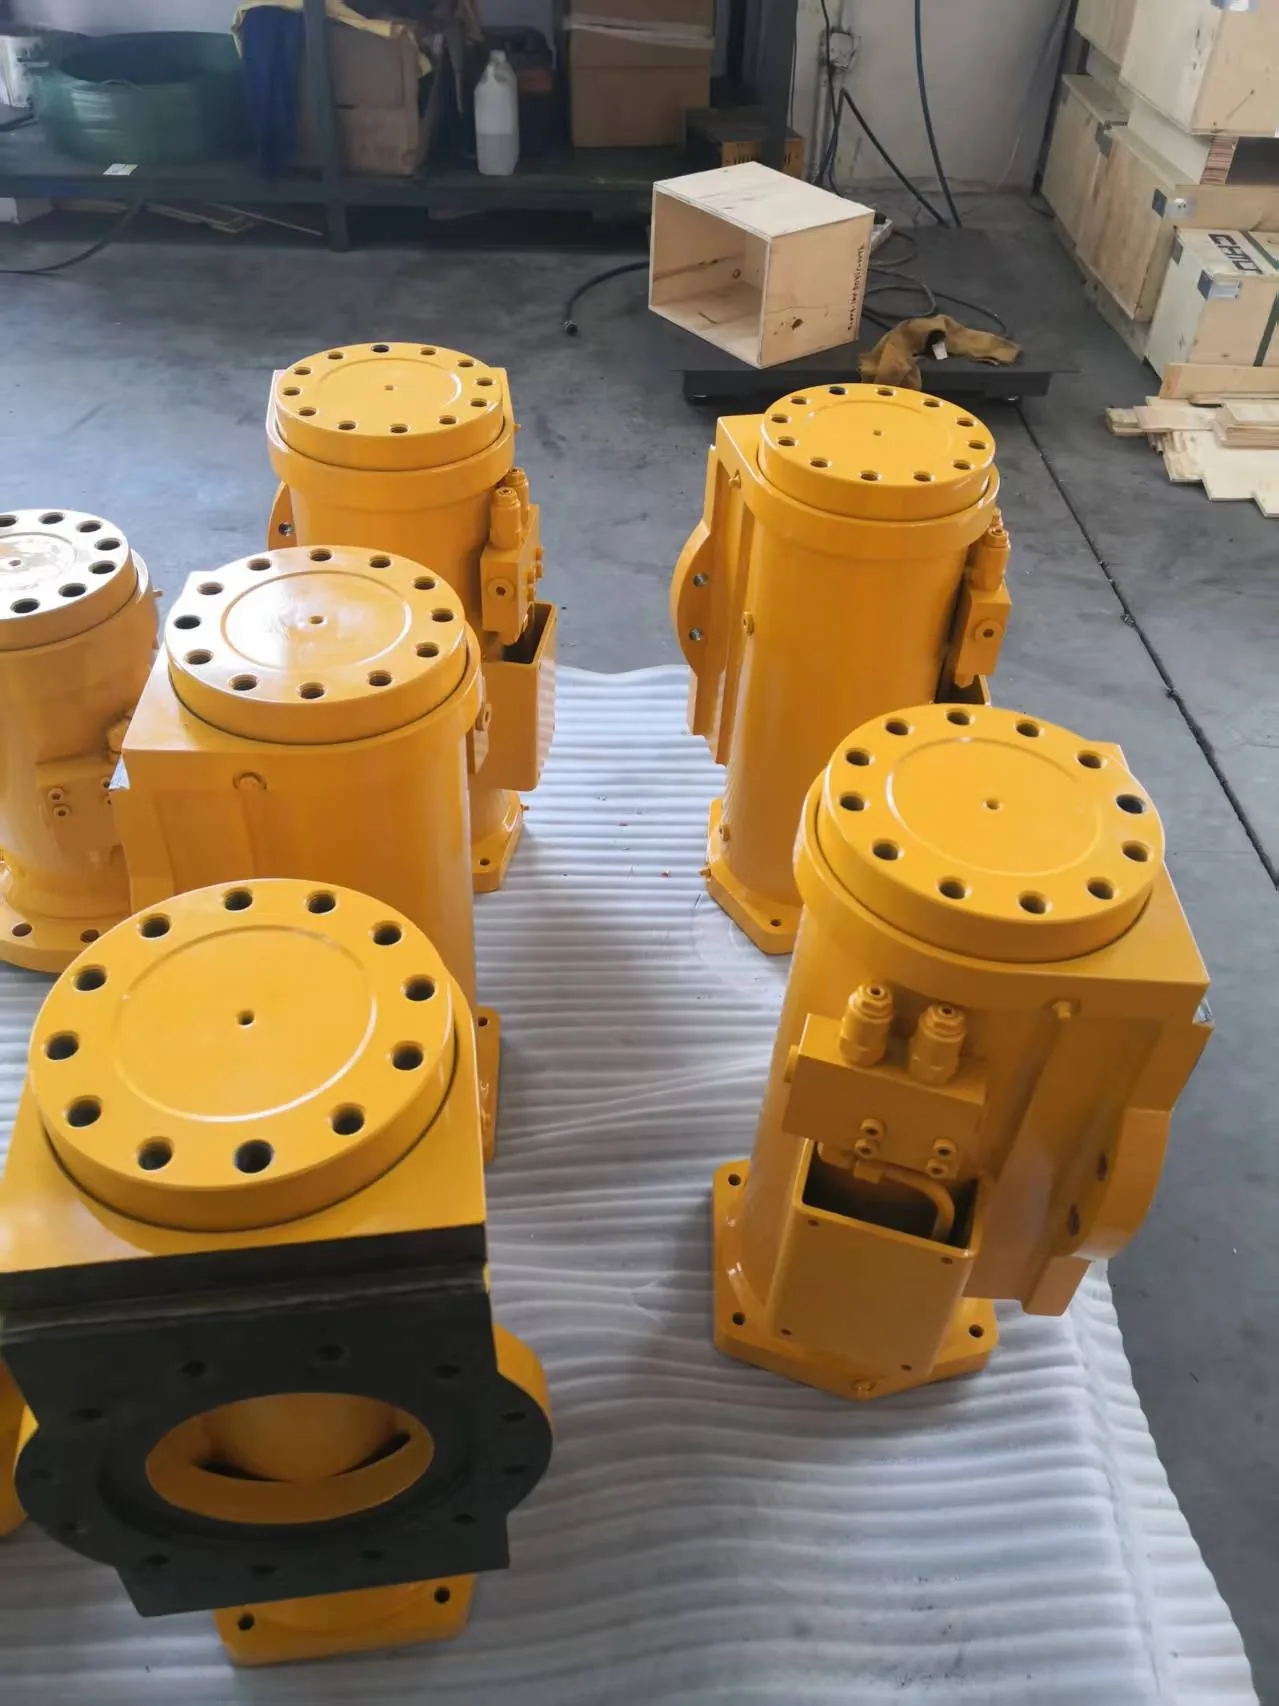
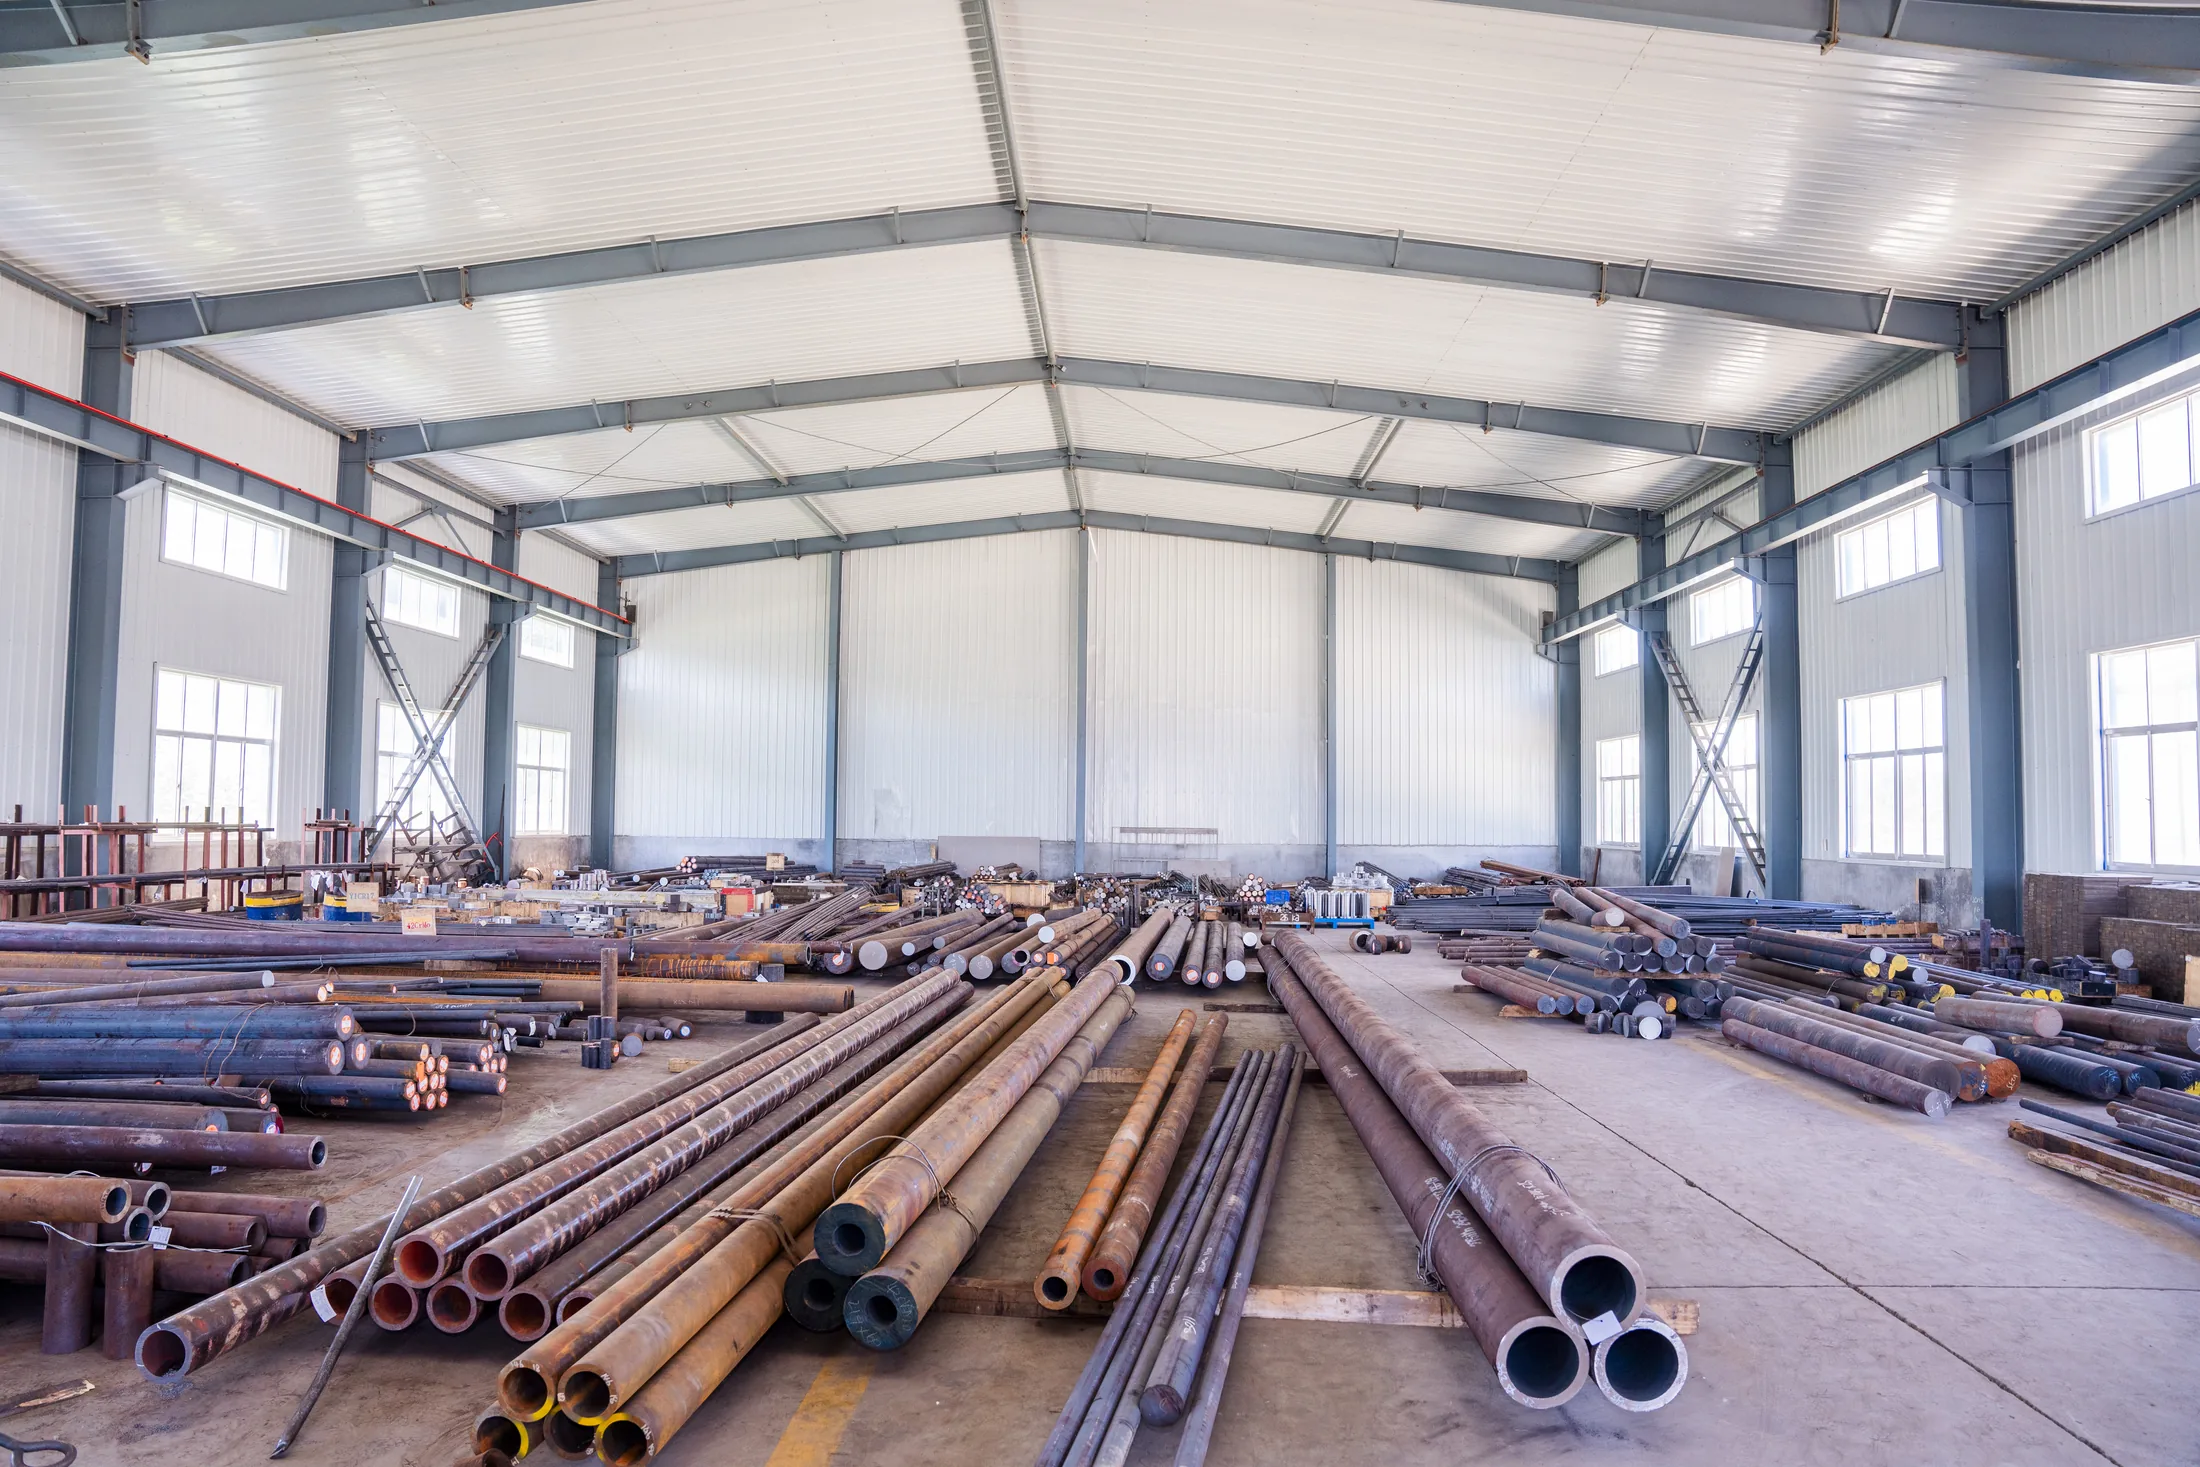
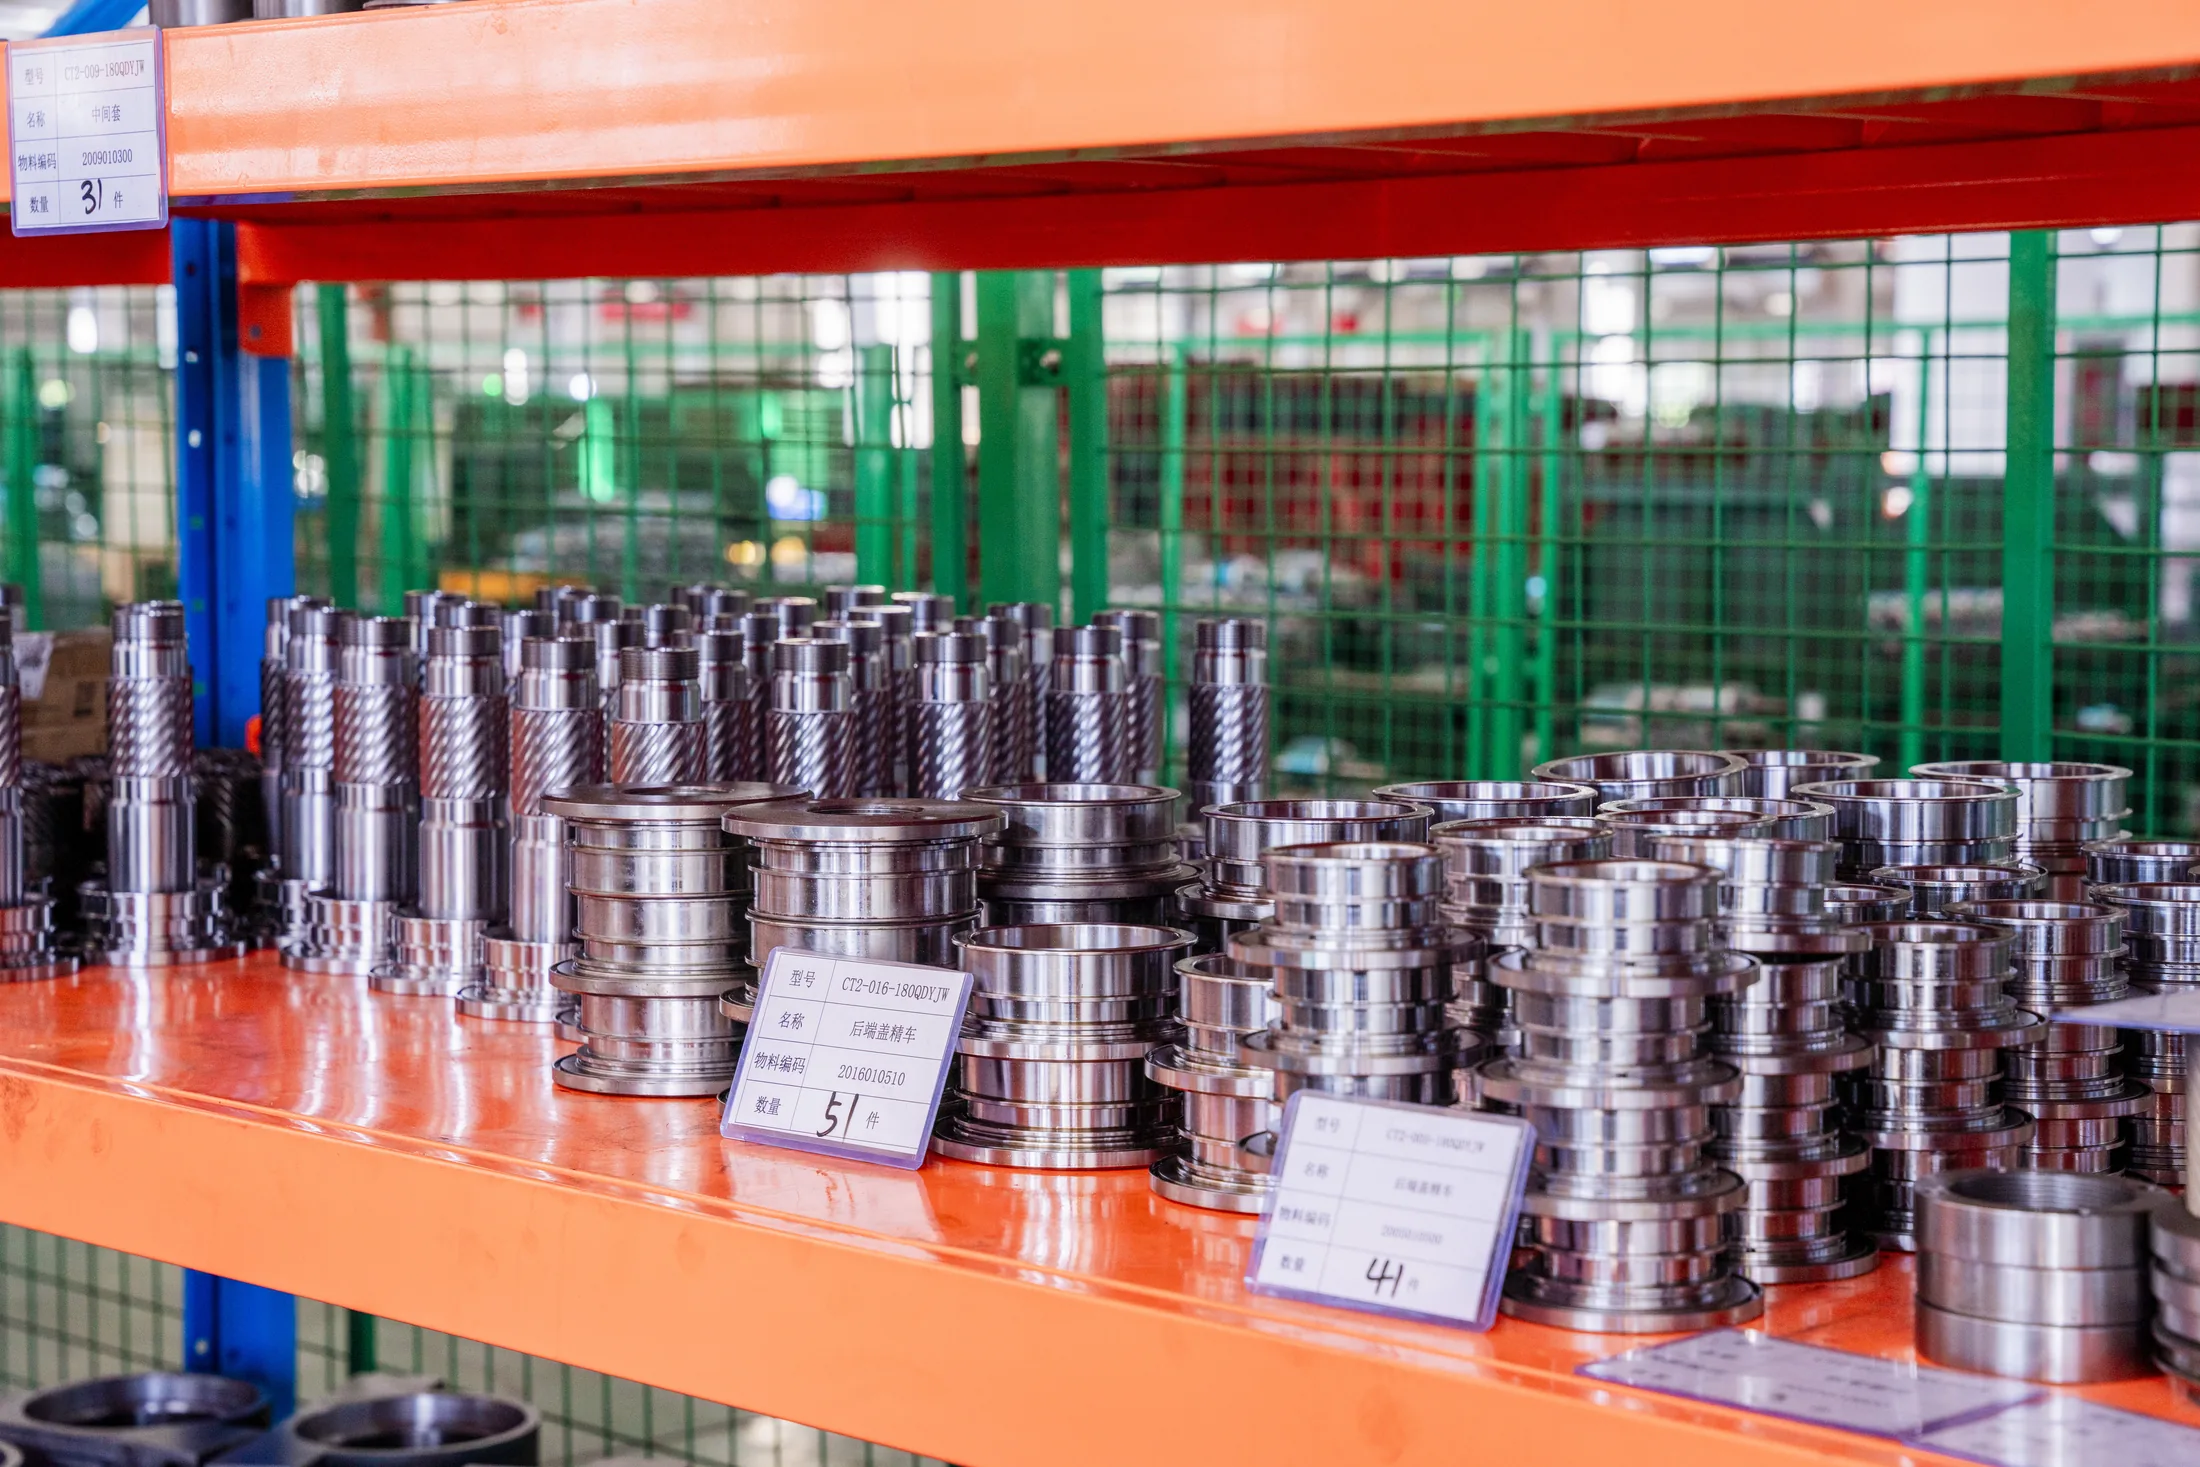
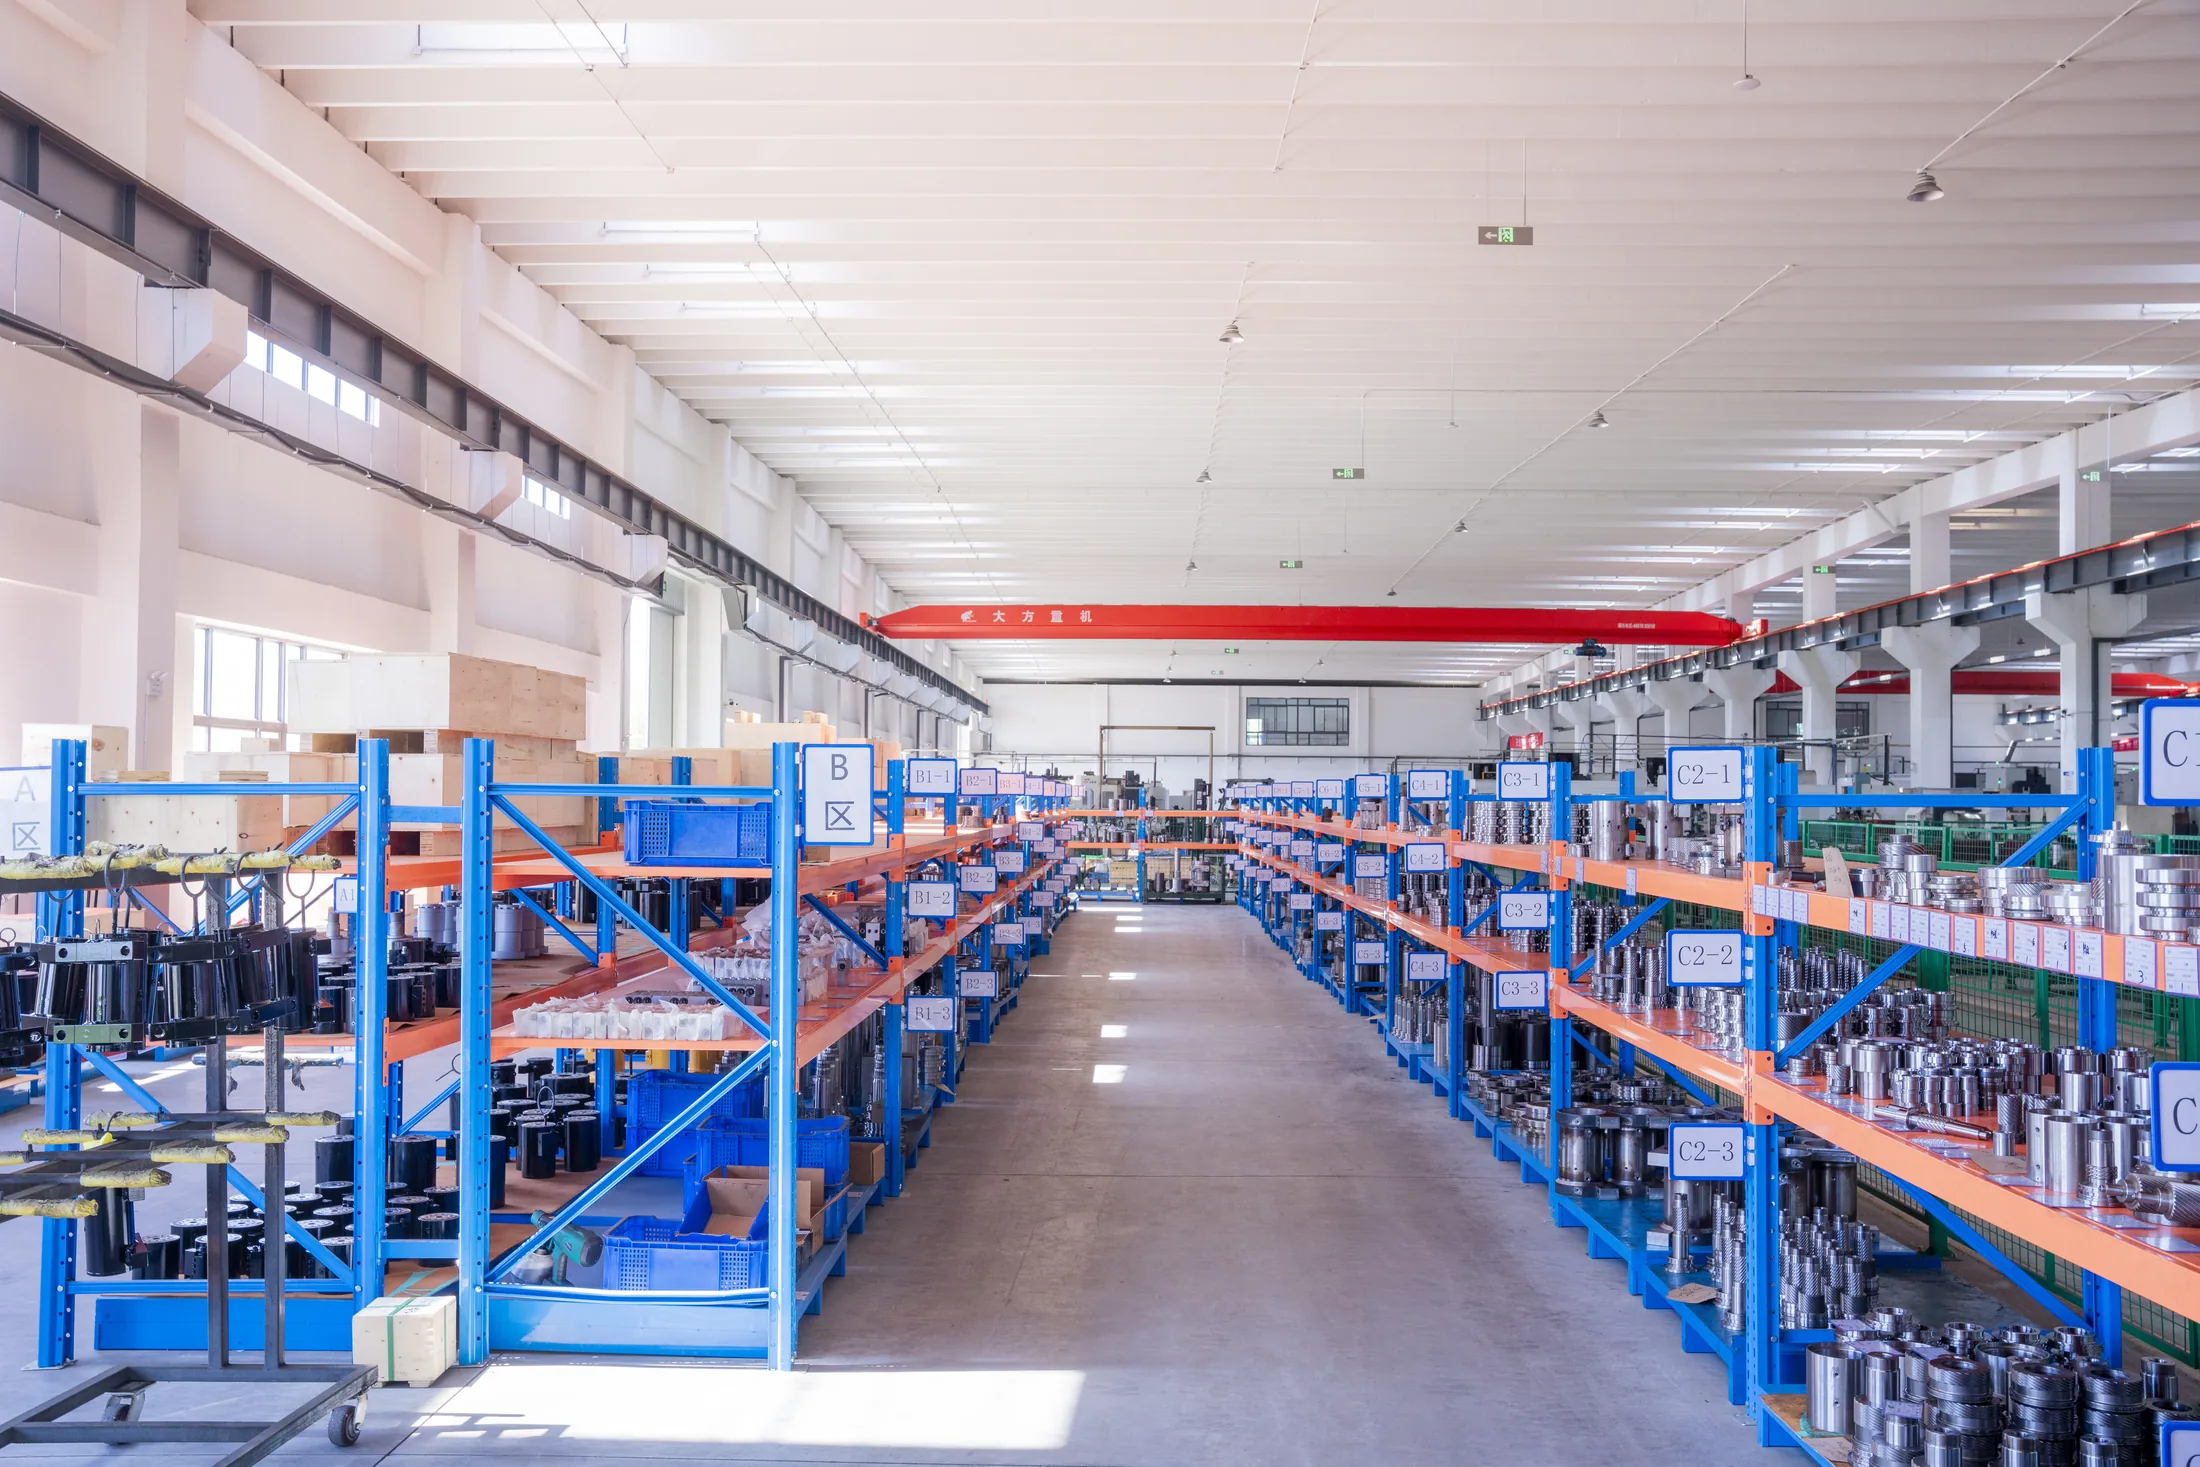
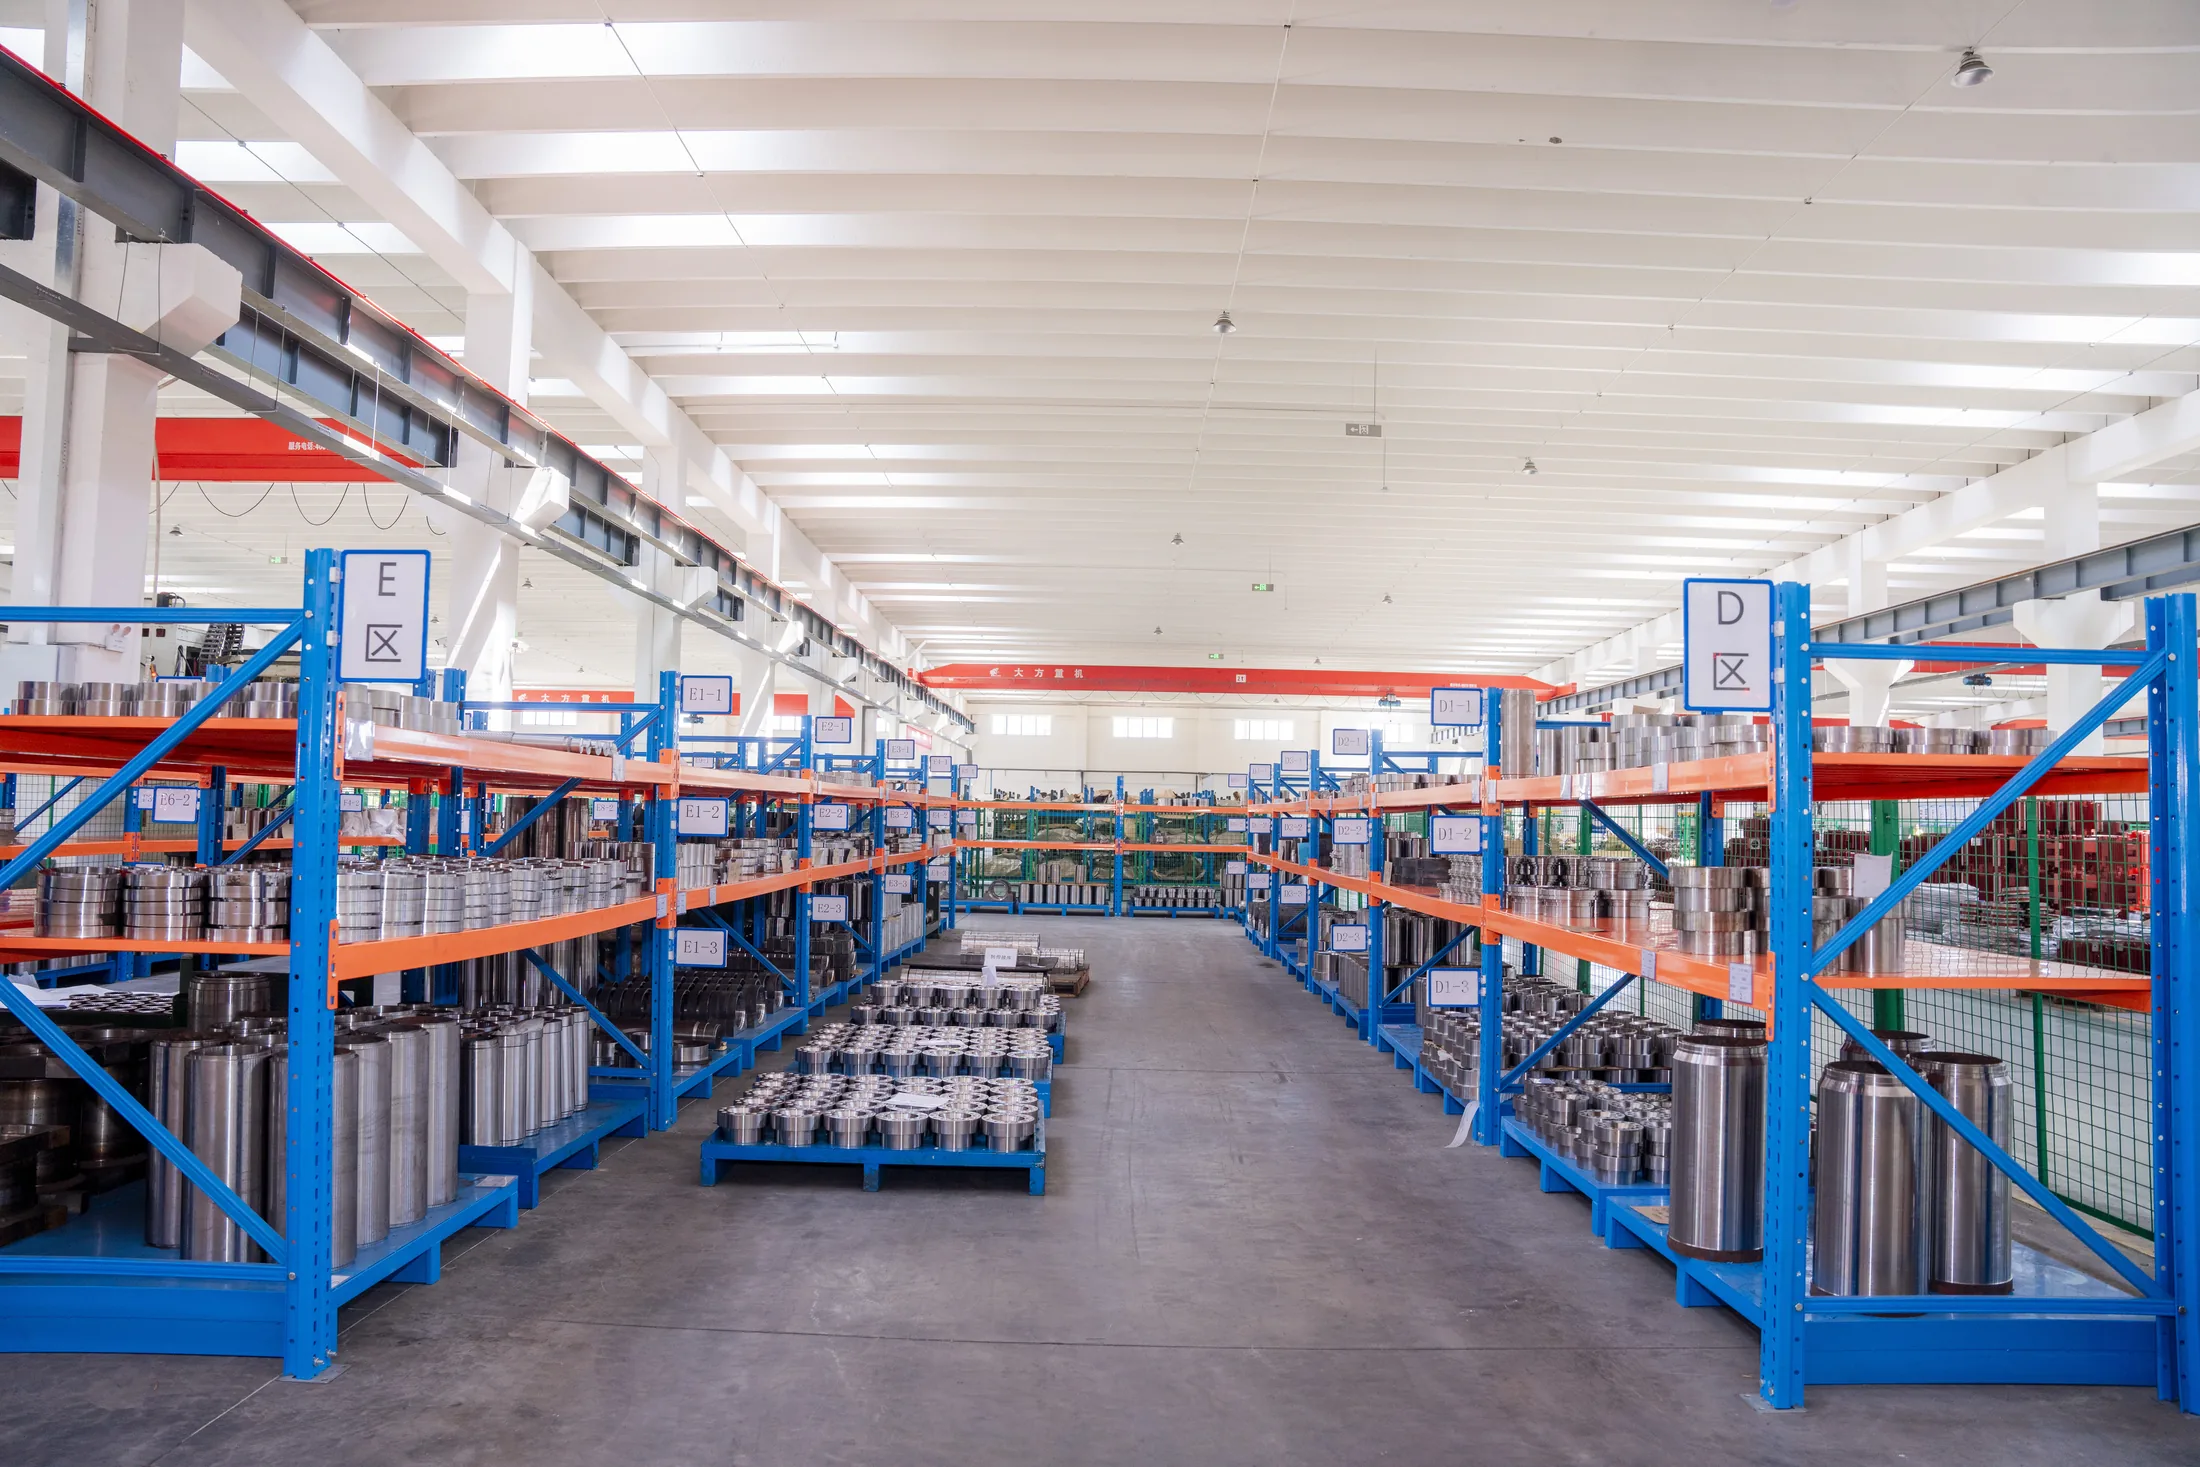
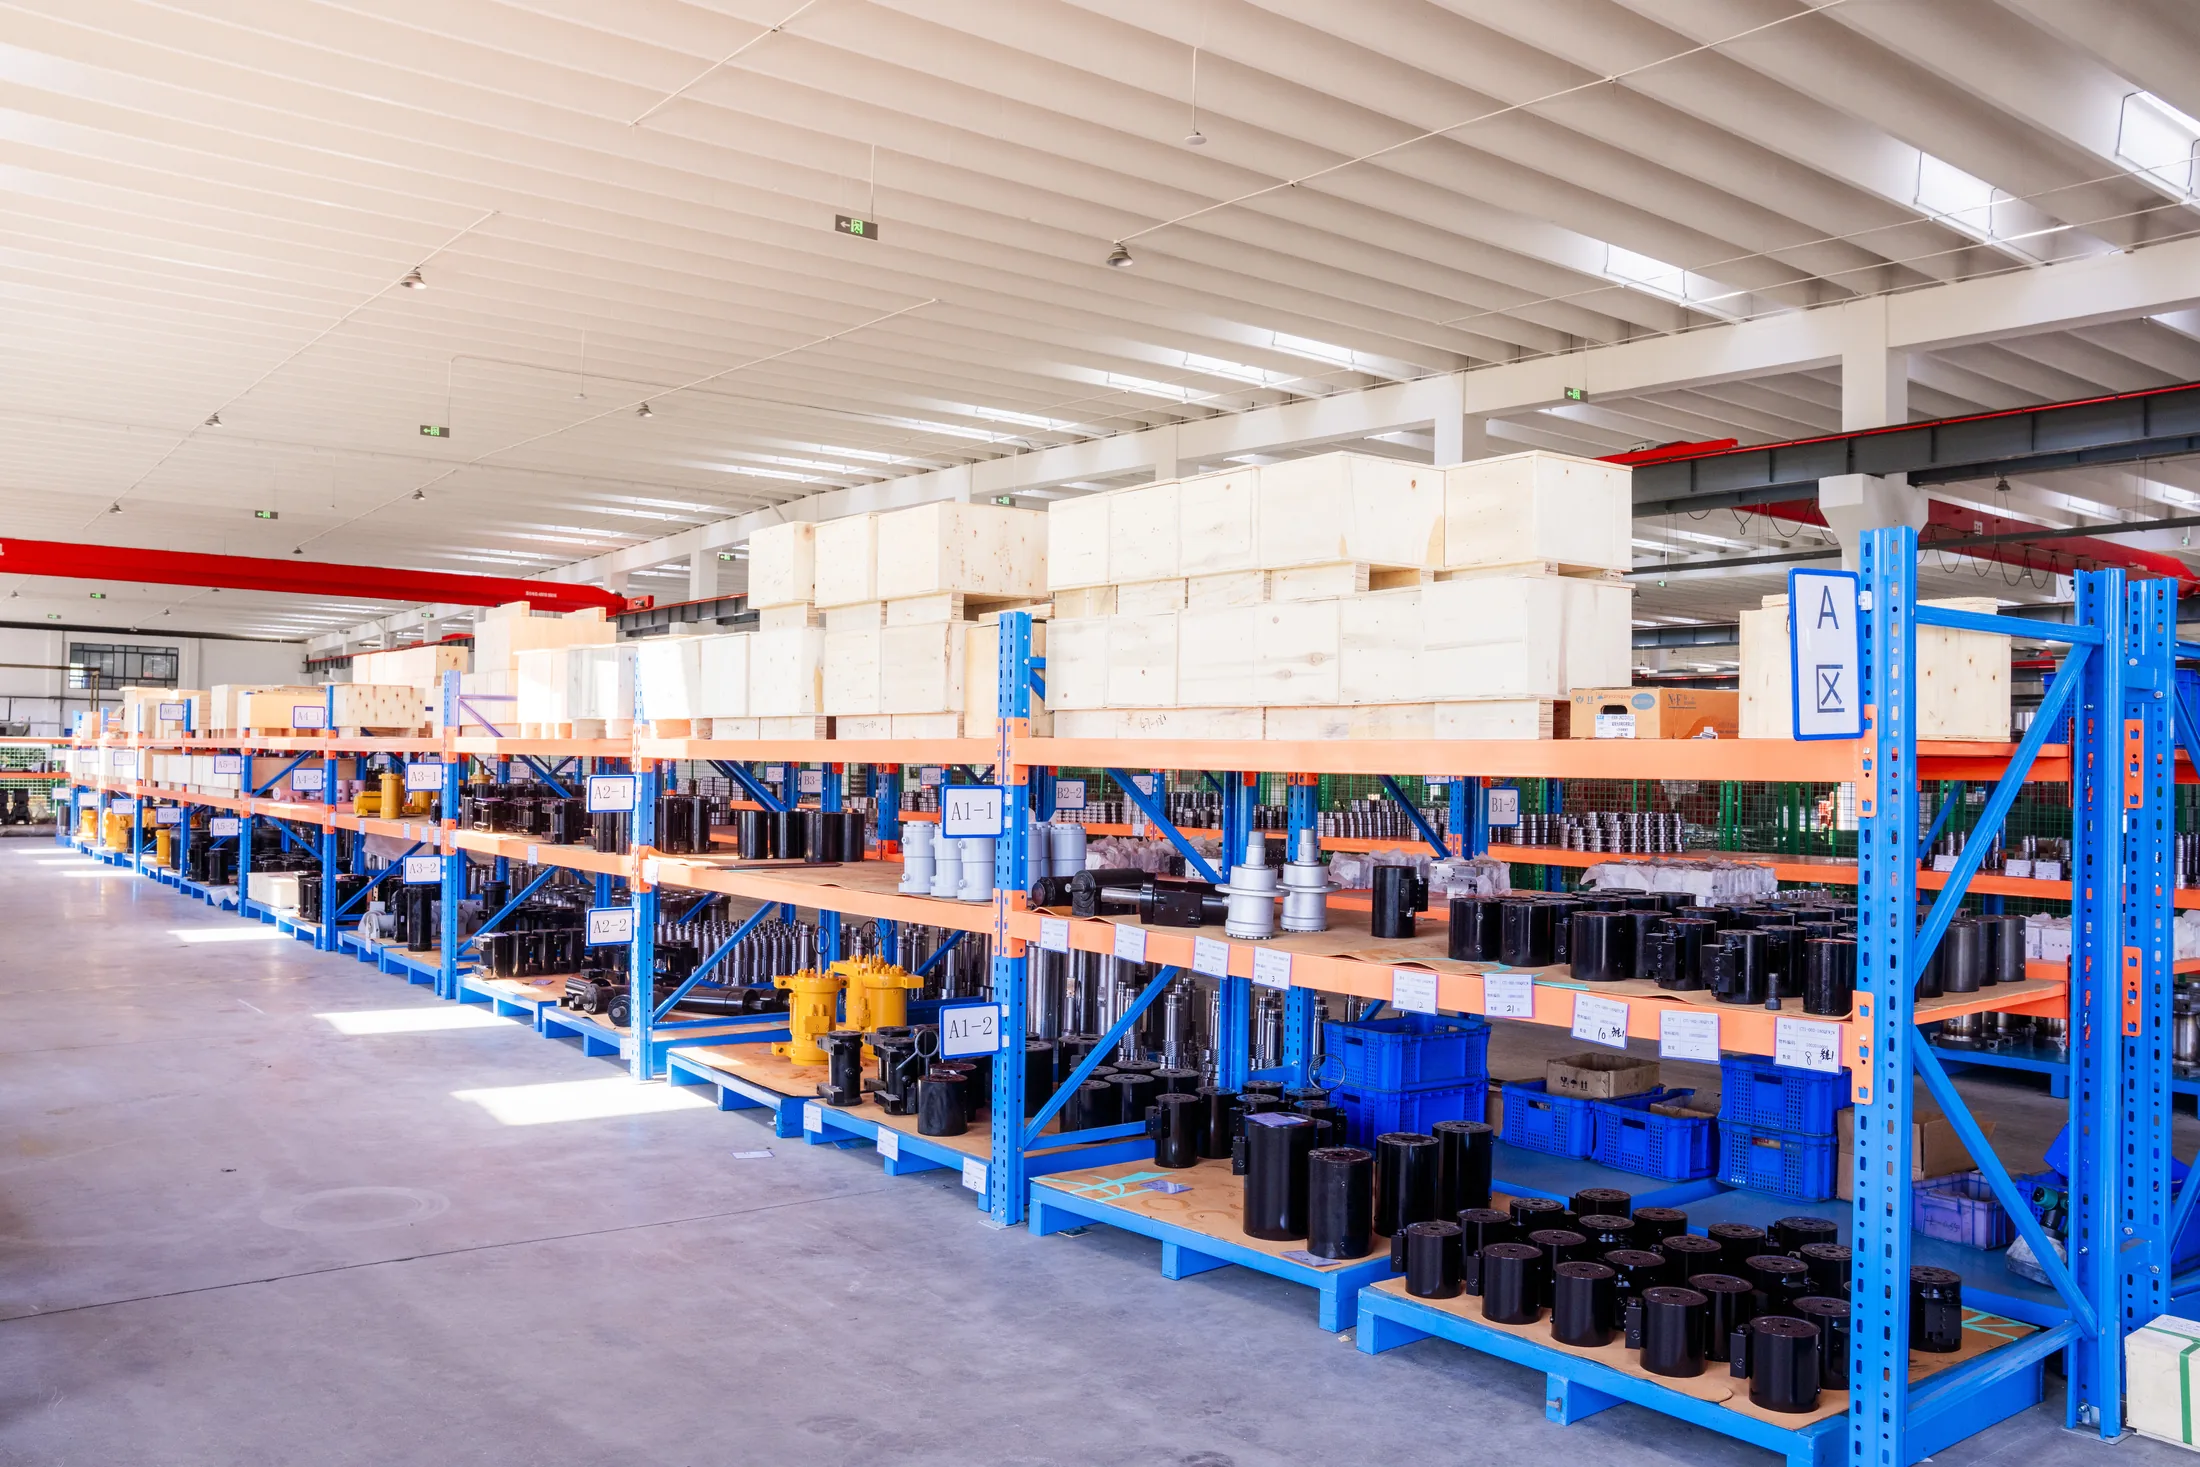
Zoned stock, ready for dispatch
Bin locations across parts, semi-finished and finished-goods stores — this is what "ex-stock dispatch" actually looks like. Replacement units for the L10 / L20 / L30 ladder are held as semi-finished and finished stock.
What we run, by process
| Process | Machine type | Makes on the floor |
|---|---|---|
| Helical spline whirling-milling | CNC thread whirling machine | ZRD80WA and up |
| Gear cutting / skiving | Gear hobbing machine / CNC gear skiving machine | YK8130 series |
| Vertical turning (big flanges) | CNC vertical turning lathe (VTL) | Doosan PUMA V8305, Neway VNL80S |
| Slant-bed turning | Slant-bed CNC lathe | Haitian line, Hision |
| Swiss-type turning (small shafts) | CNC Swiss-type lathe | Tornos SwissDT 26 |
| Milling — vertical | Vertical machining centre (VMC) | Doosan DNM 5705, Sino VMC1060, JM-1160 |
| Milling — horizontal | Horizontal machining centre (HMC) | Four-side HMC with pallet work |
| Cylindrical grinding | External cylindrical grinder | Finish grinding of shafts and pistons |
| Dimensional inspection | Coordinate measuring machine (CMM) / contour measuring instrument | Brown & Sharpe CMM (1210×1212×1200), Mitutoyo Contracer CV2000 |
Every machine carries a numbered equipment plate and maintenance log — third-party auditors can trace any serial-numbered unit back to the machine, the operator and the shift.
About the works
Is Baishili a manufacturer or a trader?
A manufacturer. Machining, gear grinding, assembly, painting and 100% pressure and function testing happen under one roof, on a single site in Weihai, China — no trading and no outsourcing of core processes.
Are the helical splines made in-house?
Yes. The multi-start helical spline is whirling-milled in one clamping, ring gears and pistons are cut on a CNC gear machine, and each spline set is finish-ground and kept together as a matched set from grinding to assembly.
How is each actuator tested?
Every unit is cycled and logged on the pressure and function test rig before dispatch. First articles, batch samples and custom prototypes are also measured on the CMM and contour machine, and the reports are supplied with every custom order.
Can a unit be traced back to how it was made?
Yes. Every unit is serialised, and every machine carries a numbered equipment plate and maintenance log — auditors can trace any serial-numbered unit back to the machine, the operator and the shift.
Can we visit or inspect the factory?
Yes. Visitors and third-party inspections are welcome at the Weihai works.
Where is stock held for India?
Replacement units for the L10 / L20 / L30 ladder are held as semi-finished and finished stock at the works, and as ready stock in Bengaluru for pan-India dispatch in 3–7 days.